
Tuowei Precision is a die casting supplier for housings, covers, brackets and enclosures needed in repeat volumes. We build the tool, cast the parts in non-ferrous alloys, then machine critical bores and faces so each die-cast part arrives ready to assemble, with casting and machining handled by one team.
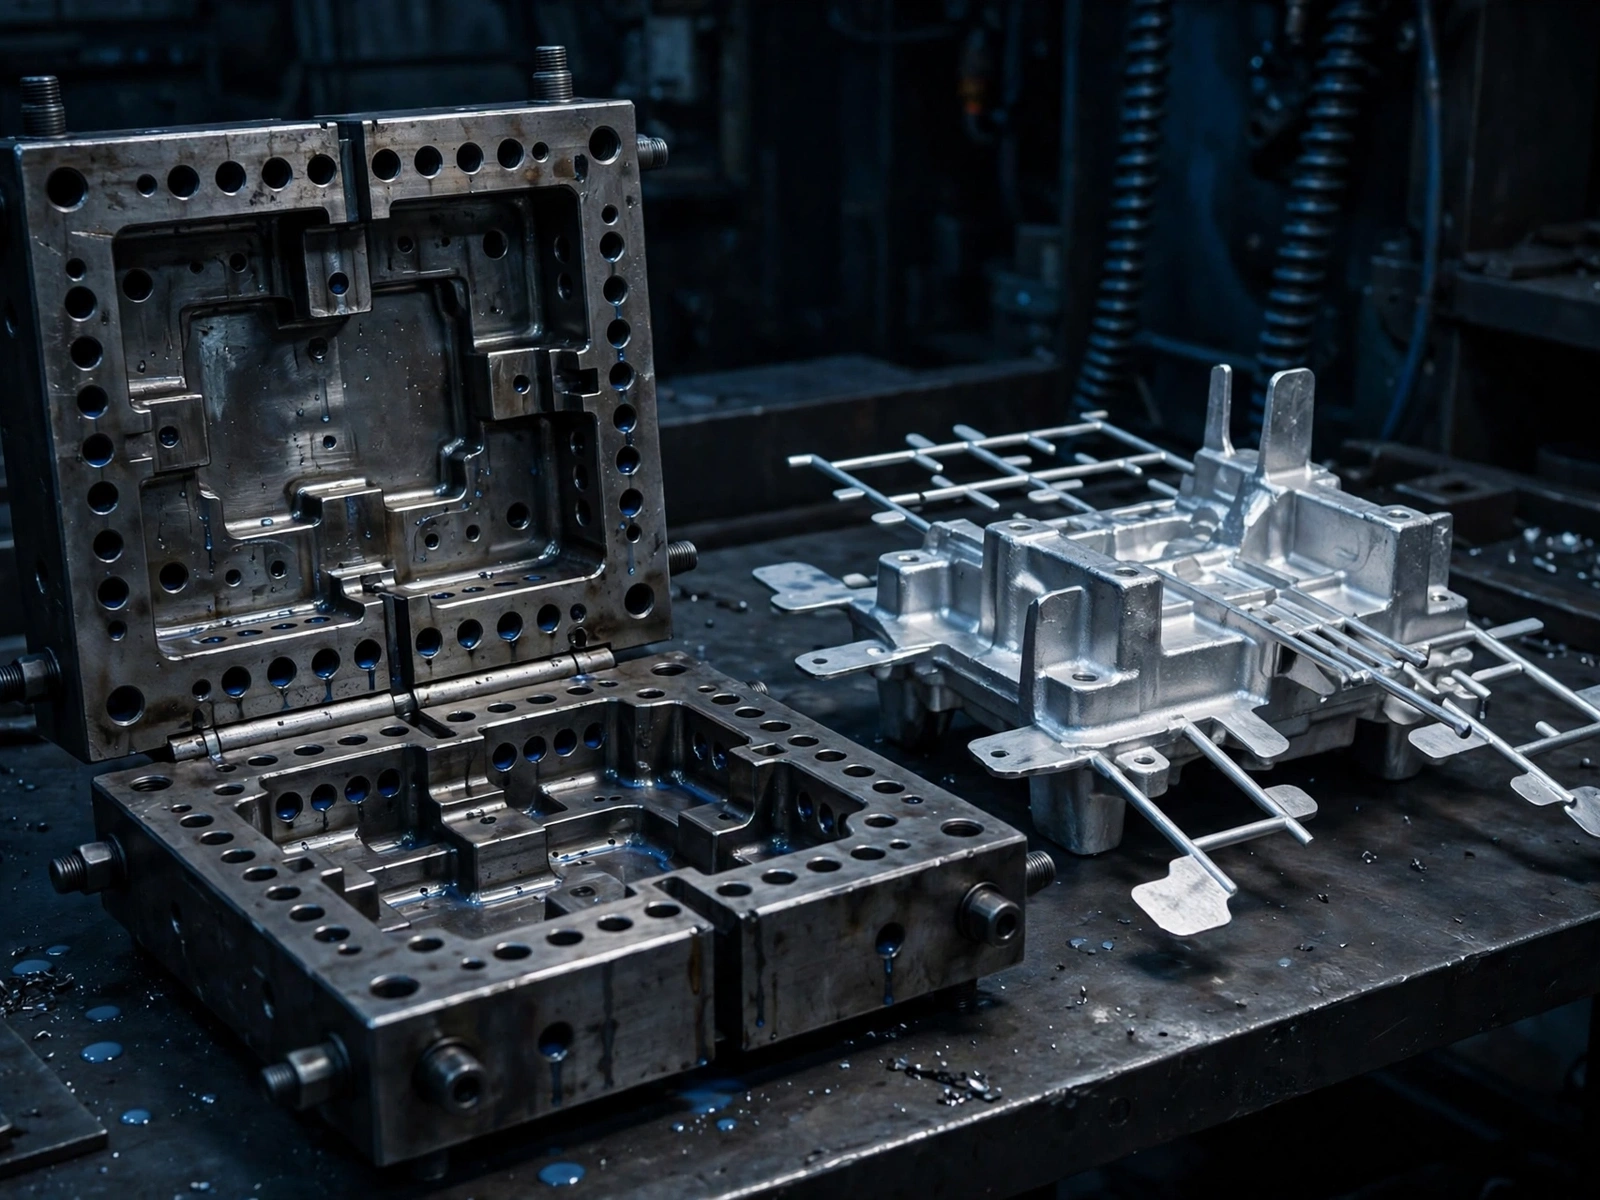
Die casting forces molten metal into a hardened steel die, so every shot repeats the same geometry. For parts needed in hundreds or thousands, that repeatability lowers cost well below machining from solid. Thin walls, ribs, bosses and mounting features come out of the die in one piece, which cuts assembly steps and weight. This ability to produce complex shapes at volume makes high-pressure die casting a cornerstone for cabin hardware and electronics boxes, and die casting enables thinner, lighter designs than sheet metal assemblies.
The trade-off is porosity. Trapped gas and shrinkage during solidification can leave small voids inside a casting, so die casting suits housings, covers and brackets far better than pressure-tight or fatigue-critical structure. We review where your part carries load, place gates and overflows to push voids away from critical areas, and tell you when machining from plate is the better choice.
| Alloy | Typical use | Notes |
|---|---|---|
| Aluminum A380 / ADC12 | Avionics housings, covers, brackets | Good strength-to-weight and fluidity; most common choice |
| Magnesium alloys | Weight-critical enclosures and cases | Lightest structural metal; needs a protective finish |
| Zinc Zamak 3 / Zamak 5 | Small detailed parts, connectors, knobs | Excellent detail and surface; heavier than aluminum |
Aluminum is the default for aerospace casting parts because it balances weight, tensile strength and cost. Magnesium saves more weight but needs coating against heat and corrosion. Zamak suits small, detailed parts where weight matters less. If you are unsure, send your load and environment requirements and we will shortlist the alloy.
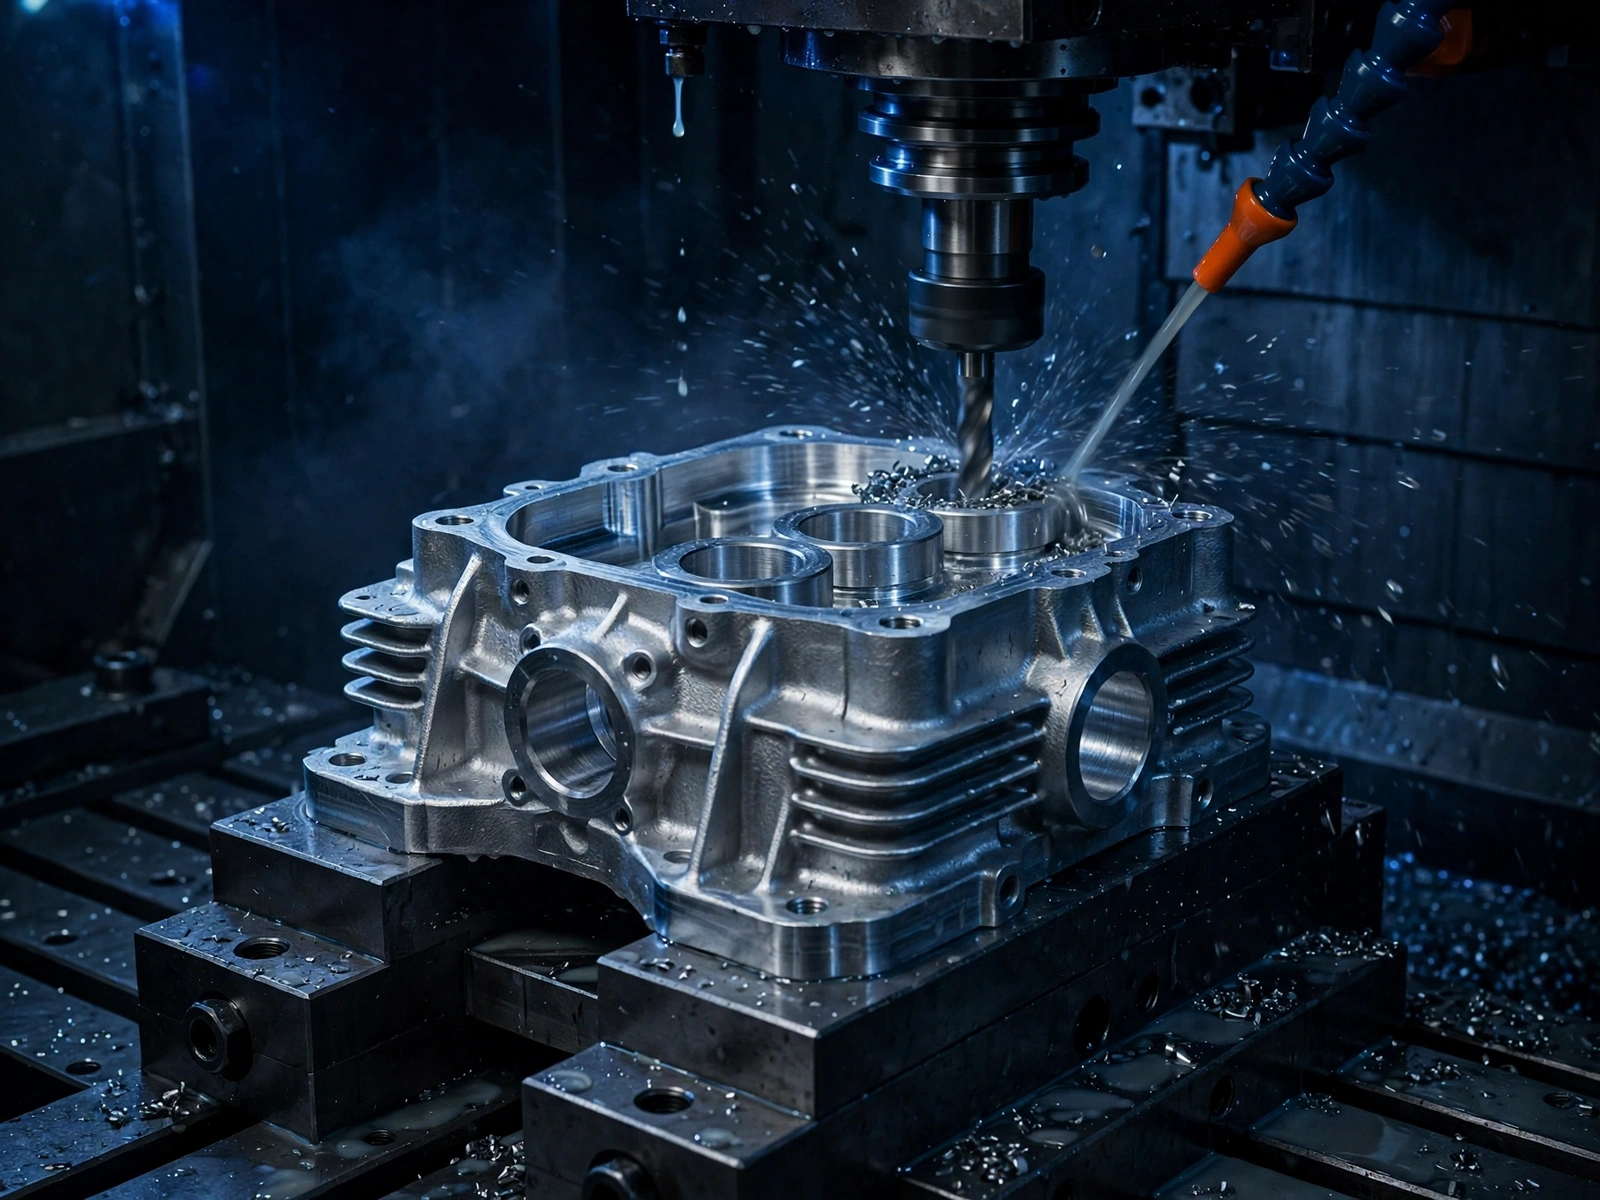
As-cast dimensions are repeatable, but bearing bores, sealing faces and threaded holes usually need CNC machining to reach the tolerances flight hardware demands. We design each housing with machining stock on those features and fixture it on cast datums, so machined features line up with the rest of the part. Anodizing, chromate conversion coating, powder coating and plating protect the surface after machining.
Engineers comparing casting methods usually weigh three routes:
| Method | Best for | Trade-off |
|---|---|---|
| Die casting | Housings, covers, brackets in volume | Tooling cost; internal voids limit critical use |
| Lost-wax casting | Turbine blades, superalloy and complex parts | Slower and costlier per part |
| Machining from solid | Prototypes and fatigue-critical parts | Higher cost per part at volume |
Lost-wax foundries handle nickel superalloys and steels for engine parts, which die casting cannot. We do not offer that process and will point you to a specialist foundry. Where volumes are low or the part is critical, our aerospace machined parts service is often the better route.
When you need 20 to 200 plastic parts before committing to a mold, vacuum casting pours polyurethane resin into a silicone mold under vacuum to remove air bubbles. Parts mimic ABS, PP or elastomers, hold about ±0.15 mm, and simple parts can ship in under 5 days. It is a common bridge for interior trim, covers and test housings. See our vacuum casting service for materials.
Our quality system follows standards like AS9100 and ISO 9001 and covers the route from alloy to finished part. We provide material certificates, first article inspection, dimensional reports on machined features and lot traceability on request. Sectioning or X-ray checks by an approved lab can be arranged when your drawing calls for proof of structural integrity. These quality standards are how we deliver precision and reliability on critical applications.