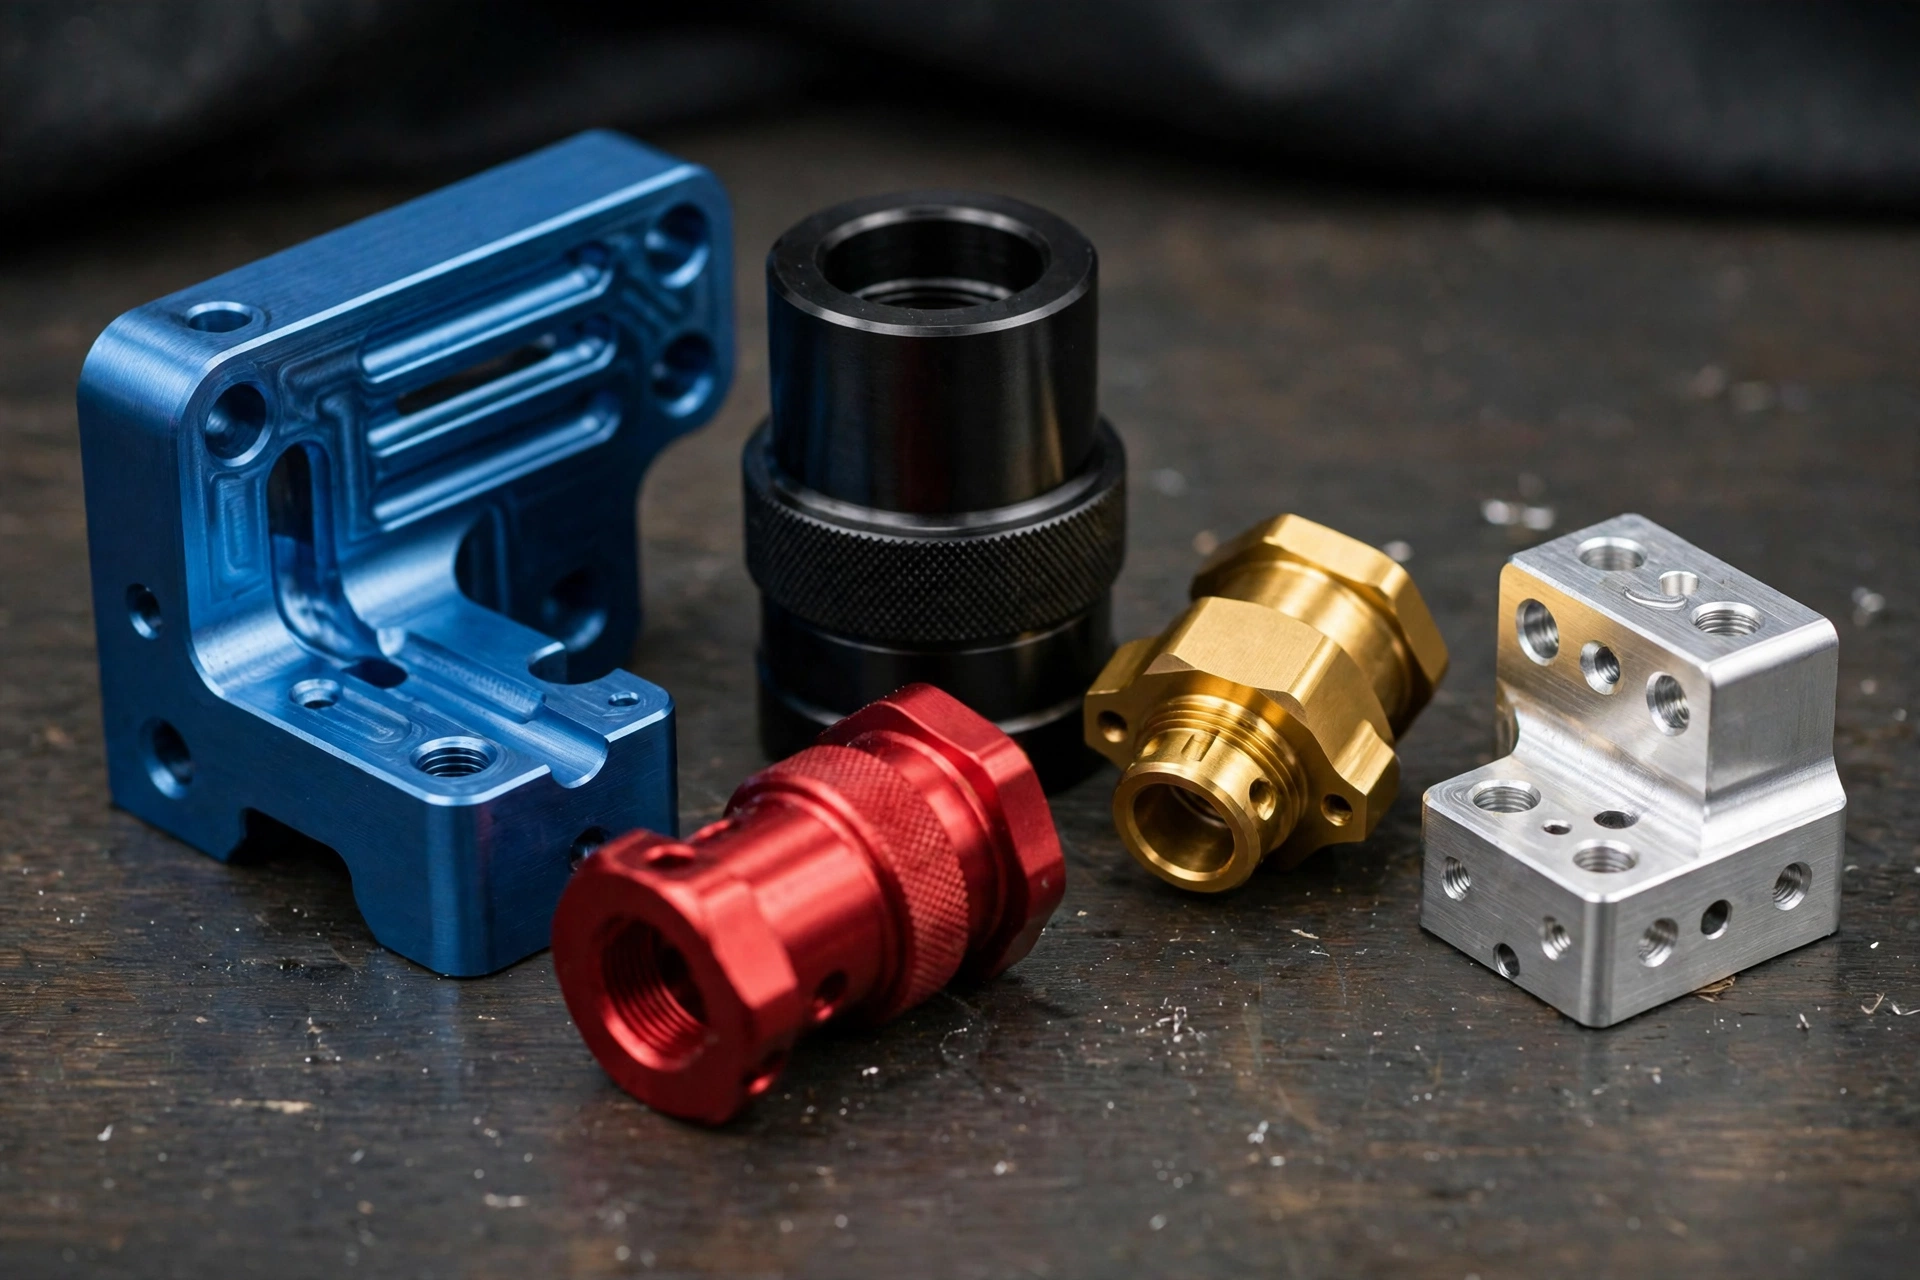
Anodizing is an electrochemical process that grows a hard, protective oxide layer on the surface of a metal, most often aluminum. The part is placed in an acid bath and connected to the positive side of a power supply, and the current converts the outer surface into aluminum oxide. The result is a finish that resists corrosion and wear, accepts color dyes and will not peel, because it is part of the metal itself. Outside North America the process is spelled anodising, so British and European specs refer to sulphuric acid anodising and chromic acid anodising of aluminium.
Short answer: Anodizing turns the surface of aluminum into a controlled anodic coating. Electric current passes through an acid electrolyte with the part as the anode, so oxygen bonds with the surface and builds a fine, protective film. That film can be dyed and is then sealed. It improves corrosion resistance, wear resistance and appearance, and it adds a small, predictable amount of thickness.
So what is anodizing compared with paint or plating, and what should you know before you anodize a part or put the finish on a drawing? This guide explains how the process works, what it changes about aluminum parts, which metals and alloys anodize well, and the mistakes buyers make when specifying it.
Aluminum already protects itself. Exposed to air, it forms a naturally occurring film only a few nanometers thick within seconds. This natural oxide layer slows oxidation but can scratch easily and offers almost no protection against abrasion.
When people ask what is anodizing aluminum, the answer is that it takes this natural reaction and controls it. Instead of a few nanometers, the process builds a consistent oxide layer measured in microns, with a structure engineers can predict and specify.
Three points make the process different from other coatings:
The best way to explain how does anodizing work is to follow a part through one process cycle. A typical line has six stages.
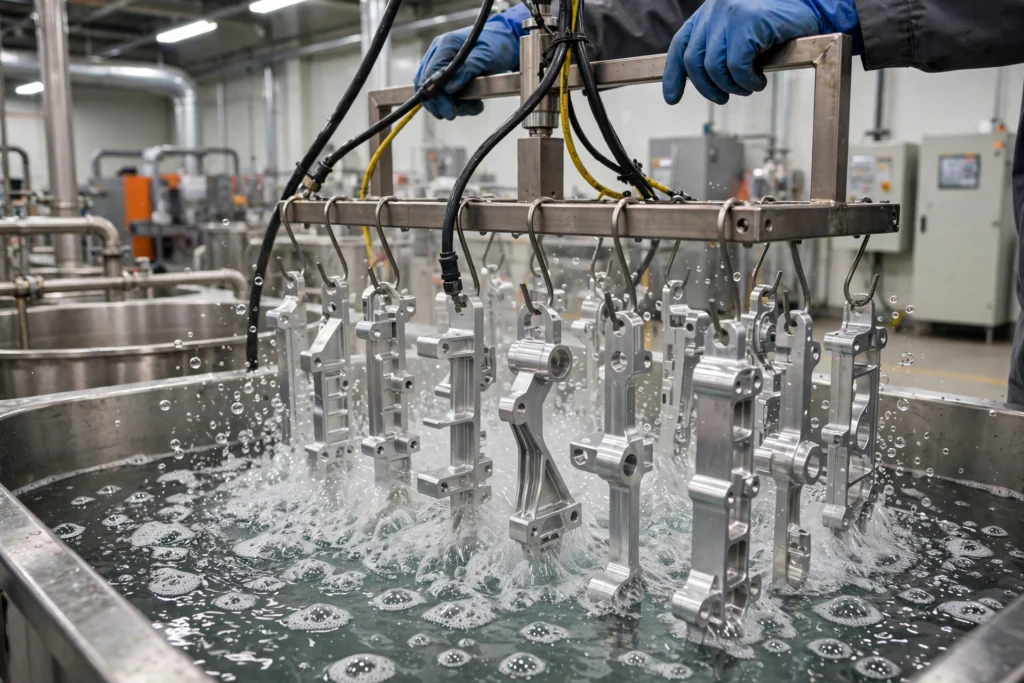
The part is degreased to remove machining oil and fingerprints. Any residue left here shows up later as stains or uneven color. Many shops also etch the part in an alkaline bath to strip the natural film and give a uniform matte base. Skipping this step is the most common reason parts anodize with blotches.
Etching leaves a dark residue called smut, made of alloying elements that do not dissolve. An acid dip removes it. Some cosmetic parts also go through chemical brightening for higher reflectivity.
The part is racked on a conductive fixture and lowered into the electrolyte solution, most often dilute sulfuric acid. The part becomes the anode, or positive electrode, and the tank holds the cathode, the negative electrode. When it flows, the current releases hydrogen at the cathode, while oxygen at the part surface combines with aluminum to build the coating. The voltage is ramped up gradually so the layer grows evenly. A Type II line often runs at roughly 12 to 20 volts, while hard coat needs a higher voltage as the film thickens. Acidity, solution temperature and current density are all controlled, because each one changes how hard and how thick the coating becomes.
While the pores are still open, the part can be dipped in an organic dye, or colored electrolytically with tin or nickel salts for deep bronze and black shades that resist fading better outdoors.
To seal the pores, shops use hot deionized water, steam or a nickel acetate solution. A good seal hydrates the film so the pore openings swell shut. This locks in the dye and greatly improves protection against corrosion. Unsealed parts stain easily and corrode faster, so always state whether you want the shop to seal the finish or leave it open for paint or bonding.
The parts are rinsed, dried and checked for coating thickness, color match and coverage. Rack contact points stay bare, so they should be placed on non-critical surfaces.
The time in the tank and the current density decide how thick the layer grows. A common rule of thumb is the 720 rule: coating thickness in mils equals current density (amps per square foot) multiplied by time in minutes, divided by 720. At 12 amps per square foot for 60 minutes, that gives about 1 mil (0.001 in) of coating. Thicker films tend to look darker and feel harder, which is why parts that anodize to hard coat in 6061 usually come out gray rather than clear.
What does anodizing do to aluminum in practical terms? It changes five things about the part.
| Property | What changes |
|---|---|
| Corrosion resistance | Much better, especially once sealed |
| Wear resistance | Better with Type II, much better with Type III hard anodizing |
| Appearance | Clear, satin or dyed in many colors |
| Electrical conductivity | Surface becomes insulating |
| Dimensions | Each coated surface grows by about half the coating thickness |
The two changes engineers forget are conductivity and dimensions.
Because the anodic layer is an electrical insulator, anodized aluminum cannot be grounded through its surface. Heat sinks are often anodized black anyway, since the dark finish helps them radiate heat. If a bracket, enclosure or heat sink needs a ground path, mark those areas for masking on the drawing.
The dimensional change is predictable but real. Roughly half the coating forms below the original surface and half builds up above it. A 0.002 in hard coat grows each surface by about 0.001 in, so a shaft gets bigger and a bore gets smaller by about 0.002 in on the diameter. Threads and tight fits need allowance before machining, or masking.
So what does anodizing do overall? It trades a small amount of dimensional control for a surface that is harder, longer lasting and better looking than bare aluminum.
In the US, aluminum anodizing is usually specified to MIL-PRF-8625, still written as MIL-A-8625 on many drawings. It defines three main types: Type I chromic acid anodizing, Type II sulfuric acid anodizing and Type III hard anodizing.
| Type | Electrolyte | Typical thickness | Main use |
|---|---|---|---|
| Type I | Chromic acid | Very thin, about 0.00002 to 0.0001 in | Aerospace parts where fatigue strength matters |
| Type II | Sulfuric acid | About 0.0002 to 0.001 in | Corrosion protection and color |
| Type III | Cold bath at high current densities | Nominal 0.002 in | Wear and abrasion resistance |
This chromic process was first developed for British defence work in the 1920s. It gives a very thin film that has little effect on fatigue strength, which kept it popular for aerospace structures. It is less common today because of environmental rules around hexavalent chromium.
Type II is the everyday choice for housings, brackets, enclosures and consumer parts. It balances corrosion protection, color and cost, and adds only a small amount of thickness.
Type III, also called hardcoat, is the process used for parts that slide, rub or face abrasion. Its bath needs strong refrigeration to stay close to freezing while running at high current.
Some specialty lines use organic acids such as oxalic acid, or a mix of acids, for particular colors or hardness. Aerospace buyers may also see AMS 2469 for hard coat, AMS 2471 and AMS 2472 for clear and dyed films, and AMS 2482 for hard coat with PTFE. ASTM B580 covers anodic finishes for general engineering use, and ASTM D3933 covers phosphoric acid anodizing before adhesive bonding.
Choosing between the two common types is worth its own guide. Our comparison of Type II vs Type III anodizing covers thickness, color, sealing and cost in detail.
Aluminum is by far the most widely used metal for anodizing, but several others can also be anodized, including magnesium, zinc, niobium and tantalum. Steel cannot be anodized in the usual sense, because iron oxide (rust) is loose and flaky rather than protective. Steel parts need plating, bluing or paint instead.
Alloy choice matters a lot for aluminum. Alloying elements do not convert the same way as pure aluminum, so they change the color and quality of the coating:
If appearance matters, choose the alloy with the finish in mind before you anodize anything. Our guide to the best aluminum alloy for anodizing compares the common grades, and our 6061 aluminum CNC machining guide covers the most popular choice for anodized parts.
What is anodizing titanium, and how is it different? Shops anodize it with the same electrochemical principle, but the result looks and behaves differently from aluminum.
The film on this metal is very thin and clear. The color you see comes from light interference, the same effect that makes a soap bubble or oil film look colored. The final voltage sets the film thickness, and the thickness sets the color. Lower voltages give bronze and blue, while higher voltages give gold, purple and green. No dye is involved, so the colors do not fade.
There are two common reasons for this finish:
The main limitation is durability. The colored film is extremely thin, so handling and abrasion can wear through it quickly.
Anodizing is the default protective finish for aluminum for good reason, but it is not perfect.
| Benefits | Limitations |
|---|---|
| Strong protection against corrosion when sealed | Adds thickness that affects tight fits |
| Hard, wear resistant surface | Surface becomes electrically insulating |
| Will not peel or flake | Thick coatings can reduce fatigue strength |
| Wide choice of dyed colors | Color can vary between batches and alloys |
| Thin, consistent layer | Some dyes fade under long UV exposure |
| Good base for paint and adhesives | Damaged areas cannot be touched up easily |
Anodizing can also be used as a pre-treatment before painting or bonding, since the porous surface gives coatings and adhesives a strong grip.
Our view: for most machined aluminum parts, sealed Type II anodizing gives the best balance of protection, cost and appearance. Move to Type III only when a surface truly needs wear resistance, because the thicker layer costs more and needs larger dimensional allowances.
Most problems with the anodizing process start on the drawing, not in the tank. These are the issues that cause rework most often:
At Tuowei Precision, we anodize parts as part of the machining job, so the same team controls both the dimensions and the finish. Our aluminum anodizing services cover Type II for corrosion protection and color, and Type III hard anodizing for wear. Our standard as-machined surface before coating is about 125 µin Ra (3.2 µm), and bead blasting can be added for an even cosmetic finish.
If you are still choosing a finish, our guide to surface finishes for CNC machined aluminum compares anodizing with chem film, powder coat, plating and more. You can also browse all of our surface finish services in one place.
Anodizing is a way of making the surface of aluminum tougher and more resistant to corrosion. The part sits in an acid bath while electricity passes through it, which grows a hard protective layer that becomes part of the aluminum itself.
Anodizing does not peel, but it can wear down over time through abrasion, harsh alkaline cleaners or long UV exposure that fades some dyes. Type III hard anodizing resists wear far better than Type II on parts that rub or slide.
You cannot anodize steel or most iron-based metals, because their rust is loose rather than a protective film. Copper and brass are also unsuitable. Aluminum and titanium are the materials most commonly anodized for engineered parts.
An anodized surface is electrically insulating, grows slightly in size and can show color differences between batches or alloys. Thick coatings can also reduce fatigue strength. Damaged areas are hard to repair without stripping and recoating the whole part.
A well-sealed anodized finish can last for decades indoors and many years outdoors. Its lifespan depends on coating type and thickness, sealing quality, dye choice, and exposure to abrasion, UV light and aggressive cleaning chemicals.