
Tuowei Precision supplies custom aerospace aluminum extrusions and turns extruded shapes into finished parts. We produce 6061 and 6063 sections on press lines from 600 to 3,800 tons, then cut, machine and anodize them, so you receive rails, frames and brackets ready for assembly rather than stock lengths.
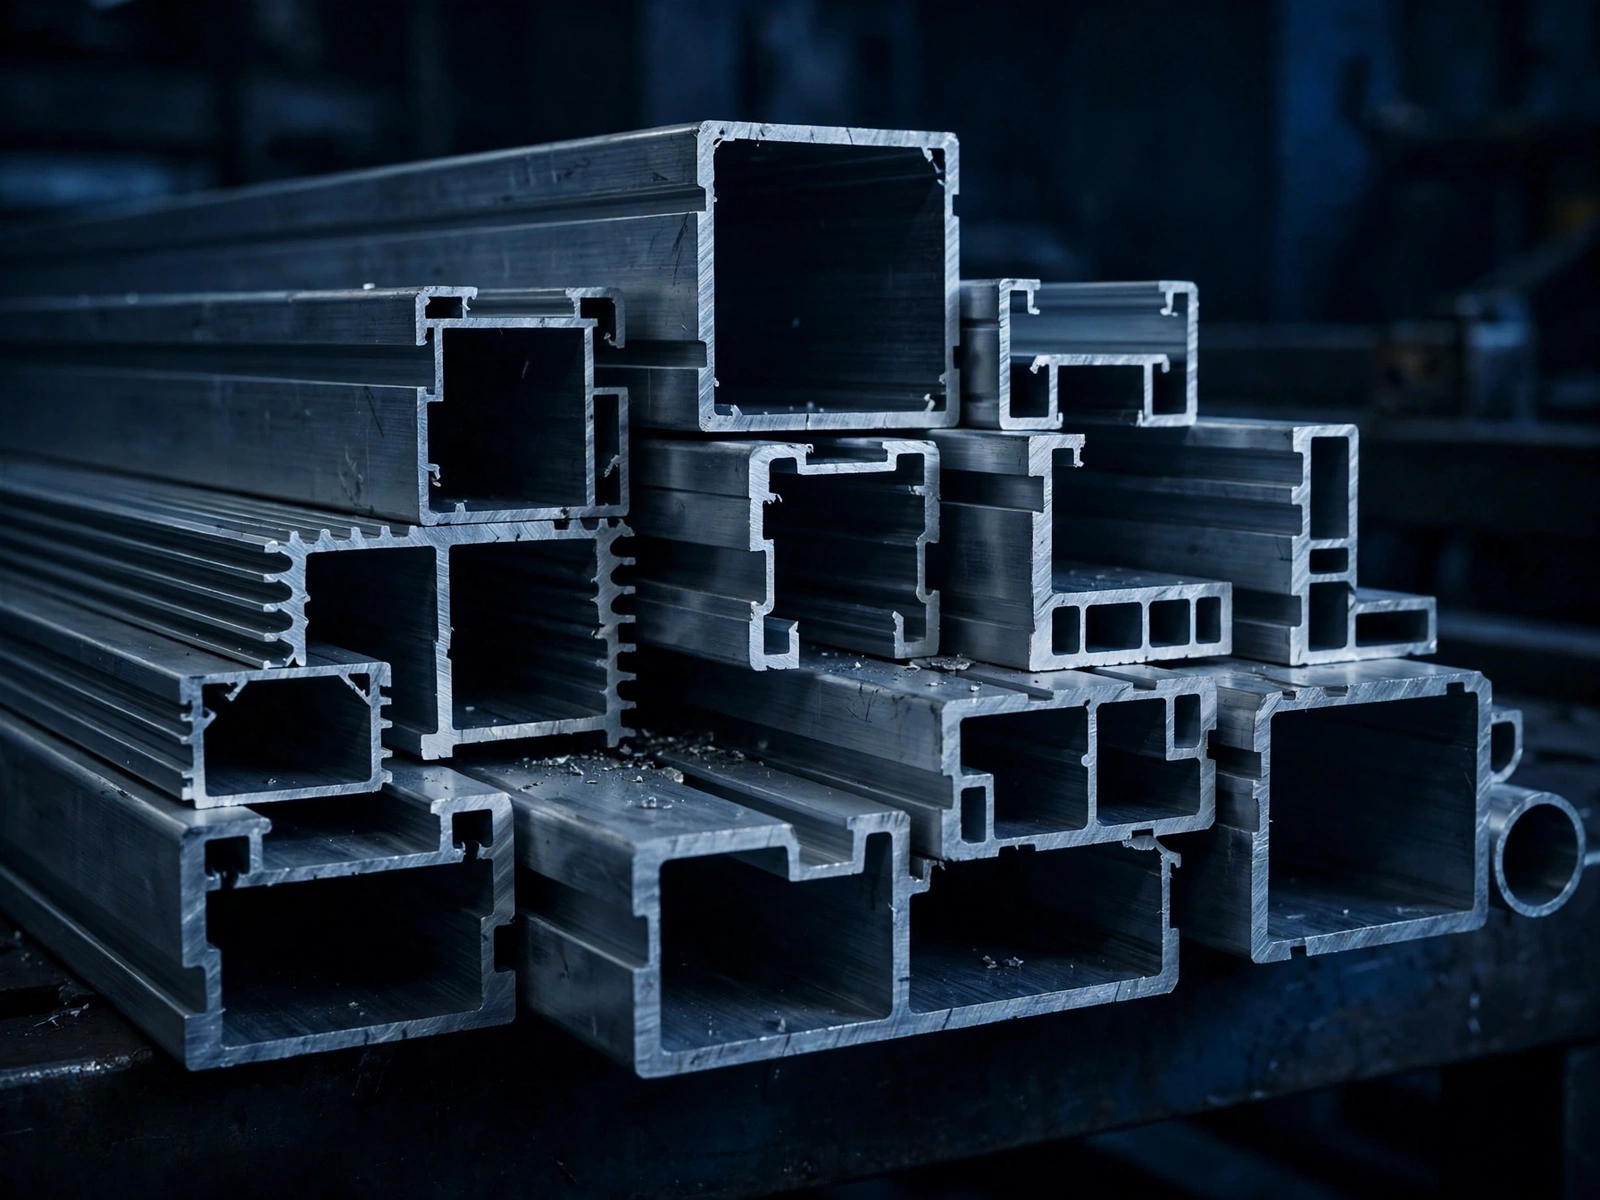
Most aircraft structures, such as stringers, stiffener sections and wing spars, use 2xxx and 7xxx series alloys bought as mill-certified extruded shapes. Distributors hold a large inventory of aircraft extrusions under Boeing BAC and AND shape numbers, and MRO shops rely on them. If your drawing calls for one of those common shapes, buy it from an approved supplier with full certification.
Where we help is the next step: custom profiles for interiors, ground equipment, UAVs and test rigs, and machining extruded aluminum into finished parts. A custom section can replace a machined part that would otherwise waste most of a solid bar, which cuts cost and lead time on repeat orders.
| Alloy | Mechanical properties | Typical use |
|---|---|---|
| 6061-T6 | Medium-high tensile strength, weldable | Ground support frames, brackets, UAV structures |
| 6063-T5/T6 | Medium strength, best surface finish | Interior trim, rails, enclosures, heat sinks |
| 2024 | Good damage tolerance under tension | Wing and fuselage structure (stock shapes) |
| 7075 | Very high strength | Highly stressed fittings (stock shapes) |
We produce custom sections in 6061 and 6063 to ASTM B221, an industry standard for extruded bar and shapes. High-strength aluminum grades are hard alloys usually bought as stock; we can machine those to your drawing when you supply certified material.
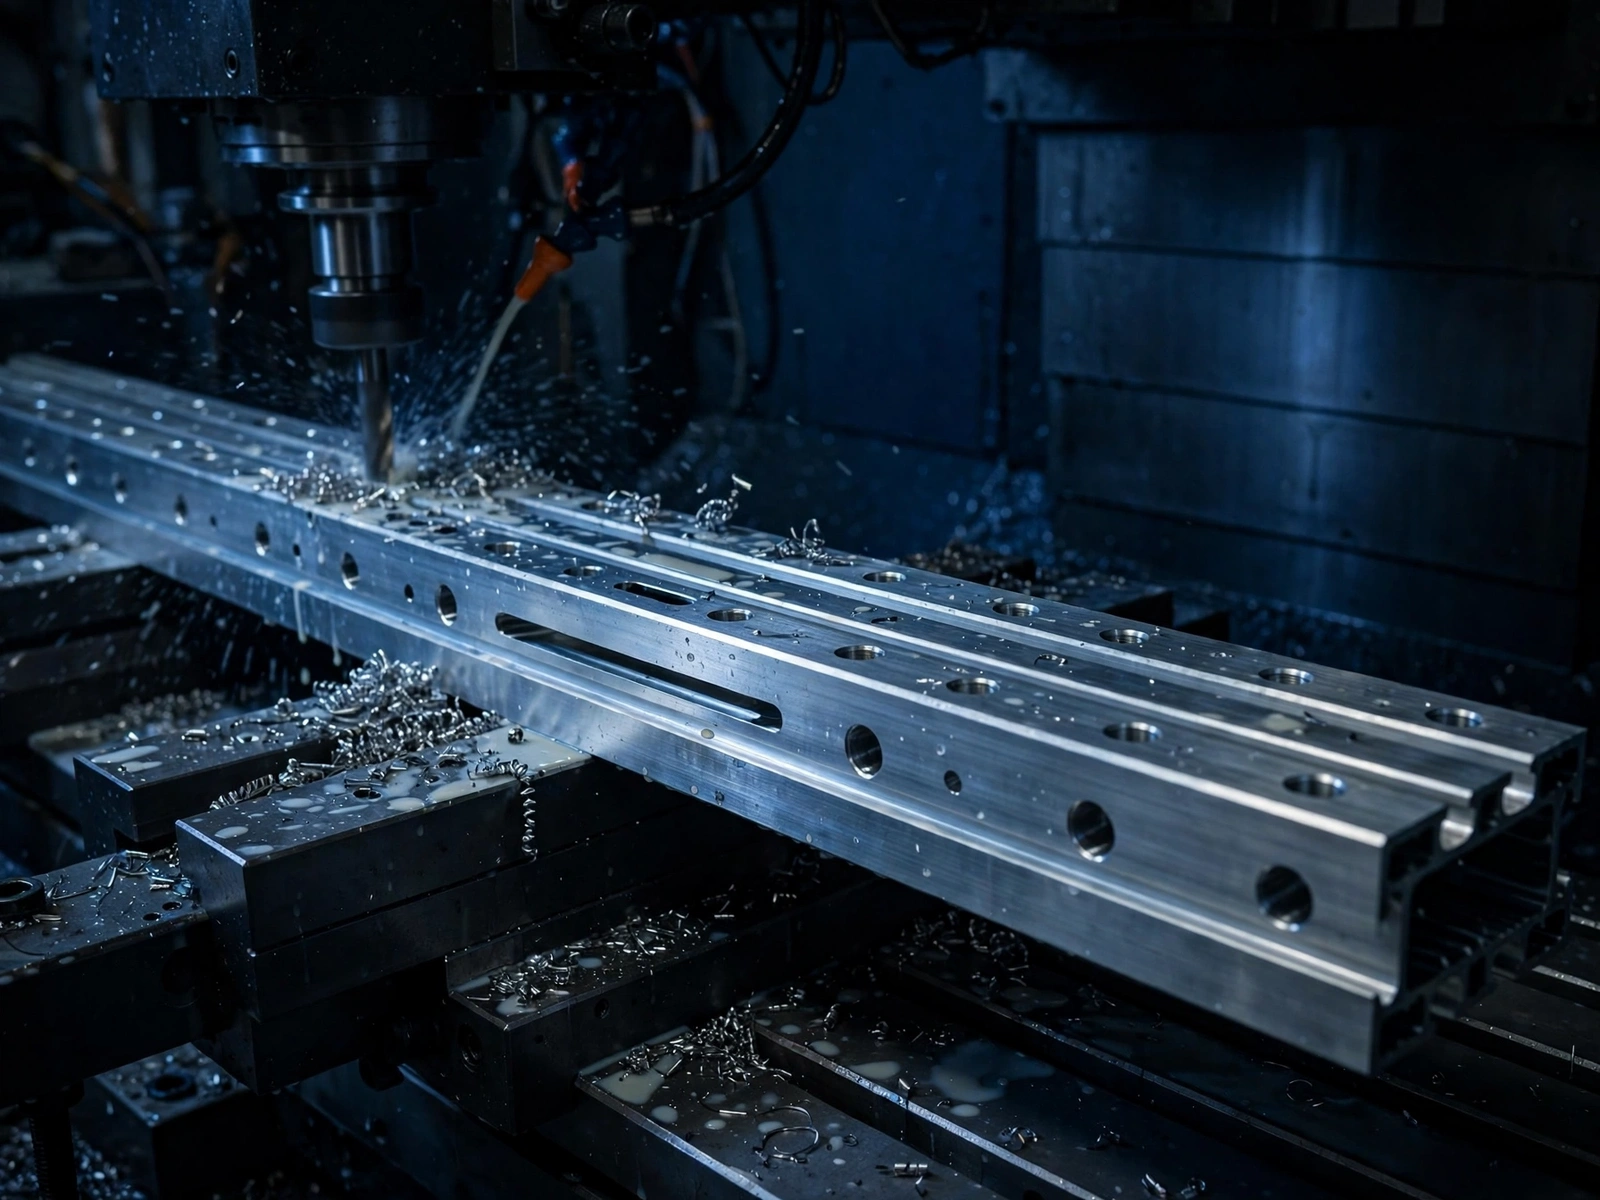
A new die typically takes 2–4 weeks, and production usually runs 2–3 weeks after samples are approved.
| Feature | Typical tolerance |
|---|---|
| Wall thickness up to 3 mm | ±0.10 mm |
| Thicker walls | ±0.30 mm |
| Machined features | Down to ±0.025 mm |
| Press capacity | 70 lines, 600 to 3,800 tons |
Extruded sections carry some twist and bow. Mating surfaces and bores that need tight tolerances are machined downstream rather than relied on as-extruded.
Machining and finishing run under our AS9100D quality system, and our extrusion plants are ISO 9001:2015 certified. We supply material certificates, dimensional reports and lot traceability on request. For flight-critical parts, your program and its FAA approval path decide whether a custom section is acceptable or whether certified stock to an AMS specification is required to protect structural integrity.