
Need expert machining solutions? Our team at Tuowei Precision is here to assist with all your manufacturing needs. Get in touch today for a quote on your ongoing or upcoming projects!
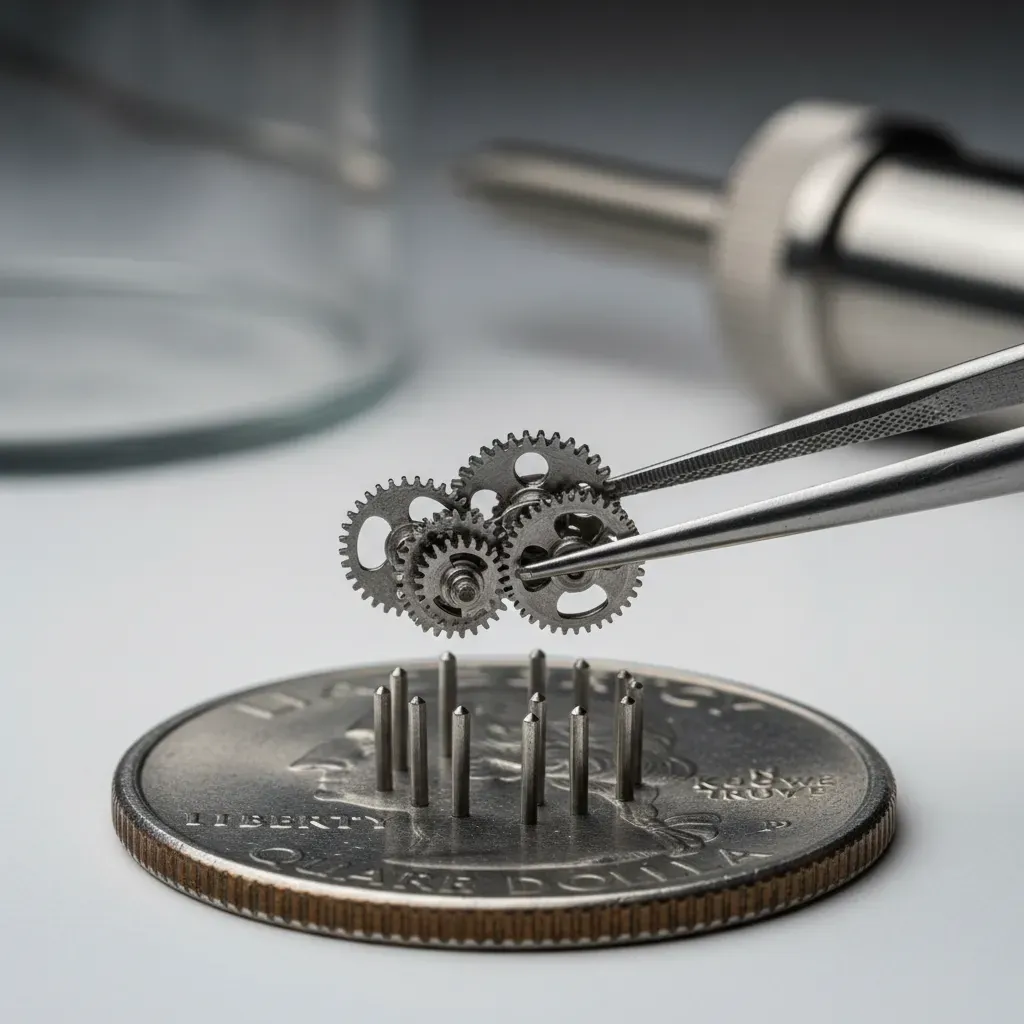
Micro machined parts are components whose features are measured in microns rather than millimeters — 0.1 mm drilled holes, 0.05 mm wide ribs, watch-scale gears and medical components that fit on a fingertip. Producing them is not just “small machining”: tools flex, chips weld, and a fingerprint’s worth of heat changes the dimension. This page defines what micro machining realistically achieves, the size and tolerance limits, how such parts are measured, and when EDM or laser processes are the better choice.
In practice, micro machining covers parts or features where:
| Process | Capability |
|---|---|
| Micro milling | End mills Ø0.1–1.0 mm; 3D features, pockets, slots; spindles to 60,000 rpm |
| Micro drilling | Holes from Ø0.05 mm; depth up to 10× diameter |
| Micro turning (Swiss) | Pins and shafts from Ø0.3 mm; L/D to 20:1 — see Swiss screw machining |
| Thread milling / tapping | From M1 (tapped), M0.8 possible by thread milling |
| Dimensional tolerance | ±0.005 mm standard; ±0.002 mm on controlled features |
| Surface finish | Ra 0.2–0.4 µm milled; Ra 0.1 µm achievable |
| Edge condition | Burr height controlled <5 µm with micro-deburring |
| Factor | Micro CNC machining | Micro wire/sinker EDM | Laser micromachining |
|---|---|---|---|
| Materials | Metals and plastics | Conductive metals only | Almost anything |
| 3D contours | Excellent | Limited (2.5D wire; sinker needs electrode) | Shallow features best |
| Hardened steel | Limited | Excellent | Good (thin) |
| Min feature | ~0.05 mm | ~0.02 mm (fine wire) | ~0.01 mm |
| Heat-affected zone | None | Minimal recast layer | Present — may need post-process |
| Deep holes | 10× dia | Excellent (EDM drilling 100× dia) | Limited |
| Typical use | 3D micro parts, pins, manifolds | Hardened dies, micro slots | Foils, stents, masks |
Machining of features roughly 0.05–1 mm in size with tolerances of 2–10 µm, using miniature tooling, high-speed spindles and micron-level metrology — typically for parts that fit within a 10 mm cube.
Tool fragility: micro end mills deflect and break at tiny chip loads, so success depends on runout control, high spindle speeds, micro chip loads and rigid, temperature-stable machines.
Setup and metrology dominate: a simple micro part may cost more to inspect than to cut. Unit prices fall steeply with quantity — prototypes carry the programming and qualification cost, production runs amortize it.
±0.005 mm is standard; ±0.002 mm is achievable on controlled features with climate control and appropriate metrology.
Tuowei Precision produces micro machined parts on high-speed milling centers and Swiss-type lathes, with vision-system metrology and per-feature burr specifications. For larger precision work see our precision machining and CNC machining services, or run the full program under contract machining. Send your drawing — quotes within 24 hours.

Written by Andy, Manufacturing Engineer at TUOWEI Precision. Andy specializes in CNC machining, precision manufacturing, and production engineering, with hands-on experience supporting projects from rapid prototyping through full-scale production. He works closely with engineering and manufacturing teams to evaluate materials, tolerances, machining processes, and design manufacturability. His articles provide practical, technically informed insights to help engineers and buyers make better manufacturing decisions, optimize production efficiency, and achieve consistent part quality. Explore TUOWEI Precision’s CNC machining and custom manufacturing solutions for your next project.
From rapid prototypes to scalable production, Tuowei Precision delivers reliable CNC machining with accuracy and consistency at every step. Start your project today.
Read our latest guides on CNC machining, materials, finishing and industry trends to make better production decisions.





