Reaction injection molding turns two liquids into a solid part inside the mold. Instead of melting plastic pellets, the process mixes an isocyanate with a polyol blend, then lets the mixture cure into a thermoset part. If you are weighing molding against prototyping first, our rapid prototyping guide explains how to test a design before any tooling is cut.
The short name is RIM, and the key difference from regular injection molding is chemistry, not just pressure. Standard molding shapes a melted thermoplastic that hardens as it cools, while RIM creates the polymer itself in the mold through a curing reaction. That difference explains the low pressures, the tooling options, and the part sizes RIM handles well.
Reaction injection molding is a process for making plastic parts by mixing two reactive liquids and letting them polymerize inside a closed mold. The mixture starts with a much lower viscosity than molten thermoplastic, so it flows easily into large or complex cavities before it cures. Once cured, the result is a thermoset part that cannot be remelted, unlike a thermoplastic part.
The chemistry is what makes RIM flexible. One side of the system is an isocyanate, and the other is a polyol blend that typically also carries a surfactant, a catalyst, and a blowing agent. Changing the blend changes the result, from a rigid structural panel to a soft foam cushion, without changing the basic process.
The rim molding process starts with metering. Two liquid streams are held in separate temperature-controlled tanks and pumped at an exact ratio into an impingement mixing head, where they collide and mix in a turbulent zone. Precise ratio control matters: even a small deviation from the target mix can change the cured part’s properties.
Next comes the low-pressure fill and the cure. One molder fills molds at just 50 to 150 psi, a fraction of injection molding pressure, and holds mold temperatures around 140 to 180 degrees Fahrenheit while the exothermic reaction turns the liquid into a solid in minutes. The part is then demolded, trimmed, and inspected.
| Step | What happens |
|---|---|
| Metering | Two liquid streams are pumped at an exact ratio from separate tanks |
| Mixing | Streams collide in an impingement mixing head and blend turbulently |
| Filling | Mixture fills the mold at low pressure (50 to 150 psi, per one molder) |
| Curing | Exothermic reaction turns the liquid into a solid in minutes (mold 140 to 180 degrees Fahrenheit) |
| Demolding | Part is removed, trimmed, and inspected |

Standard RIM makes unreinforced polyurethane parts, which suit appearance panels, housings, and other components where moderate strength is enough. Reinforced reaction injection molding, or RRIM, mixes short reinforcing fibers such as glass fiber or mica into the liquid before molding, raising stiffness and strength for more demanding parts.
Structural reaction injection molding, or SRIM, goes further. A fiber mesh is arranged in the mold first, and the polymer mixture is then molded over it, so the reinforcement sits exactly where the load will be. SRIM parts are the strongest of the three, which is why the process is chosen for high-load panels and structural components.
| Type | Reinforcement | Best for |
|---|---|---|
| Standard RIM | None | Appearance panels, housings |
| RRIM | Short fibers mixed into the liquid | Stiffer structural parts |
| SRIM | Fiber mesh pre-placed in the mold | Highest-load structural components |
Polyurethane dominates RIM because the same basic chemistry covers a wide property range. Formulations run from soft, flexible foams for seating and cushioning to rigid foams for insulation and lightweight structures, including integral-skin foam with a dense outer skin and a foamed core.
Polyurethane is the urethane polymer behind RIM — see what is urethane for the chemistry, grades and uses.
Other systems cover special needs. Polyureas, polyisocyanurates, polyesters, epoxies, and nylon 6 all appear in RIM-type processes, chosen for properties such as higher heat resistance or specific electrical behavior. The trade-off is usually higher material cost or more demanding processing, so polyurethane stays the default starting point.
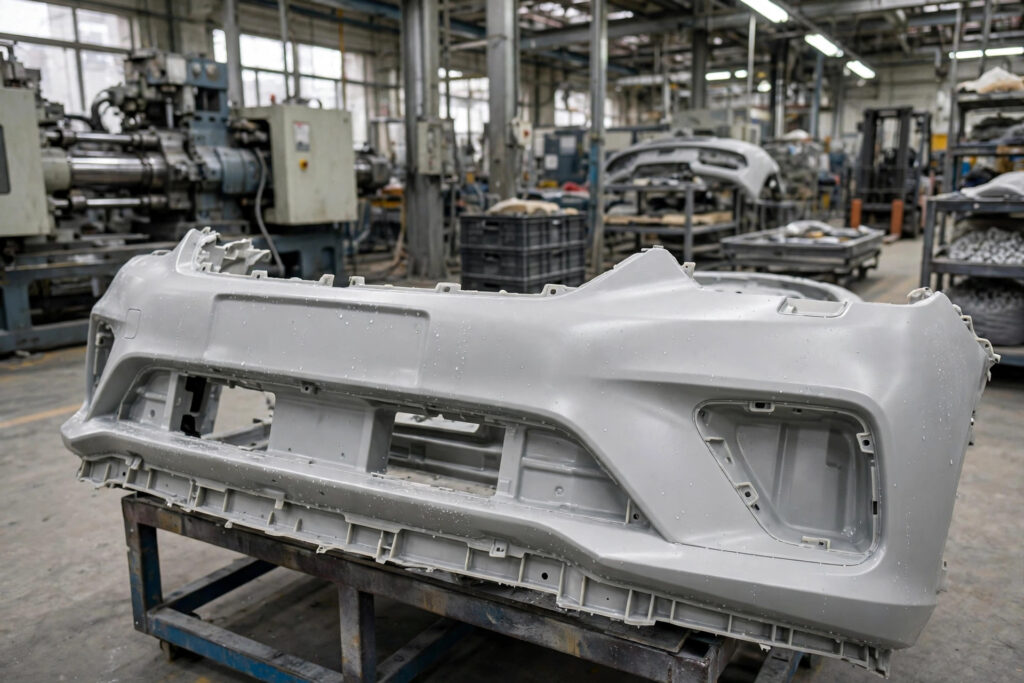
Automotive work leads RIM usage, with bumpers, spoilers, fenders, and body panels among the classic parts. The process suits these parts because large, lightweight panels can be molded without the massive presses that high-pressure molding would need, and the surface quality supports painted exterior finishes.
Other uses play to RIM’s gentle filling and encapsulation strengths. Medical housings can use insert molding to surround metal parts or electronics in a single shot, electronics enclosures benefit from the insulating properties, and construction uses window frames, architectural panels, and insulation components where weatherability and thermal performance matter.
The clearest contrast is how the part is formed. Regular injection molding melts solid thermoplastic pellets and forces the melt into a mold under high pressure, then cools it into shape. Reaction injection molding instead mixes two liquids at low pressure and cures them into a thermoset part, so the mold sees far less stress.
That contrast drives tooling and part-size choices. RIM’s low fill pressure allows aluminum tooling instead of hardened steel, which cuts tooling cost and build time, and it allows large parts and varied wall thickness in one component. Traditional molding wins on cycle speed and very high volumes, where its fast, repeatable cycles pay back the steel tool.
| Aspect | Injection molding | Reaction injection molding |
|---|---|---|
| Material state | Melted thermoplastic | Two reactive liquids |
| Pressure | High | Low (50 to 150 psi fill, per one molder) |
| Tooling | Hardened steel typical | Aluminum common |
| Part size | Limited by press | Large parts possible |
| Wall thickness | Mostly uniform | Varied in one part |
| Best volume | Very high volumes | Low-to-medium volumes |
Custom reaction injection molding means a manufacturer builds parts to a buyer’s design, material, and reinforcement specification rather than selling a standard product. Buyers usually come with a part that is too large, too complex, or too low-volume for a steel production tool, and they need the molder to advise on material choice, reinforcement, and tooling.
Before committing, ask what the manufacturer needs and what it will prove. Useful questions cover the material system and its data sheet, whether RRIM or SRIM reinforcement fits the load case, the tooling material and tool life, the inspection plan for articles, and how design changes are handled after the tool is built. Lead times vary by part size, tooling, and material availability, so treat any lead-time promise as a question, not an answer.
RIM tooling usually costs less and arrives faster than a hardened steel injection mold, because low fill pressure allows aluminum tooling and smaller equipment. That advantage matters most when the design is still changing, since aluminum tools are easier to modify than steel, and when volumes do not justify a production steel tool. Our injection mold cost breakdown explains which tooling cost drivers matter most.
The trade-offs are real. RIM cycle times run slower than injection molding because the part must cure in the mold, and the reactive raw materials cost more than commodity thermoplastic pellets. RIM therefore fits low-to-medium volumes and large or complex parts best, while very high volumes still favor traditional molding’s speed.
Most RIM defects trace back to ratio, temperature, or mixing. Metering equipment must hold the two streams at the target ratio, since even a small deviation changes cured properties, and component temperatures must stay in their specified window or the material will flow poorly or start curing before the mold fills.
Mold release and cure defects follow the same logic. Complex shapes can stick without proper mold preparation and release agent, and soft spots or poor surfaces usually point to wrong ratios, contamination, or temperature drift. Regular calibration, housekeeping, and maintenance prevent most of these failures before they reach inspection.
Reaction injection molding, or RIM, is a process that mixes two reactive liquids, an isocyanate and a polyol blend, and injects the mixture into a mold at low pressure. The liquids react and cure inside the mold into a solid thermoset part, which cannot be remelted. Low-viscosity flow allows large, lightweight, and thin-walled parts.
RIM is used most for automotive bumpers, spoilers, fenders, and body panels, where large, lightweight parts need good surface quality. It also serves medical device housings molded around inserts, electronics enclosures, and construction panels, frames, and insulation components that need weatherability and thermal performance.
The rim molding process meters two liquid streams, an isocyanate and a polyol blend, into an impingement mixing head where they mix turbulently. The mixture fills the mold at low pressure, then the exothermic reaction cures it into a solid part in minutes. The mold opens, the part is removed, trimmed, and inspected.
Regular injection molding melts solid thermoplastic pellets and forces the melt into a mold under high pressure, then cools it into shape. RIM mixes two liquids at low pressure and cures them into a thermoset part inside the mold. RIM tooling is usually cheaper, while traditional molding is faster at very high volumes.
Structural reaction injection molding, or SRIM, is the reinforced RIM variant that places a fiber mesh in the mold before the polymer mixture is injected over it. Because the reinforcement sits exactly where loads will act, SRIM parts are the strongest of the RIM family and suit high-load panels and structural components.
Start with the part’s requirements: material system, reinforcement type, part size, and expected volume. Then ask the manufacturer about its material data, RRIM or SRIM capability, tooling material and tool life, first-article inspection, and how it handles design changes. Compare answers across suppliers rather than comparing headline prices alone.
Every figure in this guide comes from one of the sources below. Where a figure describes one molder’s own process rather than an industry standard, the article says so.
Reviewed by Leon Xu, Engineer, Tuowei Precision. Last updated: November 2026. This guide gives general reaction injection molding guidance for engineers and buyers; it describes the market and the process and claims no Tuowei RIM service.