Need expert machining solutions? Our team at Tuowei Proto is here to assist with all your manufacturing needs. Get in touch today for a quote on your ongoing or upcoming projects!
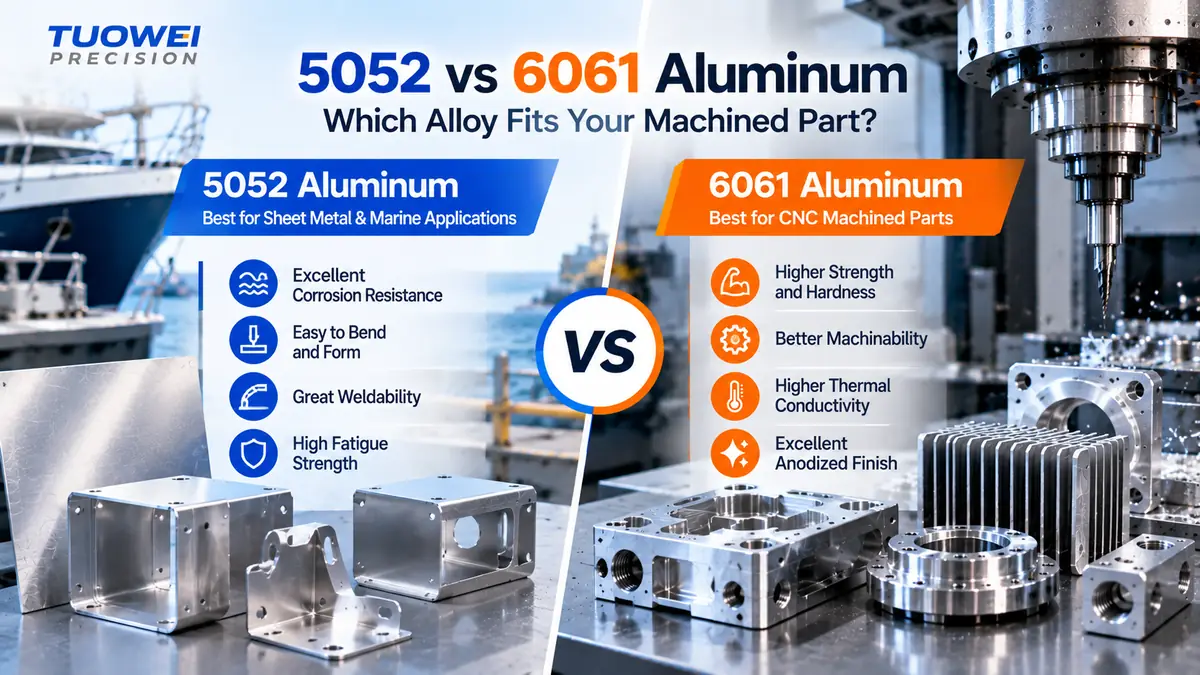
In the 5052 vs 6061 aluminum decision, the part’s main process usually settles it. Choose 6061 for CNC machined parts: it is stronger in the T6 temper, cuts cleanly, and anodizes evenly. Choose 5052 for bent sheet metal and parts exposed to salt water, because it forms tightly without cracking and resists marine corrosion better.
Quick answer: 6061-T6 has higher tensile and yield strength, better machinability, and a more uniform anodized finish. 5052-H32 bends and welds more easily and holds up better in salt water, but it is gummy to machine. If the part is milled from a block, use 6061. If it is folded from sheet, use 5052.
The difference starts with chemistry. According to the Aluminum Association’s alloy guide, 5xxx alloys use magnesium as the main alloying element, while 6xxx alloys combine magnesium and silicon to form magnesium silicide.
That one change decides how each alloy gets its strength:
Everything else in this comparison, from machinability to welding, follows from that split.
The table below shows typical values for the tempers engineers use most. Specification minimums in ASTM B209 for sheet and plate are lower, so design to the minimums, not the typical values.
| Property (typical) | 5052-H32 | 6061-T6 | Better for |
| Ultimate tensile strength | 228 MPa (33 ksi) | 310 MPa (45 ksi) | 6061 |
| Yield strength | 193 MPa (28 ksi) | 276 MPa (40 ksi) | 6061 |
| Fatigue strength | 117 MPa (17 ksi) | 96.5 MPa (14 ksi) | 5052 |
| Modulus of elasticity | 70.3 GPa | 68.9 GPa | Similar |
| Density | 2.68 g/cm³ | 2.70 g/cm³ | Similar |
| Thermal conductivity | 138 W/m·K | 167 W/m·K | 6061 |
| Heat treatable | No | Yes | 6061 |
| Machinability | Fair, gummy | Good | 6061 |
| Formability and bending | Excellent | Poor in T6 | 5052 |
| Weldability | Excellent | Good, loses strength near the weld | 5052 |
| Salt water corrosion resistance | Excellent | Good | 5052 |
| Cosmetic anodizing | Good, can look less uniform | Very good, even color | 6061 |
Two numbers in the 5052 vs 6061 comparison surprise people. 5052 has the higher fatigue strength, so it handles vibration well. And 6061 moves heat about 20% better, which matters for heat sinks and electronics housings.
6061 is easier to machine, and by a clear margin.
5052 is soft and ductile. On a mill it tends to smear, form long stringy chips, and weld itself to the tool. That leads to torn surfaces, burrs, and tool wear. It can be machined well. If a design calls for machined features in 5052-H32 aluminum, such as pockets in a formed cover, these habits help:
6061-T6 aluminum is harder, so chips break cleanly and the surface finish comes straight off the tool. That is why it is the default alloy for CNC milling housings, brackets, and fixtures, and why most shops quote it faster and cheaper per part.
Our position: if a part is mostly machined, specify 6061-T651 plate. Using 5052 for a heavily machined part usually costs more in cycle time and deburring than it saves in material.
5052-H32 aluminum is the standard alloy for bent aluminum sheet metal. It takes tight bend radii without cracking, which makes it ideal for enclosures, brackets, chassis, and covers.
6061-T6 is a poor choice for bending. It tends to crack along the outside of a tight bend. If a 6061 part must be formed, it is usually bent in a softer temper and heat-treated afterward, which adds cost and a distortion risk.
A common mistake is copying the alloy from a machined part onto a sheet metal drawing. If your metal bending supplier asks to switch a formed part from 6061 to 5052, that is usually the right call.
5052 is often called marine grade aluminum. Its magnesium content gives excellent resistance to salt water and salt spray, which is why it is used for boat parts, fuel tanks, and outdoor cabinets.
6061 also resists corrosion well in normal atmospheres, and anodizing improves it further. In constant salt water exposure, 5052 is the safer choice.
For welding, 5052 has the edge. Because it is not heat-treated, the area near the weld keeps much of its strength. 6061-T6 aluminum welds well, usually with 4043 or 5356 filler wire, but the heat destroys the T6 temper in the heat-affected zone next to the weld, so a welded 6061 frame is weaker at the joints unless it is heat-treated again.
Both 5052 and 6061 anodize, and both work with Type II anodizing. The difference is appearance.
6061 gives an even, consistent color, which is why it is the usual choice for cosmetic parts. 5052 can come out slightly less uniform, and it may show a different shade from 6061 even in the same tank.
It also matters for aluminum sheet metal parts that sit next to machined parts, and that is where many assemblies go wrong.
Plenty of products use both alloys, and this is where the 5052 or 6061 question gets less clear-cut. A classic case: an enclosure with a machined 6061 base and a bent 5052 lid.
It works, but two problems come up often:
Neither problem is a reason to avoid mixing alloys. Just plan for it on the drawing.
“Aluminum” on a drawing is not a specification, whether you pick 5052 or 6061. Write the alloy, temper, and product form:
Ask for a mill test certificate with each batch. It confirms the alloy and temper you received match the drawing.
| Your part | Best choice | Why |
| Milled housing, bracket, or fixture | 6061-T651 | Strength, clean machining, even anodizing |
| Bent enclosure, cover, or chassis | 5052-H32 | Tight bends without cracking |
| Marine or salt spray exposure | 5052 | Better salt water corrosion resistance |
| Welded frame that must stay strong | 5052, or 6061 re-heat-treated | 5052 keeps more strength at the weld |
| Heat sink or thermal plate | 6061 | Higher thermal conductivity |
| Vibration-loaded thin part | 5052 | Higher fatigue strength |
When a part is both machined and bent, settle 5052 vs 6061 by the dominant process and design around the weaker property.
No. 6061-T6 has higher tensile and yield strength than 5052-H32, with typical yield strength around 276 MPa compared with 193 MPa. However, 5052 has higher fatigue strength and keeps more of its strength after welding, so in some vibration-loaded or welded parts it can perform better overall.
Yes, but it is harder to machine well than 6061. 5052 is soft and gummy, so it forms stringy chips and built-up edge on the tool. Sharp tools, good chip evacuation, and conservative cutting parameters help. For heavily machined parts, 6061-T651 is usually faster and cheaper per part.
You can, but 6061-T6 often cracks on tight bends. Use a generous bend radius, or form the part in a softer temper and heat-treat it afterward. For bent sheet metal parts, 5052-H32 is usually the better choice because it forms tight radii without cracking.
5052 is generally better for marine use. Its magnesium content gives excellent resistance to salt water and salt spray, which is why it is called marine grade aluminum. 6061 also performs well outdoors, especially when anodized, and is chosen when the part needs higher strength.
Raw material prices are usually close and depend on form and market conditions. The bigger cost difference comes from processing. 5052 is cheaper to bend and weld, while 6061 is cheaper to machine. Compare the finished part price, not the price per kilogram of stock.
For the 5052 vs 6061 aluminum choice, start with the process. Machined parts belong in 6061, bent sheet parts in 5052, and marine or welded assemblies lean toward 5052.
Tuowei Precision works with both alloys, including 6061-T651 plate for machined parts and 5052 sheet for formed parts. Send your drawing through the Tuowei Precision homepage for a DFM (design for manufacturing) review, and our engineers will flag alloy or temper changes before cutting starts.
Written by Andy, Manufacturing Engineer at TUOWEI Precision. Andy specializes in CNC machining, precision manufacturing, and production engineering, with hands-on experience supporting projects from rapid prototyping through full-scale production. He works closely with engineering and manufacturing teams to evaluate materials, tolerances, machining processes, and design manufacturability. His articles provide practical, technically informed insights to help engineers and buyers make better manufacturing decisions, optimize production efficiency, and achieve consistent part quality. Explore TUOWEI Precision’s CNC machining and custom manufacturing solutions for your next project.
From rapid prototypes to scalable production, Tuowei Precision delivers reliable CNC machining with accuracy and consistency at every step. Start your project today.
Keep updated on the real CNC machining, industry trends, and production insights in Tuowei Precision, but is installed to enable you to make better production decisions.