

By Leon Xu, Engineer, Tuowei Precision · November 2026
Laser cutting is a thermal cutting process that uses a focused, high-power laser beam to melt, burn or vaporize material along a programmed path, while a jet of gas clears the molten material out of the cut. It is the standard way to cut flat sheet metal parts, from thin stainless brackets to carbon steel plate around 25 mm thick.
So what is laser cutting best at, and where does it fall short? This guide answers both.
Short answer: A laser cutter concentrates light from a fiber or CO2 source into a spot a fraction of a millimeter wide. CNC motion moves that spot along the part outline, the beam melts the material, and assist gas such as oxygen, nitrogen or air blows it out of the cut. The result is a clean, narrow cut with no tool contact.
Below we cover how the process works step by step, the three main laser types, which materials cut well, what accuracy to expect, what the process is used for, and the design mistakes that cause most rejected parts.
Laser is an acronym for Light Amplification by Stimulated Emission of Radiation. A laser source produces a beam of light that is a single wavelength and travels in step, which means it can be focused to an extremely small, intense spot. Put enough power into that spot and it heats metal past its melting point almost instantly.
A laser cutting machine is a CNC machine. Computer numerical control moves the cutting head, or the sheet, along a path generated from your CAD file. Because nothing touches the part, there is no tool wear and no cutting force, so thin and delicate parts cut as cleanly as heavy ones.
A few terms come up again and again:
Here is how laser cutting works on a typical sheet metal job, from file to finished blank:
What goes wrong is usually visible on the bottom edge. If speed or gas pressure is off, molten metal sticks there as dross. Very small holes can show a bulge where the lead-in starts. And when many small parts are nested tightly in thin sheet, heat builds up in the remaining skeleton and can warp the last parts cut. Good programming, not more laser power, fixes most of these.
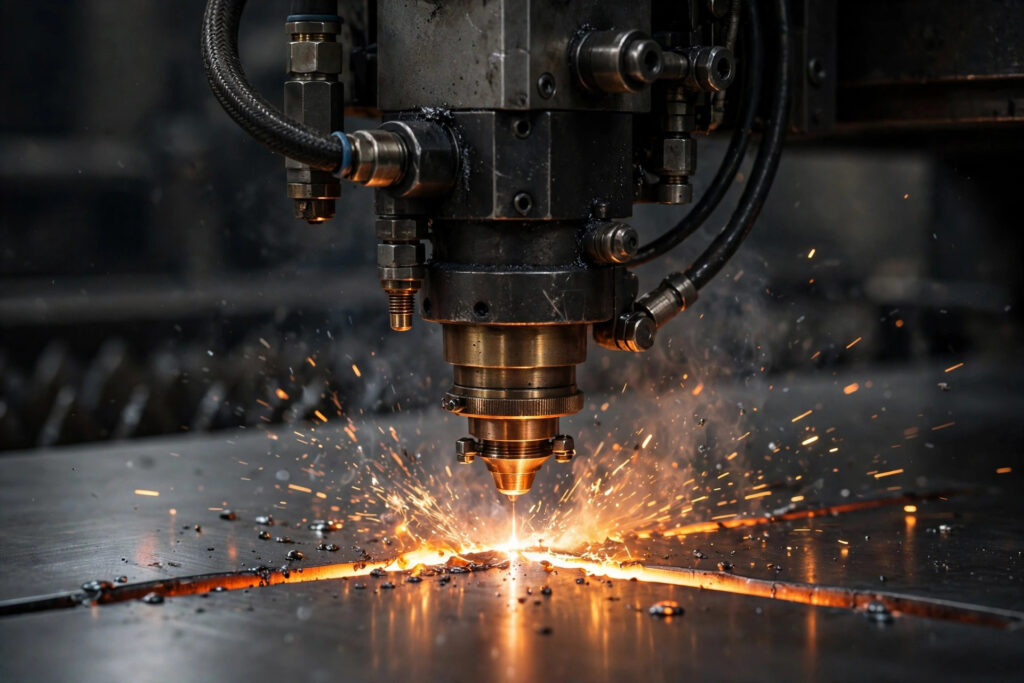
The gas choice changes speed, cost and the edge you get, so it is worth understanding even if you never run a machine.
| Gas | How it works | Typical use | Edge result |
|---|---|---|---|
| Oxygen | Reacts with hot steel and adds heat to the cut | Carbon steel, especially thicker plate | Fast, with a dark oxide layer on the edge |
| Nitrogen | Inert, simply blows the melt out | Stainless steel and aluminum | Bright, clean, oxide-free edge |
| Compressed air | Mostly nitrogen with some oxygen | Thin sheet where cost matters | Low cost, with slight edge oxidation |
Our view: if a carbon steel part will be powder coated or welded, ask for nitrogen-cut edges or plan to remove the oxide. Coating applied over oxygen-cut scale can flake off at the edges later.
| Laser type | Wavelength | Best for | Notes |
|---|---|---|---|
| Fiber | About 1.07 µm | Steel, stainless, aluminum, copper, brass | Energy efficient, handles reflective metals, fast on thin and medium sheet |
| CO2 | 10.6 µm | Acrylic, plastics, wood, rubber, foam, thin metals | Leaves a polished edge on acrylic; long wavelength reflects off bare aluminum and copper |
| Nd:YAG | 1.064 µm | Fine precision work, thick or hard alloys, drilling | High peak power in pulses; less common for general sheet cutting today |
Fiber lasers generate light inside a doped glass fiber, which gives a small spot and high efficiency. CO2 lasers excite a gas mixture, and their longer wavelength is absorbed well by organic materials. Nd:YAG lasers use a solid crystal and deliver short, powerful pulses.
Our view: for sheet metal parts, fiber is the default today. CO2 still earns its place on acrylic, wood and other non-metals, and Nd:YAG is a specialist tool. At Tuowei Precision we run all three types, with laser sources up to 10 kW, so the laser is matched to the material rather than the other way round.
Metals are the main industrial use. We regularly cut carbon steel, stainless steel (including 304 and 316), aluminum alloys such as 5052, 6061 and 7075, copper, brass and titanium. Non-metals include acrylic, engineering plastics, rubber, foam and wood.
Maximum thickness depends on the material and laser power. On our equipment:
| Material | Maximum thickness |
|---|---|
| Carbon steel | Under 25 mm (0.98 in) |
| Stainless steel | Under 15 mm (0.59 in) |
| Aluminum | Under 15 mm (0.59 in) |
| Copper | Under 12.7 mm (0.5 in) |
Some materials should not be laser cut at all. PVC releases chlorine compounds that are toxic and corrode the machine. PTFE gives off fluorine compounds when heated. Polycarbonate tends to burn and discolor rather than cut cleanly. Fume extraction and beam enclosure matter for every laser, and OSHA lists the laser hazard standards that apply to these machines in general industry.
Laser cutting is accurate enough for most sheet metal work without secondary operations. These are the capabilities of our laser cutting process:
| Specification | Value |
|---|---|
| General dimensions | ISO 2768-c, typically ±0.2 mm (0.008 in) |
| Repeatability | ±0.05 mm (0.002 in) |
| Positioning accuracy | ±0.10 mm (0.004 in) |
| Kerf | About 0.5 mm (0.02 in) |
| Minimum part size | 2 × material thickness, minimum 1 mm (0.04 in) |
| Edge condition | Matte, with fine vertical lines |
| Lead time | 5 to 7 days |
ISO 2768-1 defines four general tolerance classes: fine (f), medium (m), coarse (c) and very coarse (v). Stating the class on your drawing tells the shop which tolerance applies to every dimension you have not toleranced individually.
Two details trip people up. First, the CAM software offsets the cutting path by half the kerf, so the part comes out at the drawn size. Do not add kerf to your drawing yourself. Second, on thick plate the cut edge has a slight taper and a wider heat-affected zone, so holes that need a precise fit are better drilled or reamed after cutting.
Accuracy also depends on the part, not just the machine. A long, thin part can move slightly as stresses in the sheet release, so very tight flatness or straightness may need extra steps.
Laser cutting turns flat stock into profiles, so it shows up wherever sheet or plate parts are needed. Common uses include:
The industries that use laser cutting most include automotive, aerospace, consumer electronics, medical devices, robotics and automation, industrial machinery and construction. In most of these, laser cutting is the first step of a wider sheet metal fabrication workflow that continues with bending, welding, hardware insertion and finishing.
| Process | Best at | Limits |
|---|---|---|
| Laser cutting | Thin to medium sheet, fine detail, narrow kerf | Thickness ceiling; reflective metals need fiber; small heat-affected zone |
| Plasma cutting | Thick conductive plate at high speed and low cost | Wider kerf, rougher and slightly beveled edge; conductive metals only |
| Waterjet cutting | Almost any material, very thick stock, no heat | Slower; abrasive adds running cost |
| Turret punching | High volumes of standard holes, louvers and forms | Needs a tool for each shape; less suited to complex contours |
Our view: laser is the first choice for most sheet parts up to medium thickness because it combines accuracy, speed and no tooling. Switch to waterjet when heat would damage the material, and to plasma for thick structural plate where edge quality matters less than cost.
Yes. Metal is the most common material for industrial laser cutting. Fiber lasers cut carbon steel, stainless steel, aluminum, copper, brass and titanium. Maximum thickness depends on power and material; our machines cut carbon steel up to about 25 mm and stainless steel or aluminum up to about 15 mm.
The three main laser types are fiber, CO2 and Nd:YAG. Fiber lasers lead in metal cutting, CO2 lasers suit acrylic, wood and other non-metals, and Nd:YAG lasers handle specialist precision work. By technique, cutting is done by fusion with nitrogen, flame cutting with oxygen, or vaporization.
A CNC laser cutter is a laser cutting machine whose motion is controlled by computer numerical control. The controller reads a program generated from your CAD file and moves the cutting head along each contour, setting power, speed and gas. Nearly all industrial laser cutters are CNC machines.
Parts are usually drawn in CAD software such as SolidWorks, Fusion or AutoCAD and exported as DXF or STEP files. CAM and nesting software then arranges parts on the sheet, assigns cutting parameters and generates the G-code that the laser machine runs.
Laser cutting uses a focused light beam and gives finer detail, narrower kerf and cleaner edges on thin and medium sheet. Plasma cutting uses an ionized gas arc, works only on conductive metals and is faster and cheaper on thick plate, but leaves a rougher edge.
At Tuowei Precision we run fiber, CO2 and Nd:YAG laser cutters with sources up to 10 kW, and our quality system is certified to ISO 9001:2015, ISO 13485, IATF 16949:2016 and AS9100D. Typical laser cutting lead time is 5 to 7 days.
Upload a STEP, STP, SLDPRT, DXF, IPT, PRT or SAT file with the material, thickness, quantity and finish. Our engineers review every drawing before quoting and flag design issues before cutting. Parts that also need tapped holes or milled pockets move straight into our CNC shop, so they arrive ready to assemble. Start with our laser cutting services page.
About the author: Leon Xu is an engineer at Tuowei Precision. He reviews customer drawings, gives DFM feedback and plans CNC machining processes to hold tight tolerances.





