
¿Necesitas soluciones de mecanizado especializadas? El equipo de Tuowei Precision está a tu disposición para ayudarte con todas tus necesidades de fabricación. ¡Ponte en contacto con nosotros hoy mismo para solicitar un presupuesto para tus proyectos actuales o futuros!
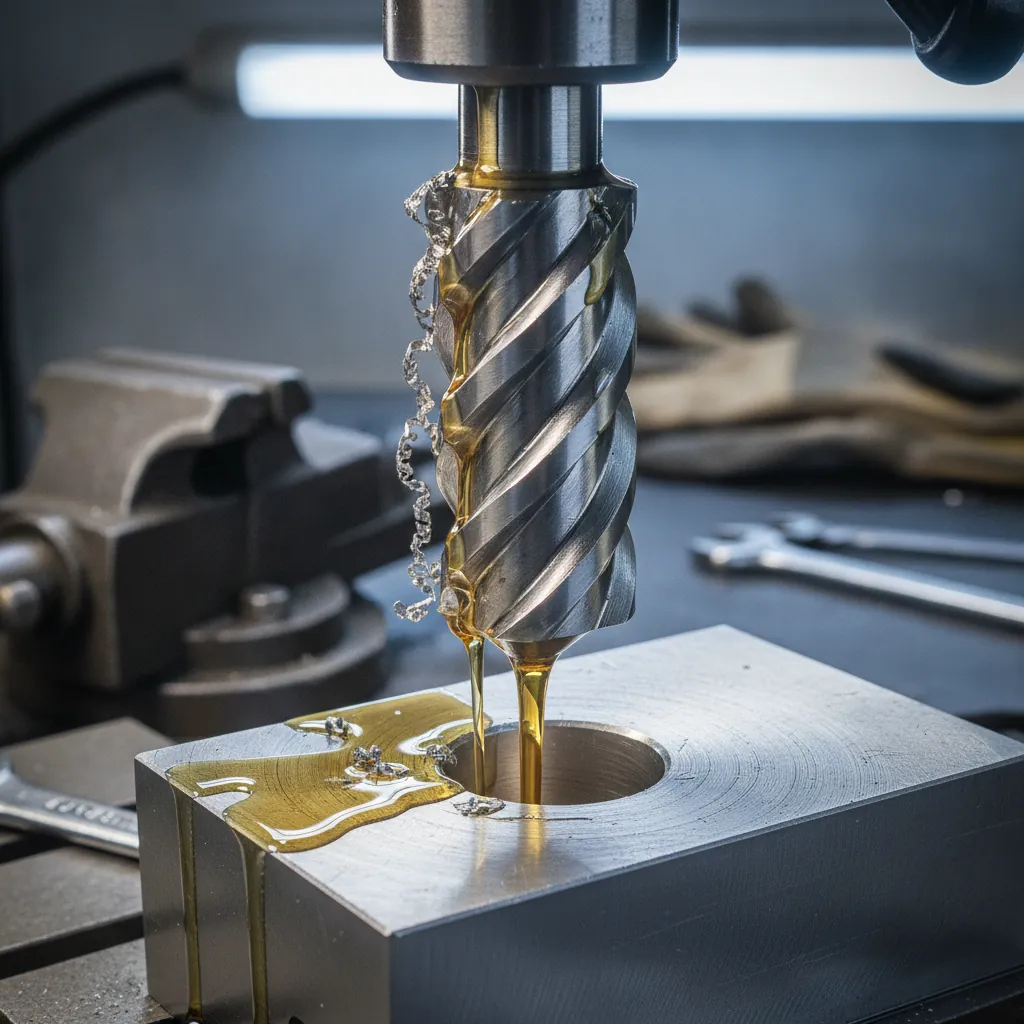
Reaming is the finishing operation that turns a drilled hole into a precision hole. A reaming tool — a multi-fluted cutter with a slight lead chamfer — removes a small, controlled amount of stock from a pre-drilled hole, bringing it to exact size with a fine finish. If a drawing says Ø8 H7, a drill alone will not get you there; a reamer will. This guide defines the process, covers the tool types, and gives the working numbers: stock allowances, speeds, feeds and tolerances.
Reaming is a sizing and finishing process in which a rotary multi-edge cutting tool (the reamer) enlarges an existing hole by a small amount — typically 0.1–0.5 mm on diameter — to achieve accurate diameter (IT6–IT8), good roundness, and surface finish of Ra 0.4–1.6 µm. Because the reamer follows the existing hole, it improves size and finish but, like honing, cannot correct hole position — that is boring’s job.
| Reamer type | Personaje | Use case |
|---|---|---|
| Chucking (machine) reamer | Straight or spiral flute, fixed size | Standard production reaming on drill press, lathe, CNC |
| Hand reamer | Long lead taper, square drive end | Bench fitting; the long taper self-aligns in the hole |
| Adjustable reamer | Sliding blades, size range | Repair work, odd sizes; lower precision |
| Taper pin reamer | 1:50 taper | Taper pin holes in assemblies |
| Bridge/car reamer | Long taper, aggressive | Aligning structural bolt holes |
| Carbide / coated reamer | Solid carbide or TiAlN coated | Hardened steels, abrasive alloys, high-volume CNC |
Spiral-flute reamers deserve a note: left-hand spiral pushes chips forward (through holes), right-hand spiral pulls chips back (blind holes), and spiral flutes bridge interrupted cuts like keyways without chatter.
| Diámetro del orificio | Reaming allowance (on Ø) |
|---|---|
| Under 4 mm | 0.1 mm |
| 4–11 mm | 0.15–0.2 mm |
| 11–25 mm | 0.2–0.3 mm |
| 25–50 mm | 0.3–0.5 mm |
Too little stock and the reamer burnishes and rubs — glazed, work-hardened, undersize holes. Too much and it acts like a drill — oversize, poor finish, short tool life. For an H7 hole, the standard chain is: drill → (bore if position matters) → ream.
| Material | Speed (HSS) | Feed |
|---|---|---|
| Aluminio | 25–30 m/min | 0.3–0.8 mm/rev |
| Acero dulce | 12–18 m/min | 0.2–0.5 mm/rev |
| Alloy steel (treated) | 6–10 m/min | 0.15–0.3 mm/rev |
| Stainless (304/316) | 5–8 m/min | 0.15–0.3 mm/rev |
| Cast iron | 10–15 m/min | 0.3–0.6 mm/rev |
| Brass / bronze | 20–30 m/min | 0.3–0.8 mm/rev |
Rule of thumb: ream at half the drilling speed and twice the drilling feed. High speed glazes and chatters; generous feed keeps the edges cutting. Carbide tooling roughly doubles these speeds.
| Factor | Reaming | Boring | Honing |
|---|---|---|---|
| Corrects position | No | Sí | No |
| Size accuracy | IT6–IT8 | IT6–IT9 | IT5–IT6 |
| Finish (Ra) | 0.4–1.6 µm | 0.8–3.2 µm | 0.05–0.8 µm |
| Speed/cost | Fastest, cheapest | Flexible, slower | Highest precision, costliest |
| Ideal para | Standard fit holes (H7) | Located/large/odd-size holes | Sliding-seal bores |
| Problema | Causa probable | Corregir |
|---|---|---|
| Oversize hole | Misalignment, built-up edge, excess speed | Floating holder, lower speed, proper coolant |
| Undersize / glazed | Too little stock, worn reamer | Increase allowance, sharpen or replace |
| Poor finish | Chip packing, high speed, low feed | Spiral flutes, halve speed, double feed, cutting oil |
| Chatter / lobing | Rigidness lacking, even flute spacing | Shorter stickout, unequal-spacing reamer |
| Bell-mouthed entry | Spindle/hole misalignment | Floating reamer holder |
A finishing operation where a multi-fluted reaming tool removes 0.1–0.5 mm from a pre-drilled hole to deliver precise diameter (typically H7), roundness, and a fine Ra 0.4–1.6 µm finish.
Drilling creates the hole but holds only ±0.05–0.1 mm with a rough finish; reaming refines that hole to within ~±0.01 mm with a near-polished wall. Drill first, ream second — a reamer cannot start its own hole.
No. A reamer follows the existing hole’s axis. If true position matters, single-point bore the hole to correct location, then ream to final size.
Typically 0.15–0.3 mm on diameter for common sizes (see table above) — enough that every flute cuts, little enough that the reamer sizes rather than hogs.
H7 dowel fits, press-fit bearing bores, taper pin holes — reamed holes are routine callouts in the parts we ship daily through our Servicios de mecanizado CNC y mecanizado de precisión lines, including CNC turned parts with on-axis reamed bores. Upload your drawing — we quote within 24 hours with full dimensional reports available.

Escrito por Andy, ingeniero de fabricación en TUOWEI Precision. Andy está especializado en mecanizado CNC, fabricación de precisión e ingeniería de producción, y cuenta con experiencia práctica en el apoyo a proyectos que abarcan desde la creación rápida de prototipos hasta la producción a gran escala. Trabaja en estrecha colaboración con los equipos de ingeniería y fabricación para evaluar materiales, tolerancias, procesos de mecanizado y la facilidad de fabricación de los diseños. Sus artículos ofrecen información práctica y con base técnica para ayudar a ingenieros y compradores a tomar mejores decisiones de fabricación, optimizar la eficiencia de la producción y lograr una calidad constante de las piezas. Descubre las soluciones de mecanizado CNC y fabricación a medida de TUOWEI Precision para tu próximo proyecto.
Desde prototipos rápidos hasta la producción a gran escala, Tuowei Precision ofrece un mecanizado CNC fiable, con precisión y uniformidad en cada paso. Empieza tu proyecto hoy mismo.
Lee nuestras últimas guías sobre mecanizado CNC, materiales, acabados y tendencias del sector para tomar mejores decisiones de producción.





