需要专业的加工解决方案?拓维 Proto 团队可满足您的所有加工需求。现在就联系我们,为您正在进行或即将进行的项目报价!
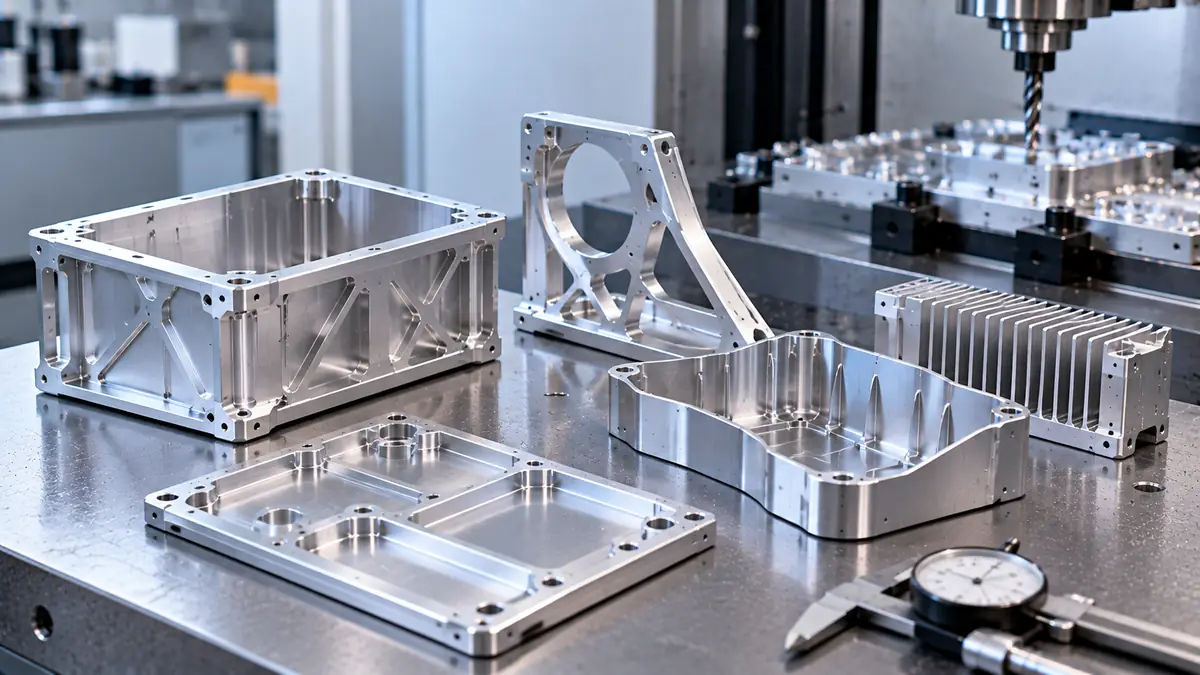
Thin-wall aluminum machining goes wrong in two ways. The wall vibrates while it is being cut, which leaves chatter marks and a wavy surface. Or the part moves after it comes off the machine, because internal stress was released unevenly or the clamps bent it. Both are controlled the same way: keep the wall supported for as long as possible, cut with light and even forces, and start from stress-relieved stock.
简短回答: To prevent warping, use stress-relieved T651 plate, remove material evenly from both sides, rough everything before finishing, and hold the part without forcing it flat. To prevent chatter, use the shortest, sharpest tool that reaches, take light radial finishing cuts, finish tall walls in steps from the top down, and tune spindle speed.
The rest of this guide explains why each of those steps works, with the physics behind them, so you can judge which ones a particular part needs.
There is no universal number. Published guides call a wall “thin” below 2 mm, below 1.5 mm, or above a height-to-thickness ratio anywhere from 10:1 to 20:1. The disagreement makes sense once you see that thickness alone does not decide how a wall behaves.
What matters is stiffness, and stiffness depends on both height and thickness. A wall standing up from a pocket floor behaves roughly like a cantilever beam. Under a sideways cutting force at its free edge, its deflection rises with the cube of its height and falls with the cube of its thickness.
So a 1 mm wall 5 mm tall may machine easily. At 40 mm tall, the same wall is a real problem. In practice, a wall is “thin” when the cutting force is large enough, relative to its stiffness, to push it out of position or set it vibrating.
That is why this guide treats thin aluminum walls by height and thickness together rather than by a single minimum.
Five mechanisms cause almost every problem with thin-walled parts. They show up at different moments, which is the quickest way to tell them apart.
| Cause | What you see | When it shows up | Main fix |
| Cutting-force deflection | Wall thicker at the top than planned, taper | During the cut; measures wrong on the machine | Lighter radial cuts, finish in steps from the top down |
| Chatter (self-excited vibration) | Wavy marks, noise, poor finish | During the cut | Shorter tool, tuned spindle speed, more support |
| Residual stress release | Part bows or twists after unclamping | After the part is released | T651 stock, balanced removal, rough-rest-finish |
| Clamping distortion | Part springs out of flat after unclamping | When clamps come off | Even, lower clamping force, vacuum or conformal support |
| 热 | Size drifts during the cut, then changes as it cools | During and just after the cut | Coolant, sharp tools, measure at a stable temperature |
Two of these, stress and clamping, only appear after the part is released. A part can look perfect on the machine and still fail inspection. That is also why “warping” and “chatter” need different fixes: one is a static problem of stress and support, the other a dynamic problem of vibration.
Two simple relationships from beam theory explain most thin-wall behavior.
Deflection. For a wall treated as a cantilever, deflection under the same force is proportional to height cubed divided by thickness cubed. Double the height and deflection rises eight times. Halve the thickness and it also rises eight times.
Natural frequency. The first natural frequency of the wall, the frequency at which it prefers to vibrate, is proportional to thickness divided by height squared. Halve the thickness and the frequency halves. Double the height and it drops to a quarter.
The table below uses the cantilever formula for a 6061 aluminum wall, with a modulus of 68.9 GPa (10.0 × 10³ ksi, from the NASA 6061 handbook) and a density of 2.70 g/cm³. Real walls joined to other walls or corners are stiffer than this idealized case, so treat the numbers as a comparison, not a prediction.
| 壁厚 | Wall height | Approximate first natural frequency |
| 2 mm | 20 mm | 4,080 Hz |
| 1 mm | 20 mm | 2,040 Hz |
| 2 mm | 40 mm | 1,020 Hz |
| 1 mm | 40 mm | 510 Hz |
Now compare that with the cutter. The tooth-passing frequency is spindle speed times number of flutes divided by 60. A three-flute end mill at 12,000 RPM hits the wall 600 times a second, or 600 Hz. The tall 1 mm wall at 510 Hz sits close to that forcing frequency, while the short 2 mm wall is far above it.
This is the practical meaning of “thin.” As a wall gets taller and thinner, its natural frequency falls toward the range the cutter is exciting, and small changes in speed or depth start to matter a lot. It also explains why milling thin walls gets harder so quickly as they grow taller.
One more point that surprises designers: switching from 6061 to 7075 does not make a wall stiffer. The NASA handbooks list moduli of 10.0 and 10.3 × 10³ ksi for the two alloys, only about 3% apart. 7075 is much stronger, but a wall that flexes in 6061 will flex almost as much in 7075.
Chatter is a self-excited vibration. Each tooth leaves a slightly wavy surface. The next tooth meets that wave, and if the timing is wrong, the vibration grows with every pass. On thin-walled aluminum parts, the vibrating part may be the wall rather than the tool, and the wall’s behavior changes as material comes off.
Machinists map where cutting is stable using a stability lobe diagram, which plots the maximum chatter-free depth of cut against spindle speed. The stable “lobes” sit at speeds where the tooth-passing frequency lines up with a whole-number fraction of the system’s natural frequency. NIST researchers showed that these stability limits also shift with tool overhang length, and that tuning the overhang can raise the chatter-free material removal rate (Schmitz et al., NIST).
In practice, these are the levers:
Spindle speed advice varies by machine, holder and tool. A speed that works on one machine may chatter on another. A tap test, which measures the tool’s frequency response with an instrumented hammer, gives the real stability lobe for a specific setup.
Rolled aluminum plate is quenched after solution heat treatment, and the fast cooling locks stress into it: compression near the surfaces, tension in the middle. While the plate is whole, these stresses balance. Machine away material unevenly and the balance breaks, so the remaining part bends to find a new equilibrium. That is machining distortion, and it often appears only after the part is unclamped.
The first line of defense is the material form. Under the Aluminum Association’s temper system (ANSI H35.1), a “51” suffix such as T651 means the product was stress relieved by stretching after solution heat treatment, with a permanent set of 1½ to 3% for plate. That stretch evens out much of the quenching stress, which is why 6061-T651 and 7075-T651 plate stay flatter after heavy pocketing than unstretched material.
Our position: for any thin-walled aluminum part cut from plate, specify T651. The small premium is far cheaper than scrapped parts.
Strategy matters as much as stock:
Heat treating to relieve stress is limited for T6 and T651 aluminum. Heating near or above the aging temperature changes the temper and lowers strength, so thermal stress relief should only be used if the heat treatment and properties are approved for the part.
The same logic applies to thin-wall parts cut from extrusions or forgings. The stress pattern is different, but uneven removal still releases it unevenly, and the same balanced sequence still helps.
Stock form decides how much stress a part starts with, which makes it the first defense against machining distortion. For thin-walled aluminum parts, the temper suffix is the quickest guide:
在此情况下,合金的类型不如形状重要。6061-T651是加工铝制薄壁件时的默认选择;7075-T651能提高强度,但不会增加刚度。.
夹紧造成的变形可能与切割造成的变形一样严重。将薄板强行压平固定在夹具上时,虽然夹紧期间板面保持平整,但松开后会发生回弹,导致误差被错误地切入到不该出现的位置。.
针对薄壁零件,良好的夹具设计能够分散受力,并在模具施加压力的位置对零件提供支撑:
对于薄壁铝制零件,例如用于 消费电子产品, 通常的做法是结合两种加工方式:先固定实心坯料对外部进行粗加工,然后利用已粗加工的特征固定工件,或者使用真空夹具或贴合夹具,对薄壁部分进行精加工。.
在加工薄壁件时,刀具路径的选择决定了作用在壁面上的力如何分布,因此这是同时减少挠曲和抖动的最经济有效的方式。.
刀具挠曲和壁厚挠曲会叠加。当细长的刀具向外弯曲,而薄壁也在向外弯曲时,壁厚在顶部可能会比程序规定得厚得多。我们的 数控铣削服务 正因如此,团队会共同规划退刀顺序和刀具长度,并在加工过程中随时检查壁厚,而不仅仅是在最终检验时才进行检查。.
铝的导热性很好,但薄铝壁的质量很小,无法有效吸收热量。切割产生的热量会迅速升高壁的温度,因此壁在加工过程中会膨胀,冷却时又会收缩。结果就是,该零件在机床上测量时尺寸正确,但在工作台上测量时却显示尺寸不足或变形。.
保持温度稳定的方法:
对于必须干式加工的薄壁零件,应采用较浅的切削量,并在粗加工与精加工之间留出更长的时间间隔。.
通常是这样,是的。A 5 轴数控加工 该设置通过两种方式有助于薄壁零件的加工。.
首先,一次装夹即可加工多个加工面。每次重新装夹都可能导致薄壁零件变形,因此装夹次数越少,装夹误差就越少,各特征之间的对准精度也越高。.
其次,通过倾斜刀具或工件,即使使用较短的刀具也能加工深壁孔。由于刀具刚度会随着悬伸量的增加而急剧下降,因此使用较短的刀具是解决颤振问题最有效的方法之一。.
其取舍在于:每小时费率更高,但编程时间也更长。对于单面带有特征的简单薄板,采用夹具设计合理的3轴加工方案通常更具性价比。.
在车床上车削的薄壁铝制零件(如环、套筒和圆形壳体)会带来一个铣削零件所没有的问题:卡盘。 标准的三爪卡盘会在三个点上夹紧薄壁环。环在夹紧状态下被车削成圆形,松开后又会弹回略呈三叶状的形状。.
Common fixes:
The principle is the same as machining thin walls on a mill: spread the holding force, and never ask the fixture to hold the part in a shape it does not want to keep.
Many problems with thin aluminum walls can be removed at the design stage for almost no cost.
对于 航空航天零部件, where weight targets push thin aluminum walls thinner still, these choices usually decide whether a part can be made repeatably at all.
Thin-walled parts can pass or fail inspection depending on how they are held while measured. A part flexible enough to change shape under its own weight, or under a light clamp, is what the standards call a non-rigid part.
ISO 10579 covers how to dimension and tolerance non-rigid parts. It lets the drawing state whether a requirement applies in the free state, with the part unrestrained, or in a restrained condition that imitates how it will be held in assembly. ASME Y14.5 uses a free-state symbol for the same purpose. Without that note, the shop and the customer may measure the same part two different ways and get two different answers.
Temperature matters too. ISO 1 sets 20 °C as the standard reference temperature for dimensional specifications. Thin aluminum parts warm quickly during cutting and cool quickly afterward, so they should reach a stable room temperature before final measurement.
Practical inspection steps:
These patterns most often turn thin-wall parts into scrap:
Most of these cost nothing to fix once the cause is understood. The difficult part is diagnosing which mechanism is at work, which is why noting when the problem appears, during the cut or after release, is the first step.
Successful thin-wall aluminum machining comes from treating the wall as a flexible structure through the whole process. Start with stretched T651 stock, rough evenly and let the part settle, hold it without forcing it, and finish with short, sharp tools in steps that keep the thin section supported.
If you have a thin-walled housing, bracket or aerospace part to quote, send the model and drawing to 拓维精密. Our engineers will review wall heights, fixturing and inspection conditions before cutting, and our 数控加工服务 cover both prototypes and production runs.
Q: What is the minimum wall thickness for machining aluminum?
A: There is no single minimum, because wall height matters as much as thickness. Deflection rises with height cubed and falls with thickness cubed, so a short 1 mm wall can machine easily while a tall one chatters. Add ribs to tall walls and confirm limits with your machinist for each geometry.
Q: How do you prevent chatter when milling thin walls?
A: Use the shortest, sharpest tool that reaches, take light radial finishing cuts, and finish tall walls in steps from the top down so stock below supports the cut. If chatter persists, change spindle speed up or down, try a variable-pitch end mill, or support the wall with a filler.
Q: Why do thin-wall aluminum parts warp after machining?
A: Usually because residual stress from quenching is released unevenly, or because clamping forced the part flat during cutting. Using stretched T651 plate, removing material evenly from both sides, and releasing the clamps after roughing before the finish pass all reduce the movement.
Q: How do you hold thin-wall parts without distorting them?
A: Spread the holding force. Vacuum fixtures, soft jaws shaped to the part, fitted inserts and sacrificial tabs all hold without point pressure. Tighten clamps evenly and only as much as the cut needs, because an over-clamped thin part springs back out of shape when it is released.
Q: Is climb milling better for thin walls?
A: Usually for finishing aluminum, because the chip goes from thick to thin and the tool rubs less, which improves finish. On a very flexible wall, the direction the cutting force pushes the wall also matters, so confirm the choice on a first part before running production.

作者:安迪,图威精密制造工程师。. 安迪专攻数控加工、精密制造和生产工程领域,在从快速原型制作到大规模量产的整个项目过程中拥有丰富的实践经验。他与工程和制造团队紧密合作,共同评估材料、公差、加工工艺以及设计可制造性。 他的文章提供了实用且具有技术深度的见解,旨在帮助工程师和采购人员做出更明智的制造决策、优化生产效率,并确保零件质量的一致性。欢迎了解图威精密的数控加工和定制制造解决方案,为您的下一个项目提供支持。.
从快速原型制作到可扩展的生产,Tuowei Precision 提供可靠的数控加工服务,在每个环节都确保精度与一致性。立即启动您的项目。.
随时了解拓维精工的真实数控加工、行业趋势和生产见解,安装拓维精工是为了让您做出更好的生产决策。.