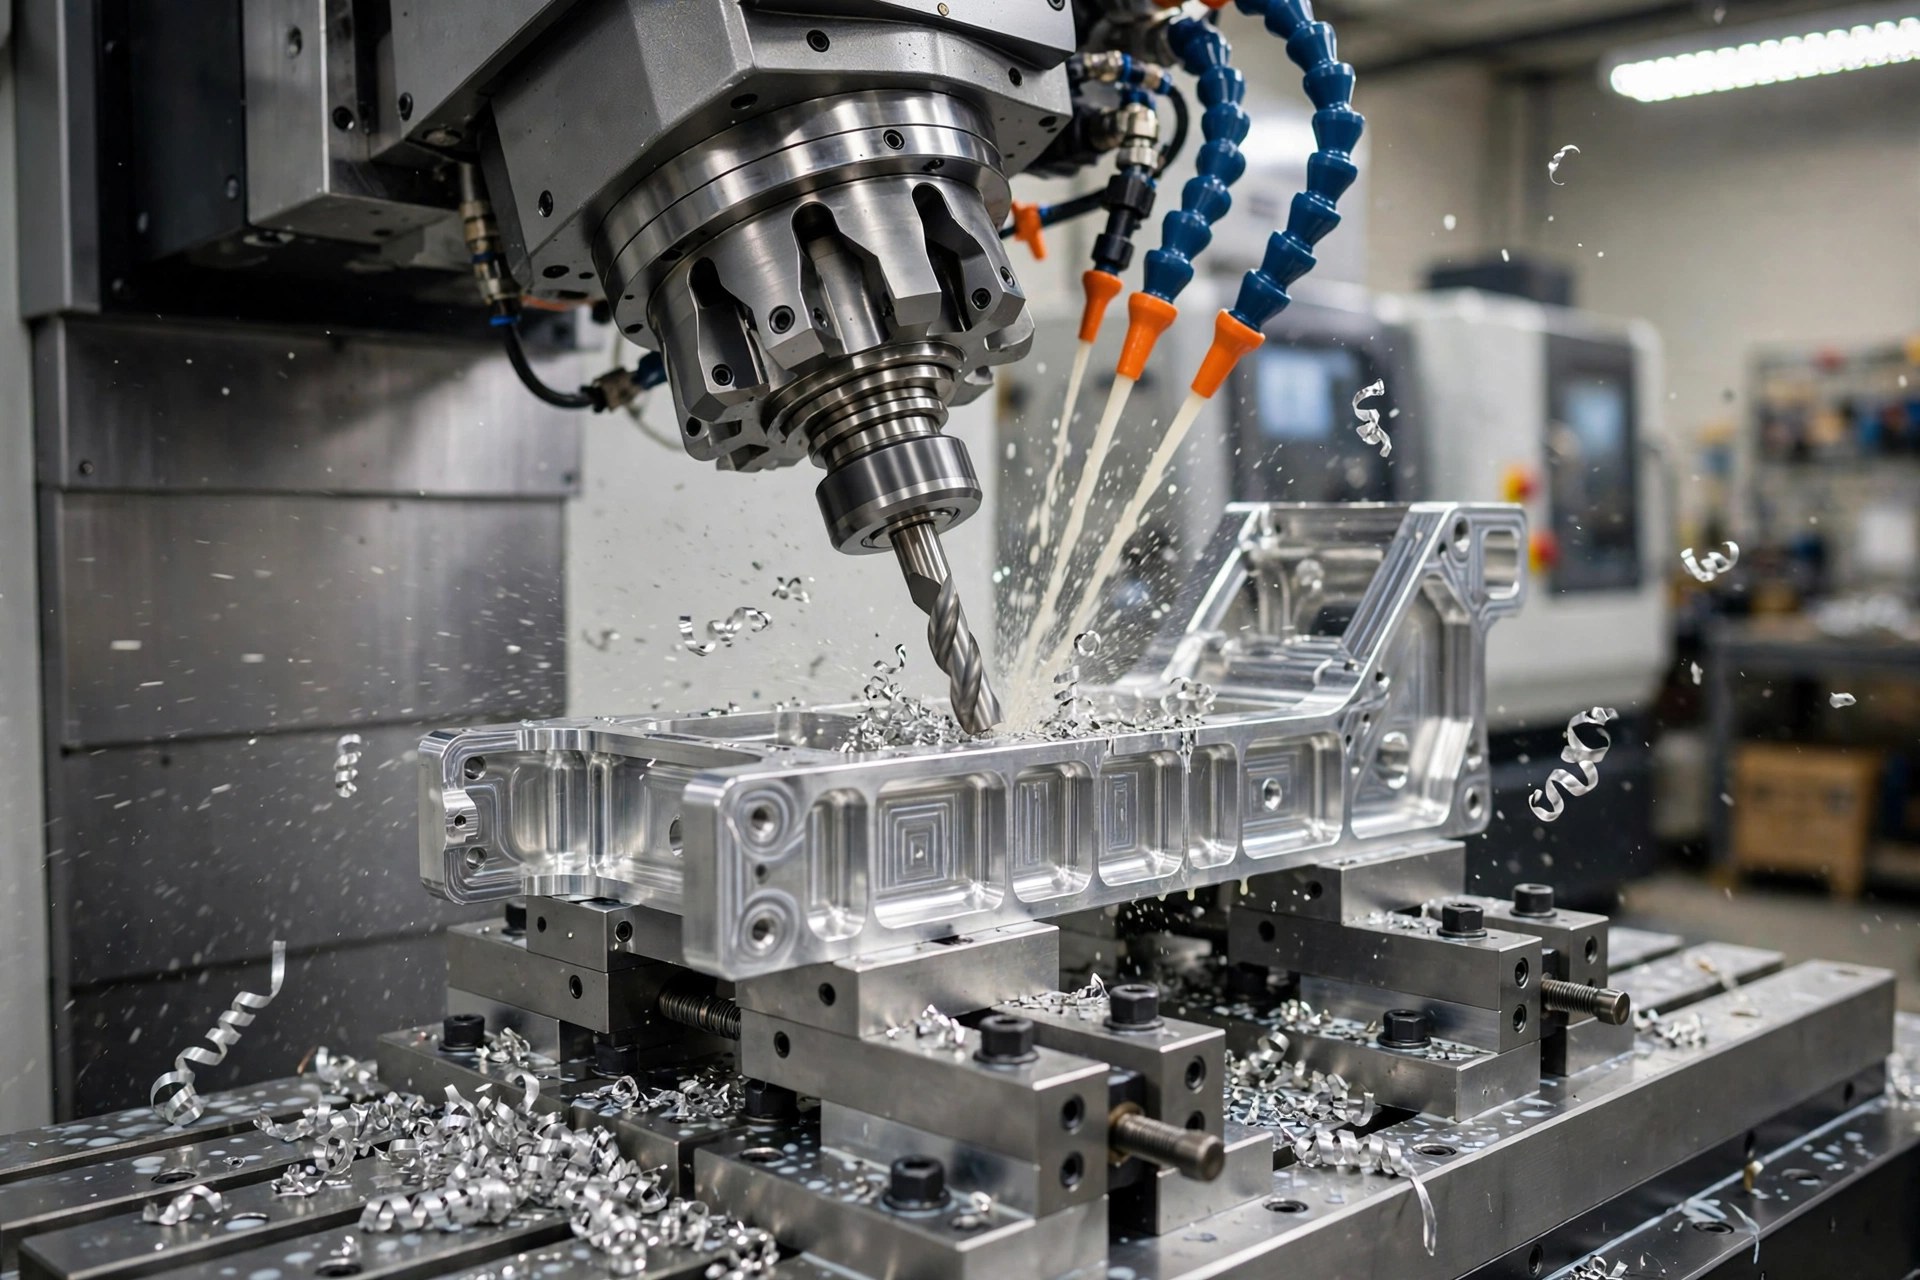
2024 aluminum machining is the process of cutting copper-rich 2024 on computer numerical control (CNC) equipment, usually from 2024-T3 or T351 stock, into precision parts. It machines well in its heat-treated tempers, but it corrodes easily, distorts if internal stress is not managed, and cannot be fusion joined. Aerospace uses it for fatigue-loaded skins, fittings and brackets.
That short answer hides most of what matters on the shop floor. 2024 is not a difficult grade to cut. It is an alloy that punishes small planning mistakes: the wrong stock form, a missing finish callout, or a part left bare for a week between operations. Most of the cost of machining aluminum sits in these planning decisions, not in the cutting itself.
This guide covers the properties of 2024 aluminum that affect machining, the problems we see most often, how to tool and fixture it, and where it earns its place in aircraft structure.
Aluminum 2024 — aluminum alloy 2024 in the European EN naming — is a wrought aluminum alloy in the 2xxx series, the family that uses copper as its main alloying element. As a heat-treatable aluminum alloy, it draws its strength from its chemical composition: copper first, then magnesium and manganese. Other aluminum families are built differently: aluminum–silicon alloys for casting, aluminum–magnesium alloys for marine sheet. The registered limits under the Aluminum Association designation system are roughly:
| Element | Content (% by weight) |
|---|---|
| Copper (Cu) | 3.8 to 4.9 |
| Magnesium (Mg) | 1.2 to 1.8 |
| Manganese (Mn) | 0.3 to 0.9 |
| Silicon (Si) | 0.5 max |
| Iron (Fe) | 0.5 max |
| Zinc (Zn) | 0.25 max |
| 铝质 | Balance |
The copper is what makes 2024 strong after heat treatment. It is also the reason 2024 corrodes faster than 6061 and takes anodizing poorly. In plain terms, this is high-strength aluminum that must be protected. Unlike a cast aluminum alloy, 2024 starts life as an ingot that is rolled, drawn or extruded, which is why its properties are so consistent.
You will see 2024 under other names on international drawings. EN AW-2024 is the European designation, AlCu4Mg1 is the chemical symbol, 3.1355 is the German Werkstoff number, and A92024 is the UNS number. They describe the same base chemistry, although temper names and property limits can differ between standards. All of them name the same aluminum alloy, whatever spelling the drawing uses. The familiar equivalents follow the same pattern in European catalogs: 6061 aluminum alloy, 7075 aluminum alloy and 6082 aluminum alloy. Aluminum is one of the lightest structural metals an engineer can choose, roughly a third the density of steel, which is why its high strength-to-weight ratio matters so much in airframe design.
The numbers below for aluminum 2024 come from published test reports rather than supplier tables. Values change with temper, product form and thickness, so treat them as a reference and design to the minimums in the governing specification. Values are stated in megapascals (MPa) and pounds per square inch (psi), the units aircraft stress engineers work in. Together these mechanical properties explain the strength and fatigue resistance the grade is known for, and in mechanical engineering practice they are the numbers that drive alloy choice for fatigue-loaded parts.
| 物业 | 2024-T3 value | Source |
|---|---|---|
| 极限拉伸强度 | 73,000 psi (503 MPa) | NACA TN 2389, test sheet |
| 屈服强度 | 54,000 psi (372 MPa) | NACA TN 2389, test sheet |
| 伸长率 | 18.2% | |
| Young’s modulus (elastic modulus) | approx. 10,600 ksi (73 GPa) | Published alloy data |
| 密度 | 2.78 g/cm³ | Published alloy data |
| 疲劳裂纹扩展 | 2 to 4 times as many cycles as 7075-T6 to reach the same crack length | NASA TN D-5390 |
| 可进行热处理 | 是 | Aluminum Association |
| Fusion joining | 不建议 | General industry practice |
Two things in this table shape how a machinist treats 2024.
First, the 18% elongation. 2024-T3 is tough and slightly ductile, so it forms a longer, more continuous chip than 7075-T6. Chip control matters more. Anyone who has machined aluminum knows the chip shape tells you how the cut is really going.
Second, the crack growth result. Designers pick 2024 because cracks grow slowly through it. That only pays off if the machined surface does not create new crack starters, which puts real weight on finish quality at holes, fillets and edges. On this alloy, surface finish is a design requirement, not a cosmetic one.
In the T3, T351 and T851 tempers, 2024 machines well. It is hard enough to shear cleanly rather than smear, it holds size, and it can take a bright finish with sharp tools. Its machinability is rated close to the 7xxx grades and noticeably better than soft aluminum grades like 5052 or 6063, and its ease of machining surprises engineers who expect a high strength alloy to fight the cutter. It also responds well to high-speed machining strategies with light radial engagement, which is why aluminum specialists keep 2024 near the top of their list for fatigue parts.
The annealed O temper is a different story. It is soft and gummy, builds up on the cutting edge, and leaves a torn surface. If a part must be formed in O or W temper, it is usually heat treated before the precision features are machined. Machinists call this the difference between good machining and a gummy, torn finish: same aluminum, different properties once treated.
Compared with 6061 aluminum, 2024 runs at similar spindle speeds and feeds in most aluminum milling work. It wears tools slightly faster because of its higher strength, and its chip is stringier. Against the 7xxx grades, it is a little more forgiving on tool wear.
Most problems with 2024 parts trace back to planning, not cutting. These are the ones that show up on our inspection reports most often.
Rolled plate and drawn bar carry internal stress. Remove a large pocket from one side and the part springs. On thin-walled aerospace parts, the movement can exceed the tolerance band after the part comes off the fixture. Thin-walled aluminum parts of any grade behave this way; 2024 just leaves less margin for error. The deformation is elastic, so it stays hidden until the part leaves the fixture.
The fix starts with material selection and stock choice. 2024-T351 plate has been stretched to relieve stress, so it moves far less than unstretched T3 or T4 stock. Then rough the part, release the clamps, let it settle, and take the finish passes last.
The alloy's toughness produces chips that wrap around tools and scratch finished walls. High-pressure coolant, a tool with a polished flute, and adequate chip load (rather than rubbing at light feeds) keep chips short.
At low cutting speeds, or with a dull or coated tool that grips aluminum, material sticks to the tool edge. The result is a torn surface and dimensions that drift through a batch. Sharp, uncoated or ZrN-coated carbide with a high positive rake reduces it, and polished flutes made for aluminum reduce it further.
This one catches buyers out. Bare 2024 can show staining or pitting within days in a humid shop, especially if water-based coolant is left sitting on the aluminum metal surface. Parts waiting for second operations or finishing should be cleaned, dried and protected. The root cause is the copper-rich microstructure: the same copper that gives 2024 its strength also gives it lower corrosion resistance compared to 6061, so its corrosion resistance can never be taken for granted and protection has to be planned, not assumed.
The ductile chip leaves burrs on drilled holes and milled edges. Drilling leaves the worst burrs, because the drill breaks through into air. On a fatigue-loaded part, a burr at a fastener hole is a ready-made crack initiation site. Deburring is not cosmetic on 2024; it is part of the fatigue design. Every aluminum part we ship gets its edges broken for the same reason.
2024 cracks and loses strength when fusion joining is attempted. In weldability terms it sits at the bottom of the aluminum family. A machining error cannot be built up and recut. That raises the cost of scrap and makes first-article checks more important than on 6061.
This is the sequence our engineers follow for a typical milled 2024-T351 part on a modern CNC machine:
Complex fittings with compound angles usually go to 5 轴数控加工, which cuts the number of setups. Fewer setups means fewer re-clamps and less chance of stress-induced movement between operations. Our machining capabilities for aluminum parts range from simple flat profiles to five-axis housings with tight tolerances held across every setup.
One honest caveat: cutting parameters depend heavily on the CNC equipment, the tool holder and the part, and on the cutting forces the part geometry creates. Take the tool maker’s recommended speeds, in revolutions per minute, and feeds for your exact cutter as the starting point, not a generic chart. That discipline is what separates precision metal fabrication from general job-shop work.
The temper on the drawing affects both the finished properties and how the part behaves during machining. Choosing the right aluminum alloy starts with temper, because tempering and aging set the final strength and machinability. Heat treating and aging are what turn a soft, formable blank into a structural part. The table below summarizes the tempers we machine most often.
| 性情 | 其含义 | Machining notes |
|---|---|---|
| 2024-O | Annealed | Soft and gummy; not used for finished precision parts |
| 2024-T3 | Solution treated, cold worked, naturally aged | Common for aluminum sheet; machines well; can move on heavy pocketing |
| 2024-T351 | T3 plus stress relief by stretching | Best choice for machined plate parts; minimal distortion |
| 2024-T4 | Solution treated, naturally aged | Similar machining to T3; used where forming comes first |
| 2024-T851 | Solution treated, stretched, artificially aged | Higher yield, lower toughness; very stable during machining |
Our position: for machined machine parts cut from plate, specify 2024-T351 unless the design needs something else. It is the temper that best matches what machinists and designers both want, stable stock and the fatigue performance 2024 is chosen for. Ask any shop that machines aluminum plate daily and you will hear the same answer.
T851 is worth considering when dimensional stability matters more than toughness. Its strength properties are a step up, but it does give up some of the damage tolerance that makes 2024 attractive in the first place, so that trade belongs with the design engineer.
2024 is widely used in aircraft structure and has been for decades, because of one property: it resists fatigue crack growth better than most other high strength aluminum alloys. Parts that see repeated tension, flight after flight, benefit most, and designers describe the result as good fatigue resistance under repeated tension loading. Its specific strength, the strength-to-weight ratio designers actually size with, is the other reason designers accept the extra protection work this alloy needs.
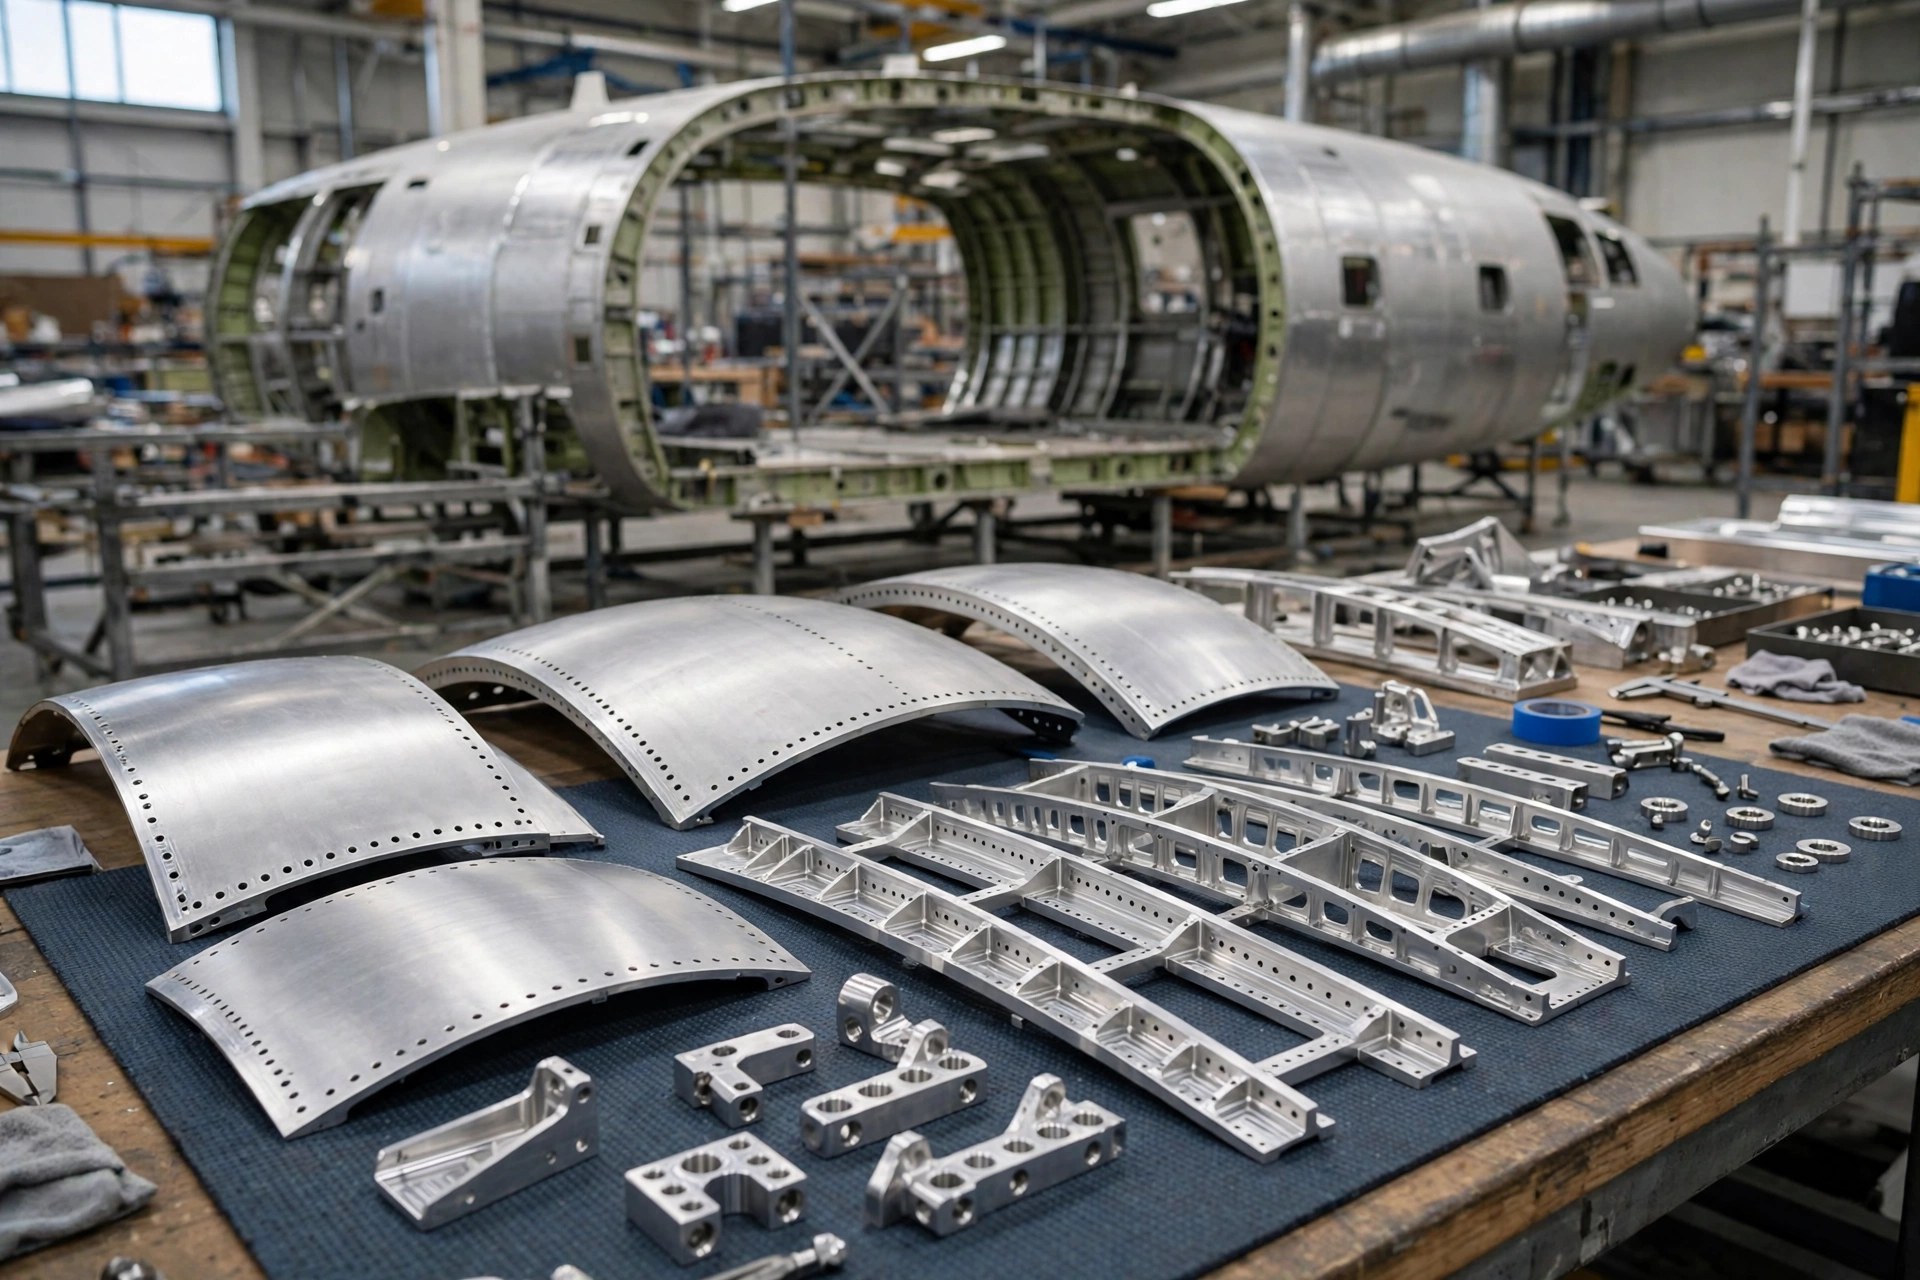
Typical aerospace applications for 2024 aluminum components include:
Upper wing skins and compression-loaded members usually move to 7xxx alloys such as 7075, where static and compressive strength drive the sizing. If you are weighing 7075 and 2024 for a specific part, our 2024 vs 7075 aluminum comparison walks through the load cases in detail.
Outside aircraft, this aluminum metal appears in automotive hardware such as motorsport and truck wheels, defense components and high-strength fasteners. Our aerospace manufacturing page lists the part types we produce for the sector.
Every aerospace manufacturer buying flight hardware asks for material traceability, mill certificates and first-article inspection. Confirm these with your quality team before the quote, because they affect both price and lead time.
Bare 2024 should not go into service. Sheet is often supplied as Alclad aluminum, with a thin layer of pure aluminum on each face, but a part machined from aluminum plate or bar has no cladding left on its machined surfaces.
The usual protective options are:
| Finish | Fit for 2024 | 说明 |
|---|---|---|
| 铬酸盐转化涂层 | 良好 | Thin, conductive, good paint base; little dimensional change |
| II型阳极氧化 | Acceptable | Color can be uneven because of the copper content |
| Type III hardcoat | Possible with limits | MIL-PRF-8625 allows a looser wear limit for alloys with 2% or more copper |
| Primer and paint | 良好 | Standard on aircraft structure, often over conversion coating |
A 铬酸盐转化涂层 is often the most practical choice for machined 2024 parts that need electrical conductivity or a paint base.
There is a trade-off worth knowing. Anodic coatings reduce fatigue strength, and thicker coatings reduce it more. On fatigue-critical parts, the finish should be chosen together with the fatigue analysis, not added at the end. On aluminum this effect is well documented, so the finish belongs in the design review. Also remember that anodizing grows into the part, so mask or adjust tight bores and fits where tight tolerances matter.
2024 is often specified because "aircraft use it", even on parts that gain nothing from its fatigue behavior. In those cases it costs more and needs more protection than the alternatives. As an aluminum grade, 2024 is a specialist, not a general-purpose choice.
A good rule: choose 2024 when a part sees repeated tension and damage tolerance matters. Otherwise, start with 6061. Our aluminum CNC machining page compares the ten alloys we stock, and explains where 2024 wins and loses against each of them. For most general engineering applications, one of those ten will be the right choice for CNC work.
Most quoting delays on 2024 parts come from missing information. A complete request includes:
A fatigue-critical drawing with no surface finish note on the loaded radii is one of the most common gaps we see. Without it, the machinist treats those surfaces as general, and the part's fatigue life depends on whichever tool happened to cut it. On aluminum, general is rarely good enough for a fatigue part.
Machining 2024 well comes down to three decisions made before any metal is cut: stress-relieved aluminum stock, a finish plan that respects the alloy’s corrosion resistance limits, and surface quality where the part carries cyclic load. Get those right and this aluminum is a predictable, well-behaved metal to machine. It is also why CNC aluminum specialists treat 2024 as a first-choice airframe material rather than a commodity plate.
在 拓维精密, our precision CNC engineers review alloy, temper and finish as part of free DFM feedback, and every critical dimension can be checked on a CMM before shipment. Send your drawing and load case through our 数控加工服务 page, and we will confirm the machining plan before quoting.
Q: Is 2024 aluminum easy to machine?
A: Yes, in heat-treated tempers such as T3, T351 and T851. It shears cleanly, holds tolerance and takes a good finish with sharp carbide tools on any modern CNC machine. The annealed O temper is gummy and difficult. The main challenges are stringy chips, burrs and distortion, not cutting difficulty. For a hard aluminum grade, it is remarkably cooperative.
Q: Why is 2024 aluminum used in aircraft?
A: The 2024 aluminum alloy grows fatigue cracks slowly. NASA testing found 2024-T3 needed two to four times as many load cycles as 7075-T6 for a crack to reach the same length. That damage tolerance suits fuselage skins, lower wing skins and tension-loaded fittings that are inspected in service. It is the reason aluminum airframes from the 1940s still fly today.
Q: Can 2024 aluminum be welded?
A: Not by conventional fusion methods. 2024 tends to crack and lose much of its strength in the joint, so aircraft structure in this alloy is joined with rivets and bolts. Friction stir welding can work but needs qualification. For joined parts, 6061 is usually the better choice.
Q: Does this alloy need a protective coating?
A: Yes. Its copper content makes bare 2024 corrode more readily than most other aluminum alloys. Machined parts have no Alclad layer on cut surfaces, so they need chromate conversion coating, anodizing or primer. Choose the finish early, because some coatings reduce fatigue strength.
Q: What is the difference between 2024-T3 and 2024-T351?
A: Both are solution heat treated and naturally aged. T351 is also stretched to relieve internal stress, so plate and bar in T351 move far less when material is removed from one side. For machined aluminum parts with pockets or thin walls, T351 is the better starting stock.