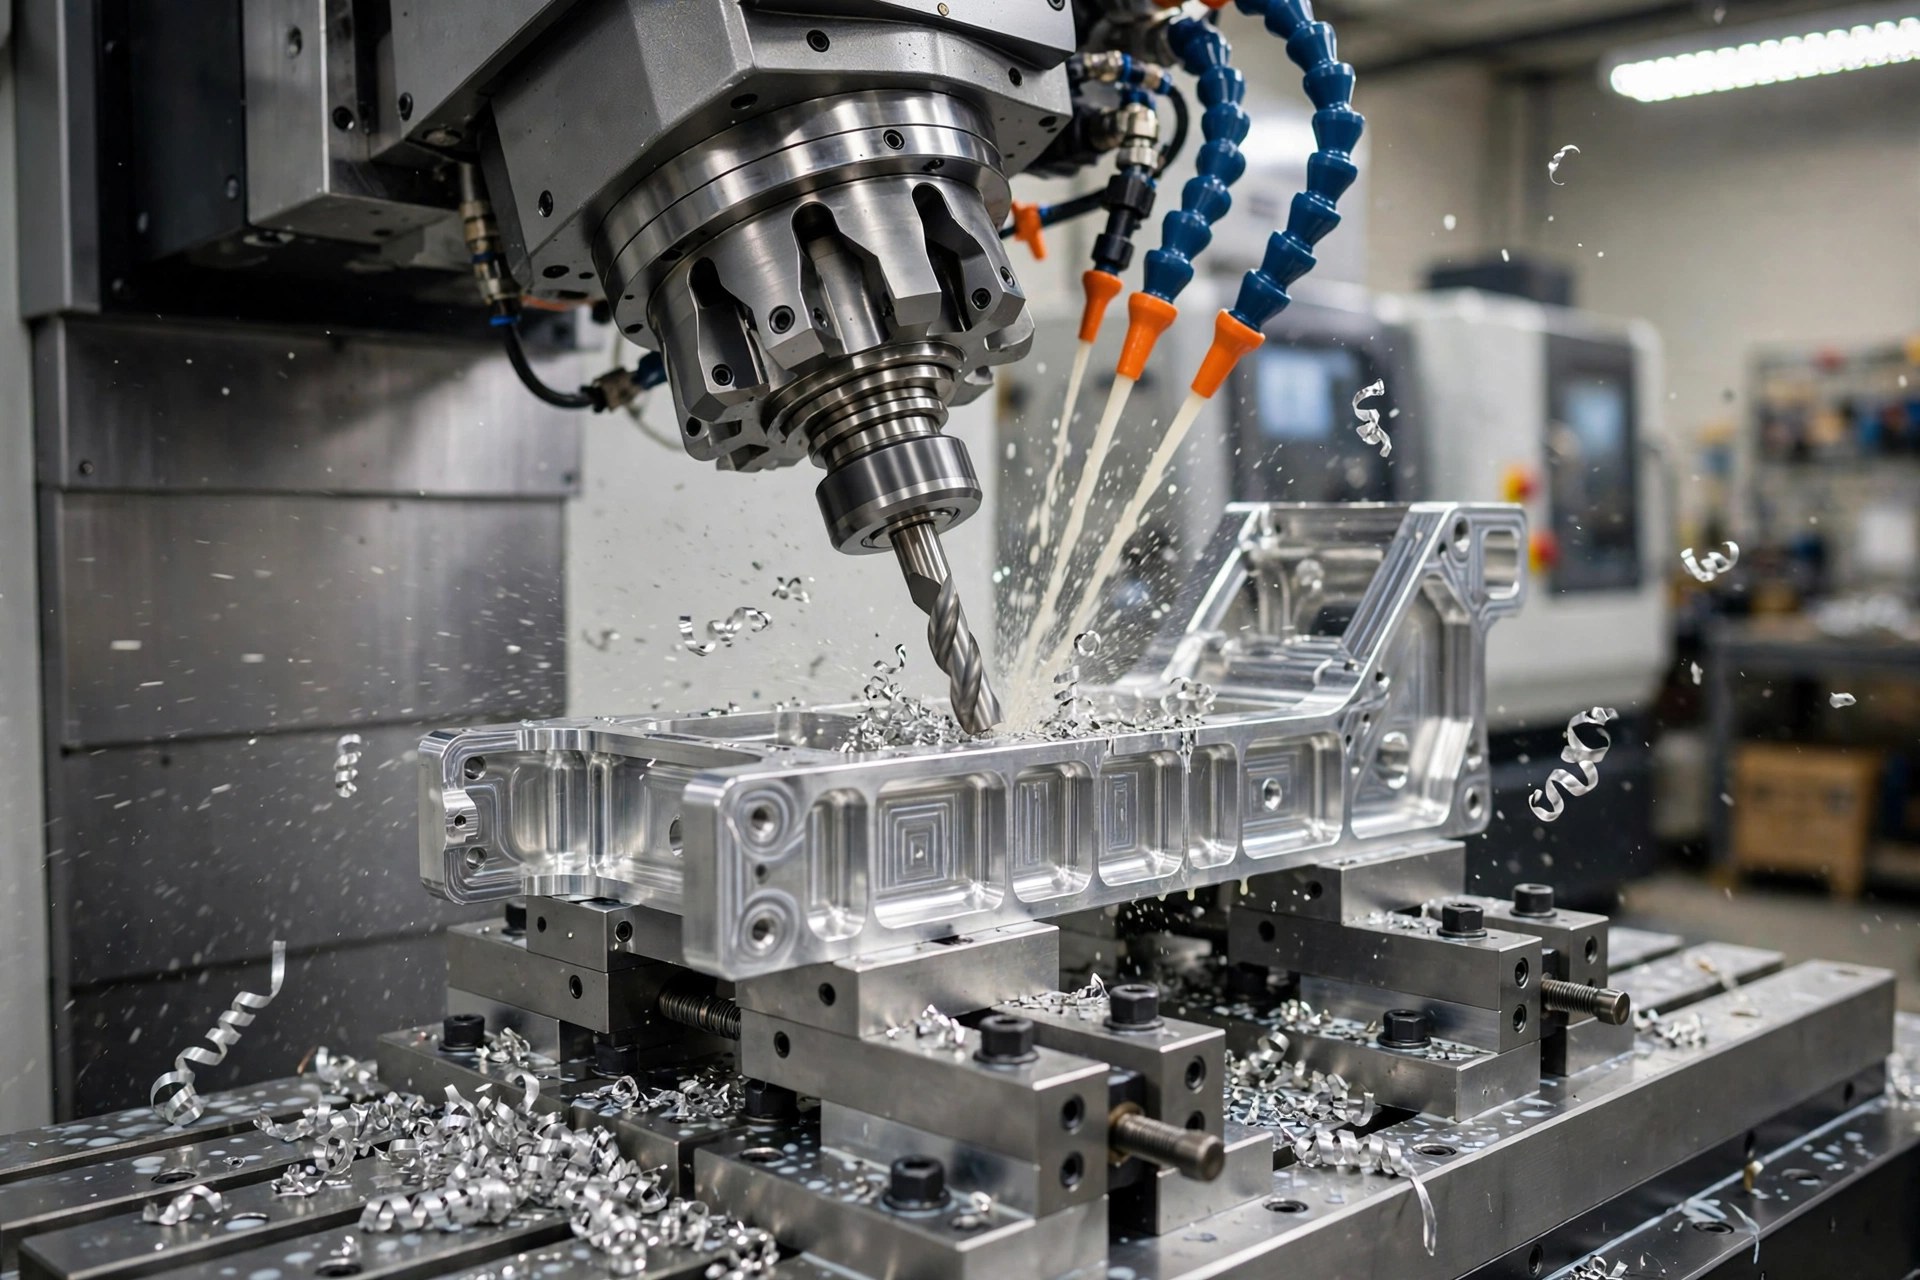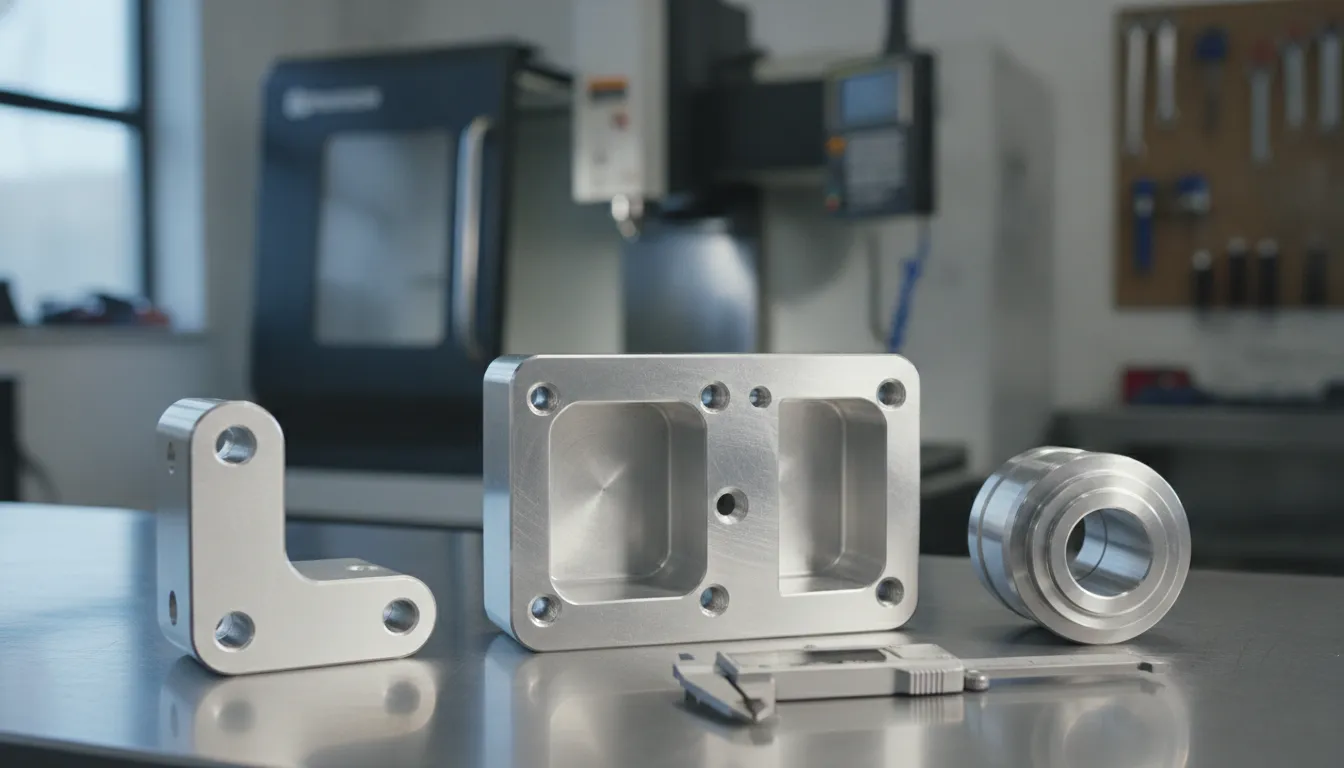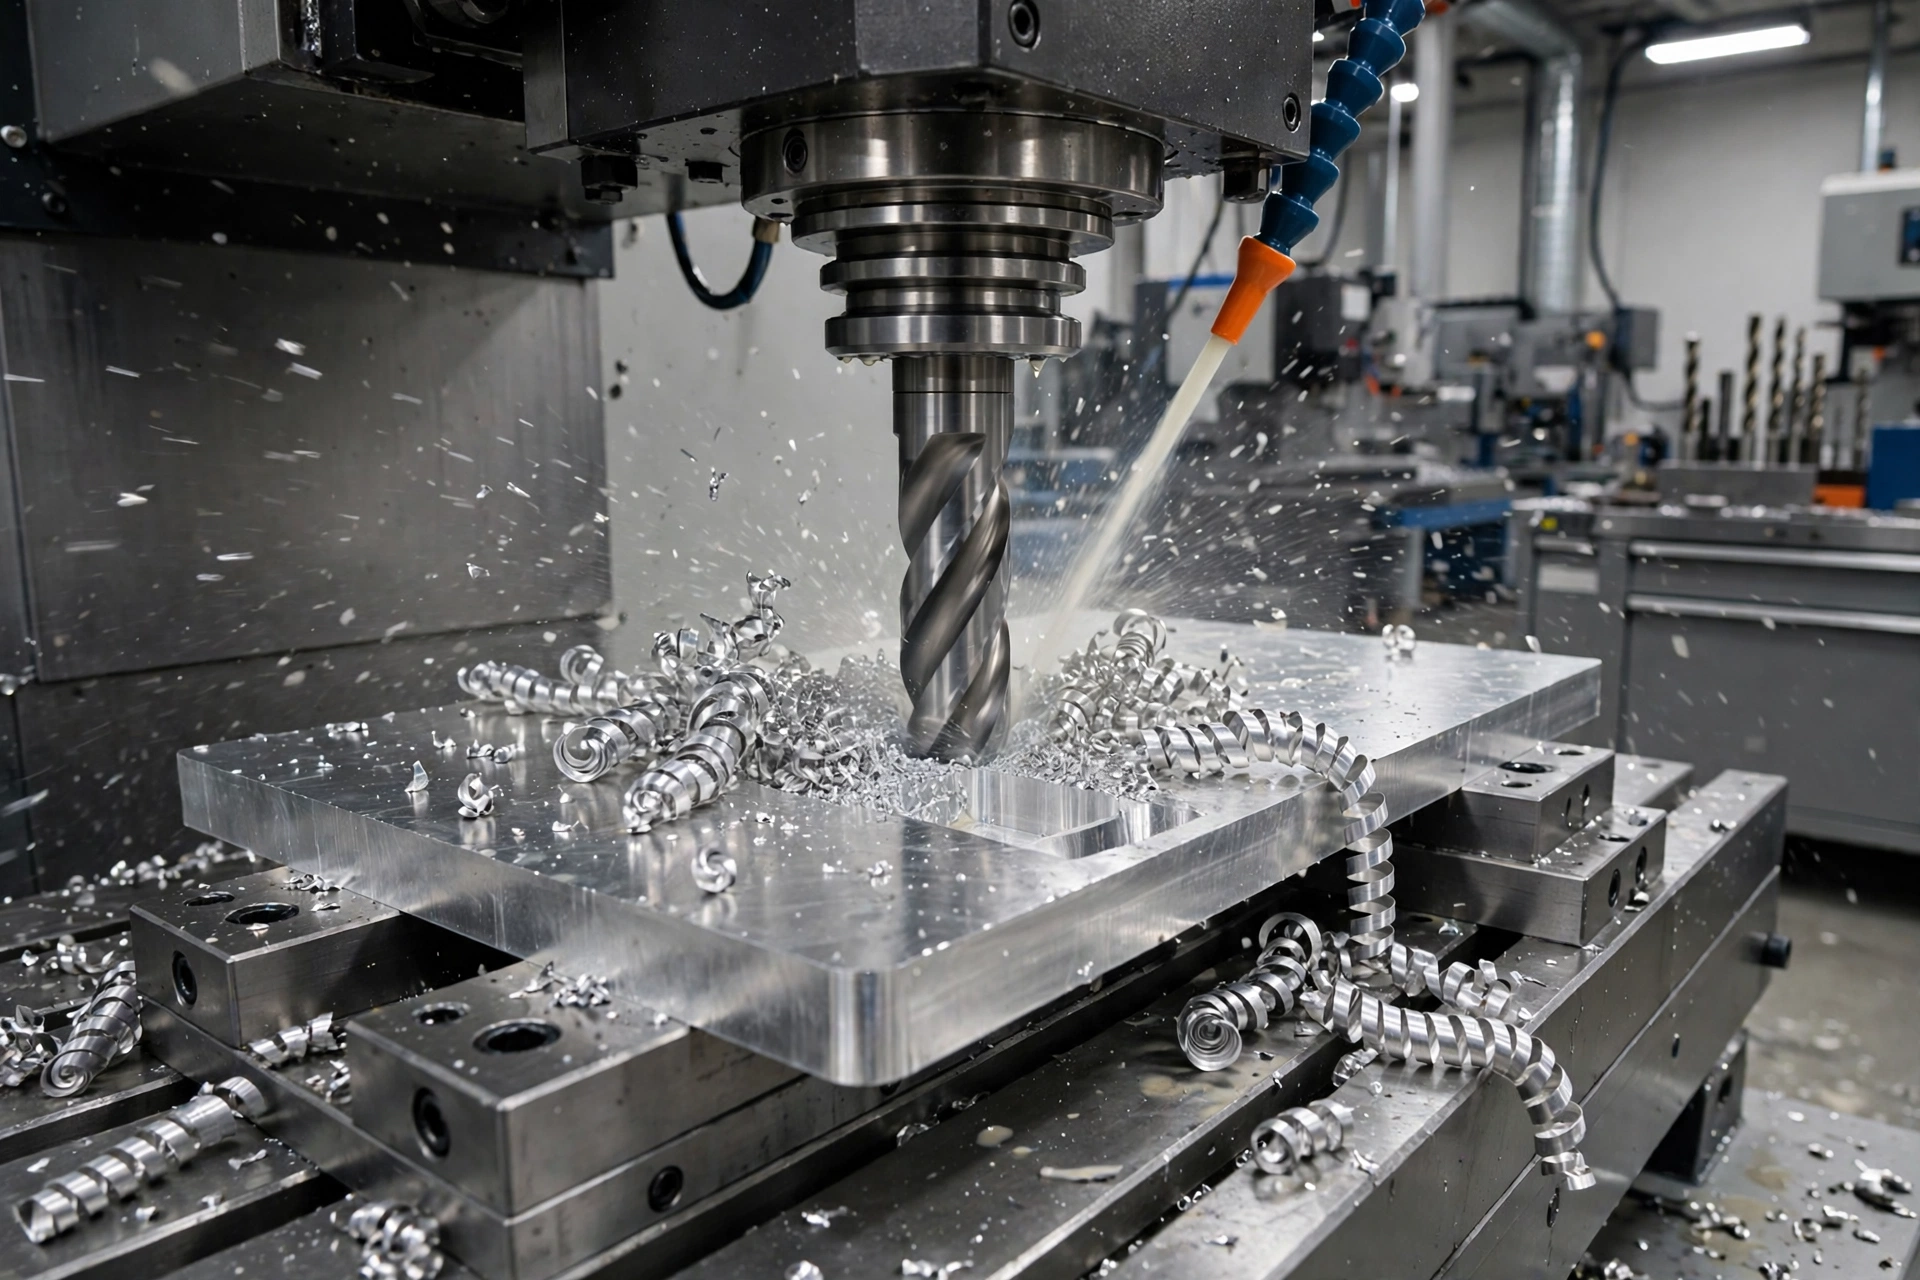
6061 aluminum is the most widely machined aluminum alloy in custom CNC work. It combines medium strength, good corrosion resistance, and easy cutting in one affordable grade. This guide covers its properties, tempers, speeds and feeds, tolerances, and finishes, so you can specify 6061-T6 parts with confidence. This is the practical side of machining 6061 aluminum, from stock selection to finished part.
Most shops reach for 6061 first when a part needs real strength without the cost or cutting difficulty of harder alloys. It welds well, takes anodizing beautifully, and holds up outdoors and in marine air. The sections below give you verified data tables first, then practical guidance for tooling, tolerances, and finishes.
6061 is a precipitation-hardened aluminum alloy whose main alloying elements are magnesium and silicon. During heat treatment these two elements form magnesium silicide, which gives the alloy its strength. Small amounts of copper, manganese, iron, zinc, and titanium complete the recipe, and the balance is aluminum.
Because it is heat-treatable, 6061 can be supplied soft for forming or hardened for structural parts. The T6 temper is the standard choice for machined parts, while T651 adds stress relief for flatter, more stable plates. Both tempers share the same minimum strength, which we compare in the temper table below. Its unified numbering system designation is UNS A96061. Single figures in the composition table are specification maximums.
| Element | Amount |
|---|---|
| Magnesium (Mg) | 0.8-1.2% |
| Silicon (Si) | 0.4-0.8% |
| Copper (Cu) | 0.15-0.40% |
| Iron (Fe) | 0.7% |
| Manganese (Mn) | 0.15% |
| Zinc (Zn) | 0.25% |
| Titanium (Ti) | 0.15% |
| Aluminum (Al) | Remainder |
In the T6 temper, 6061 offers a minimum tensile strength of 290 MPa (42.1 ksi) and a minimum yield strength of 240 MPa (34.8 ksi). Typical published ranges run slightly wider, at 260 to 310 MPa tensile and 240 to 270 MPa yield, depending on product form and test source. These mechanical properties explain why the properties of aluminum 6061 suit structural work.
Hardness sits around 95 Brinell, and density is 2.70 grams per cubic centimeter, which is why 6061 parts feel light for their size. Stiffness is 68 to 74 GPa, and the alloy is non-magnetic with high corrosion resistance and high weldability, a combination that suits structural and outdoor parts. The strength-to-weight ratio is a key reason 6061 leads material selection for structural parts, and its natural oxide layer supports excellent corrosion resistance.
| プロパティ | 価値 |
|---|---|
| 極限引張強さ | Temper minimum 290 MPa (42.1 ksi); published product range 260-310 MPa |
| 降伏強度 | Temper minimum 240 MPa (34.8 ksi); published product range 240-270 MPa |
| 破断伸度 | 8-11% typical; 10% temper minimum |
| 硬度 | 95 HB |
| 密度 | 2.70 g/cm3 (0.0975 lb/in3) |
| ヤング率 | 68-74 GPa (9.9-10.7 Mpsi) |
| 熱伝導率 | 152-169 W/m-C |
| 最高使用温度 | 130-150 C |
| 耐食性 | 高い |
| 溶接性 | 高い |
| 磁気 | 非磁性 |
Temper matters more than most buyers expect, because the same alloy can be soft and formable or hard and structural. Annealed 6061-O is the softest form and suits bending and forming, while T4 offers a middle step of strength after solution treatment and artificial aging.
For machined parts, T6 is the default, and T651 matches its strength while adding a stretching step that relieves internal stress. That stress relief gives T651 better flatness and dimensional stability, so it is the better pick for precision plates and parts with tight flatness needs.
| Temper | Treatment | 引張強度 | 降伏強度 |
|---|---|---|---|
| 6061-O | Annealed | 150 MPa max (21.8 ksi) | 82 MPa max (11.9 ksi) |
| 6061-T4 | Solution treated and artificially aged | 210 MPa min (30.5 ksi) | 110 MPa min (16.0 ksi) |
| 6061-T6 | Solution treated and artificially aged | 290 MPa min (42.1 ksi) | 240 MPa min (34.8 ksi) |
| 6061-T651 | Solution treated, stress relieved by stretching, artificially aged | 290 MPa min (42.1 ksi) | 240 MPa min (34.8 ksi) |
6061 cuts freely, and the practical limit is often the spindle speed or the setup rather than the material itself. Published carbide milling speeds run from 650 to 2,000 SFM in general guidance, while Machining Doctor‘s refined milling recommendation under ideal conditions reaches 2,100 to 2,840 SFM.
Start near the middle of the range for a new job, then adjust for tool diameter, machine rigidity, and chip evacuation. Small tools on a fast spindle can run near the top of the range, while long overhangs, weak clamping, or poor chip clearing call for slower, steadier cutting.
| Operation | Uncoated carbide (SFM) | DLC (SFM) | PCD (SFM) |
|---|---|---|---|
| Turning | 1000-3300 | 1000-6000 | 2000-8000 |
| Milling | 650-2000 | 650-3500 | 1000-6500 |
| Operation | Recommended SFM |
|---|---|
| Turning | 1670-2260 |
| Milling | 2100-2840 |
| Drilling | 710-950 |
| Grooving | 1390-1890 |
| Parting | 1120-1510 |
Uncoated carbide is the right default for 6061 in most shops, because it stays sharp and costs far less than diamond tooling. When output volume is high and the machine can use the speed, DLC-coated carbide adds slickness and wear life, while PCD is the premium choice for very long runs and fine finishes.
Tool shape matters as much as tool material. Use sharp, polished edges with a high rake angle and no edge honing, pick 2 or 3 flutes so chips have room to leave, and choose a helix angle between 35 and 45 degrees for smooth cutting. Our machining services page lists the equipment and materials we run for jobs like these.
Tight tolerances are achievable in 6061, but temper choice and part shape decide how easily they hold. T651 plate starts flatter and moves less after cutting, so it is the safer choice when flatness or close fits matter across a wide part.
Thin walls and deep pockets need care, because cutting forces can flex the wall and leave taper or chatter. Support the wall, take lighter finish passes with a sharp tool, and avoid clamping that bows the part before cutting starts. Our tolerances guide explains what is realistic for aluminum parts in more detail.
6061 takes finishes well, and the right choice depends on whether the part needs color, wear resistance, corrosion protection, or a plain machined look. Anodizing is the most popular route, bead blasting gives a soft matte texture, and chromate conversion protects without changing dimensions much.
Type II anodizing suits decorative color and general protection, while Type III hardcoat anodizing is the pick for wear resistance on sliding or handled surfaces. If a part must stay electrically conductive or needs a paint base, chromate conversion is often the better answer, and our finishes guide compares these options side by side.
| 終了 | What it gives | こんな方に最適 |
|---|---|---|
| II型陽極酸化処理 | Decorative color and general protection | Consumer parts, housings, brackets |
| Type III hardcoat anodizing | Thicker, wear-resistant layer | Sliding parts, handled parts, hard-use parts |
| ビーズブラスト | Uniform matte texture | Cosmetic parts, hiding machining marks |
| Chromate conversion | Corrosion protection with little size change | Electrical parts, paint base, conductive needs |
| 機械加工済み | Clean metal surface, lowest cost | Internal parts, prototypes, hidden parts |
Buyers often narrow the choice to a few familiar alloys, and each one trades strength, corrosion resistance, and weldability differently. 7075 is stronger than 6061 but harder to weld and less forgiving outdoors, so it fits highly loaded aircraft parts better than general brackets and housings.
5052 resists corrosion and forms well but gives up strength, which suits marine panels and bent sheet more than machined blocks. 2024 offers high strength yet poor corrosion resistance and welding, so 6061 remains the balanced middle ground for most machined parts. Our comparison posts cover 6061 against 7075 そして 5052 in full. 7075 aluminum for CNC machining suits high-stress parts where strength justifies the higher cost.
| 合金 | 強さ | 耐食性 | 溶接性 | こんな方に最適 |
|---|---|---|---|---|
| 6061 | ミディアム | 高い | 高い | General machined parts, structures, marine |
| 7075 | 高い | 下へ | 下へ | Highly loaded aircraft parts |
| 5052 | 下へ | 非常に高い | 高い | Marine panels, bent sheet, tanks |
| 2024 | 高い | 低い | 低い | High-strength aircraft structures |
6061 is stocked in more sizes and forms than almost any other aluminum alloy, which keeps lead times short and prices competitive. T6 is usually the cheapest and most available temper, which is one more reason it is the default for machined parts.
That availability also simplifies inventory, since one grade can serve brackets, housings, fixtures, and prototypes across many jobs. For a full view of how 6061 fits beside other grades, see the parent guide to aluminum alloys for CNC machining.
Most 6061 parts start as plate, bar, or extrusion and are milled, turned, or drilled on CNC equipment. Milling shapes housings, brackets, and plates, turning makes shafts, fittings, and round parts, and drilling and tapping add holes and threads for assembly.
Because 6061 cuts so easily, shops can often combine roughing and finishing in fewer setups than steel parts need. That speed is part of why 6061 prototypes and small batches stay affordable, and it also means sharp tools and good chip clearing pay off quickly.
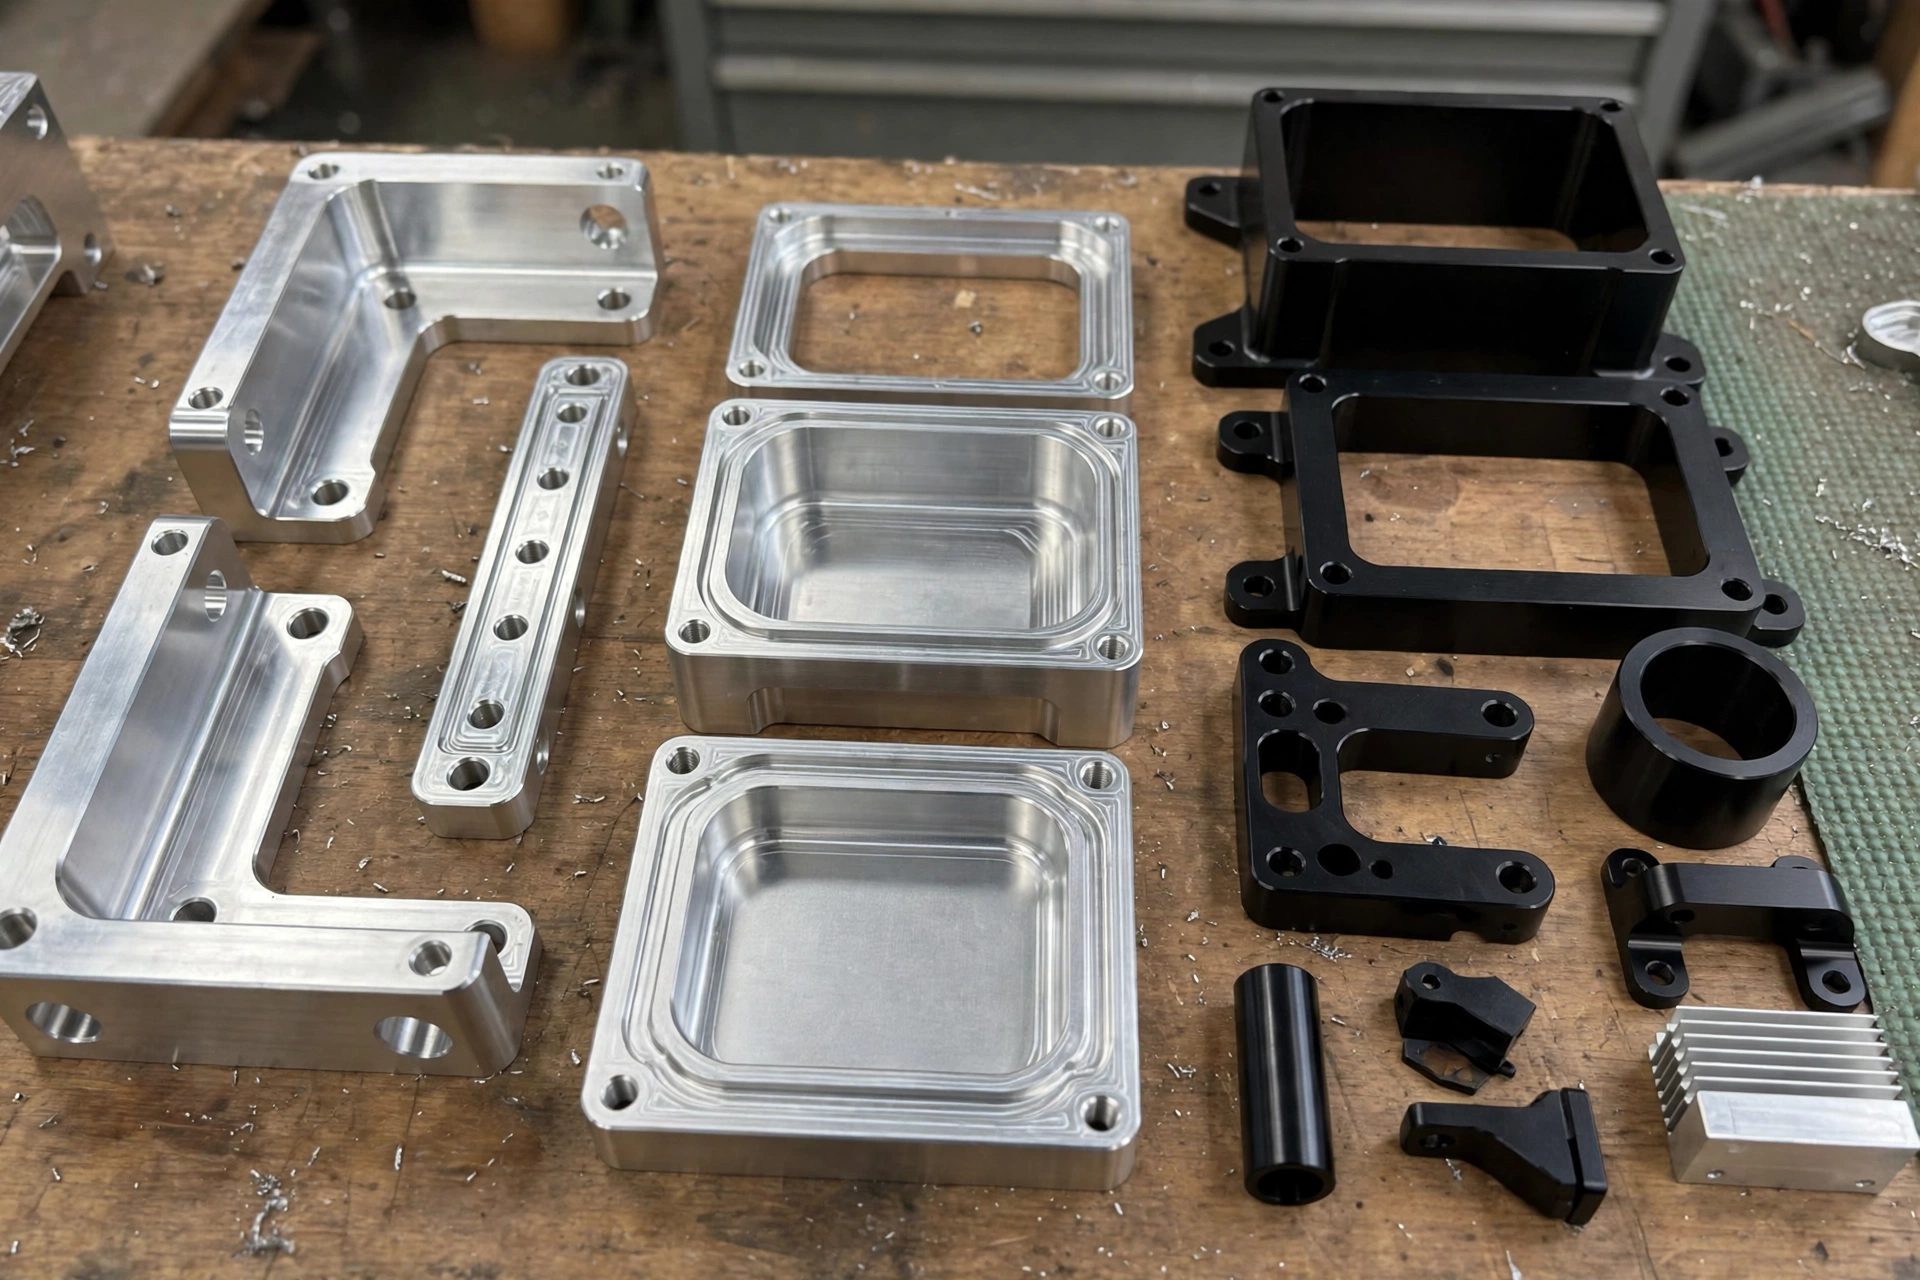
Aircraft structural components and bike frames are classic 6061 jobs, and the alloy also serves automotive parts, marine hardware, electrical fittings, and valves and couplings. Consumer electronics use it for housings and frames where light weight and a clean anodized finish both matter. 6061 is used in aerospace brackets, fittings, and machined housings, and automotive components and aluminum enclosure parts share the same strength and corrosion resistance.
Because it machines fast and finishes well, 6061 is also a strong prototype material when the prototype must behave like the production part. Fixtures, jigs, and tooling plates are another natural fit, since the alloy is stable, easy to cut, and easy to modify.
Drilling 6061 is fast, but the alloy’s softness means drills can grab and holes can drift if the point angle or feed is wrong. Use sharp, polished drills, peck deep holes to clear chips, and keep coolant or air on the cut so chips do not pack and score the hole wall.
Tapping follows the same logic, since torn threads come from dull taps, poor lubrication, or chips clogging the flutes. Form taps work well in 6061 for strong threads without chips, while cut taps need sharp edges and steady lubrication to stay accurate.
Generous fillets at inside corners reduce stress and tool chatter, and they also make the part easier to machine than sharp internal corners. Where a wall must stay thin, add ribs or bosses nearby for support rather than relying on the thin section alone. Keep wall thickness generous on thin features, and check the minimum wall thickness early so the part survives machining and handling.
Remember that anodizing adds a thin layer to every surface, so mating features and tight fits should be designed with that coating in mind. Threads cut cleanly in 6061, but sharp taps, proper lubrication, and chip clearing keep them accurate and free of torn threads. Plan surface treatments for aluminum early, since anodizing and other surface treatments change final dimensions.
Built-up edge is the most common 6061 complaint, and it usually traces back to a dull edge, slow surface speed, or chips packing around the cut. Keep edges sharp and polished, keep chips moving with air or coolant, and avoid letting the tool rub instead of cut.
For appearance work, climb milling with a sharp tool usually leaves a cleaner face than conventional cutting, and a light finish pass removes witness marks. Check the first part under good light before running the batch, since small changes in edge condition show up quickly on 6061 faces.
First-article inspection matters for 6061 because the alloy cuts so easily that small setup changes show up as size drift. Check critical dimensions, hole positions, and flatness on the first part, then recheck at set intervals during longer runs.
Surface finish deserves the same attention, since chip scratches and built-up edge marks are easy to miss under shop lighting. Inspect faces under bright light, deburr every edge, and confirm anodized parts show even color before they ship.
If you have a drawing or a prototype idea, our team can review it and recommend the right temper, finish, and tolerance plan for the job. Send your file through our services hub for a quote, and we will confirm material, lead time, and pricing before cutting starts.
For a deeper look at the full range of aluminum grades, the parent guide compares each alloy side by side, and the complete guide covers the machining process from stock to finished part. If your part needs a dedicated shop, the service page lists materials, finishes, and tolerances in one place.
Material selection starts with the aluminum grade, and the 6061 aluminum alloy is the default for most CNC aluminum work because it balances strength, corrosion resistance, and cost. The aluminum alloy 6061 compares well with 6082 aluminum and 5052 aluminum, or aluminum 5052, where forming matters more than strength. For higher strength, 7075 aluminum beats 6061, and the 6061 vs 7075 aluminum choice comes down to strength needs versus budget and weldability.
Machining costs often decide the grade, so use this guide to CNC material choice before starting a CNC machining project: 6061 is ideal for CNC work when parts need strength, weldability, and a good finish at a moderate price. Aluminum for CNC machining ranges from soft forming grades to high-strength plate, and aluminum machining shops stock 6061 because it is used in CNC machining every day.
High-speed CNC milling suits 6061 well, and face milling with a large cutter clears stock fast while leaving a smooth surface. On the mill, a rigid setup and sharp tools matter more than raw power, and a careful mill setup keeps cycle time low. Stable machining comes from light depths of cut, strong workholding, and steady chip evacuation, which also improves machining behavior across long runs.
6061 machines well on 3-axis CNC equipment, and CNC machined aluminum parts from such setups include brackets, plates, and custom aluminum housings. Mechanical parts and precision parts in 6061 T6 benefit from the alloy’s easy cutting, and CNC-machined aluminum ordered this way keeps machining efficiency high.
No. 6061 is one of the easiest aluminum alloys to machine, and it cuts cleanly at high speeds with carbide tools. The T6 temper machines better than soft tempers, which can smear and build up on the edge. Sharp, polished tools and good chip clearing keep the finish clean.
Machining Doctor lists the machinability of 6061 at 270 percent on its scale, which reflects how freely it cuts compared with harder materials. Rating scales differ between publishers, so the number is best read as a relative guide rather than an absolute score. In practice, 6061 sits at the easy end of aluminum alloys.
For carbide end mills, general guidance runs from 650 to 2,000 SFM, while Machining Doctor’s refined milling recommendation under ideal conditions reaches 2,100 to 2,840 SFM. Turning with carbide runs from 1,000 to 3,300 SFM in general guidance, with a refined range of 1,670 to 2,260 SFM. Start in the middle of the range and adjust for tool size, rigidity, and chip clearing.
Not in the formal sense. Free-machining alloys use additions such as lead or bismuth that break chips into small pieces. 6061 contains no such additions, so it forms continuous chips, but it still machines easily with sharp tools and proper chip evacuation.
Hardened tool steels, titanium alloys, and nickel alloys such as Inconel are among the hardest metals to machine, because they combine high strength with poor heat conduction and rapid tool wear. 6061 aluminum sits at the opposite end, since it cuts at high speeds with modest tool wear. That gap is why 6061 is a popular choice when machining cost matters.
Both tempers share the same minimum strength, so the choice comes down to stability and price. T651 is stress relieved by stretching, which gives better flatness and dimensional stability for precision plates and wide parts. T6 is usually cheaper and easier to source, so it is the default when extreme flatness is not required.