専門的な機械加工ソリューションが必要ですか?私たちTuowei Protoのチームは、あなたのすべての製造のニーズを支援するためにここにいる。現在進行中または今後のプロジェクトのお見積もりについては、今すぐご連絡ください!
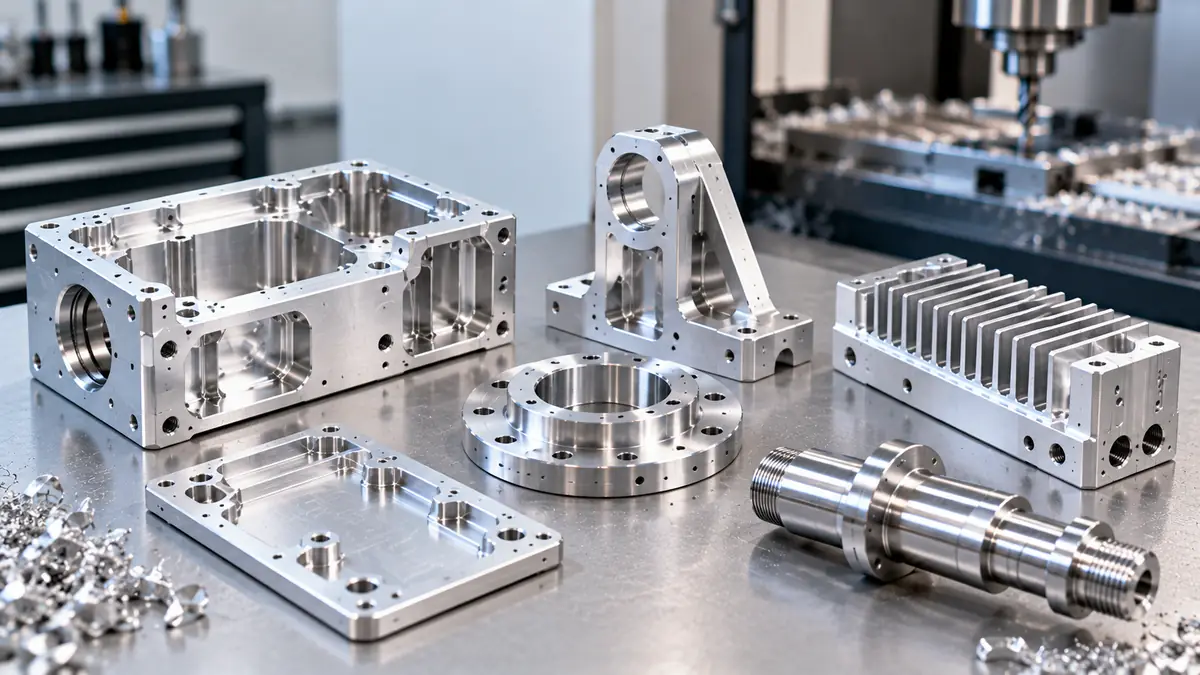
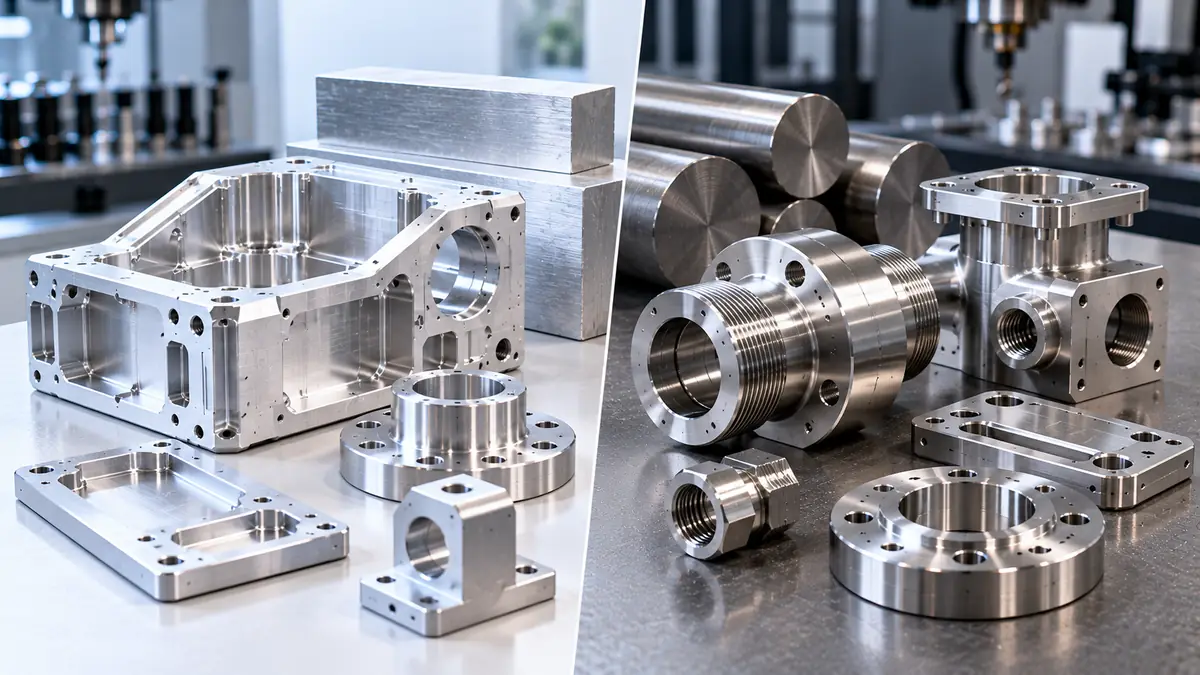
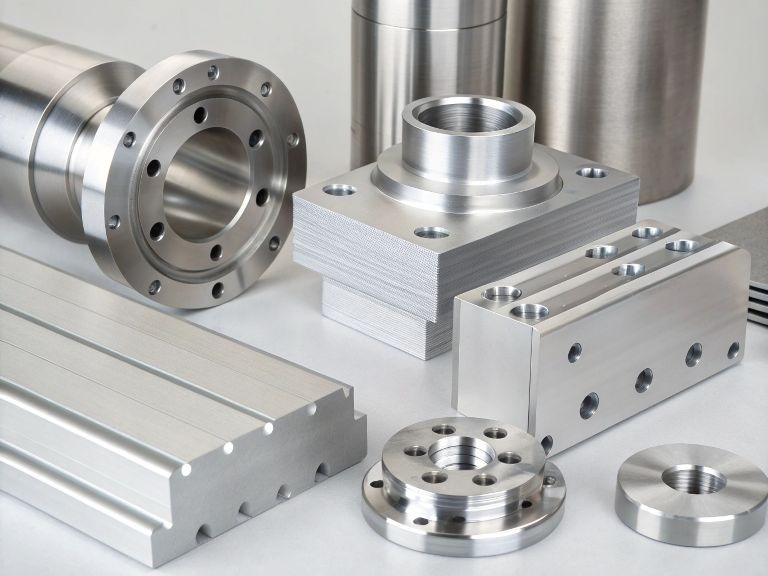
Aluminum CNC machining is the process of cutting custom parts from solid aluminum stock on computer-controlled mills and lathes. It is the most common way to make metal prototypes and production parts because aluminum cuts fast, weighs about a third as much as steel, and takes finishes like anodizing well. Most parts are made from 6061 or 7075.
簡単な答え: For most machined aluminum parts, start with 6061-T651. Design walls of at least 0.8 mm, keep holes no deeper than about four tool diameters, and use a standard tolerance of ±0.005 in unless a feature truly needs tighter. Prototypes typically ship in 1 to 5 business days. Anodizing, tight tolerances, and extra setups are the biggest cost drivers.
Aluminum is the default metal in most machine shops, and machining aluminum is usually faster and cheaper than cutting steel, for a mix of practical reasons.
The trade-offs are real too. Aluminum is soft enough to scratch and dent in handling, it moves more with temperature than steel, and thin sections can distort after heavy material removal. Good shops plan around all three.
For most parts, 6061-T651 is the best starting point. It machines cleanly, anodizes evenly, and costs less than the high-strength grades. Move to another alloy only when the part needs something 6061 cannot give.
によると Aluminum Association, the first digit of the alloy number tells you the main alloying element: copper for 2xxx, magnesium for 5xxx, magnesium and silicon for 6xxx, and zinc for 7xxx.
| 合金および焼き戻し | Pick it when | Watch out for |
| 6061-T651 | General housings, brackets, fixtures, enclosures | Moderate strength only |
| 7075-T651 | High loads, aerospace-style structures, tooling | Higher cost, poor weldability, less even cosmetic anodizing |
| 2024-T351 | 疲労荷重を受ける部品 | Poor corrosion resistance without a coating |
| 5052 | Corrosion-exposed covers and formed parts | Gummy to machine, better suited to sheet |
| 6082 | European drawings that call out EN AW-6082 | 米国の供給市場ではあまり見られない |
| MIC6 鋳造プレート | Flat plates, fixture bases, vacuum plates | Lower strength |
The temper matters as much as the alloy. T651 means the plate was stretched to relieve internal stress, so it stays flatter after machining than plain T6.
Three processes cover almost every job in CNC machining of aluminum.
CNCフライス加工 removes material with a rotating cutter while the part is held still. It makes pockets, faces, slots, and complex 3D surfaces. Housings, brackets, and plates are milled. Tuowei’s CNC milling service runs 3-axis, 4-axis, 5-axis, and right-angle heads.
CNC旋盤加工 spins the part against a stationary tool. It makes round features such as shafts, bushings, knobs, and threaded fittings. Parts with both round and flat features are often turned first, then milled. See CNC旋盤加工 for typical turned parts.
5軸加工 tilts and rotates the part or spindle so the tool reaches several faces in one setup. It costs more per hour, but fewer setups can lower the total price on complex parts and improve feature-to-feature accuracy. Parts with angled holes or sculpted surfaces are usually quoted on 5軸CNC加工.
Drilling, tapping, reaming, and boring happen on the same machines as secondary operations.
The main challenge in aluminum machining is not hardness. It is stickiness. Soft aluminum wants to weld itself to the cutting tool, which is called built-up edge. Everything in a good aluminum setup is aimed at preventing it.
One safety point: fine aluminum dust can be explosive. OSHA’s combustible dust guidance lists aluminum among the metals that can be explosible in dust form, so shops that grind, sand, or polish aluminum need proper dust collection.
Design for manufacturing (DFM) means shaping a part so it is easy to machine without hurting its function. These guidelines for machining aluminum come from Tuowei’s published milling capabilities.
| 特徴 | ガイドライン |
| 肉厚 | 0.8 mm minimum for metals; thicker walls machine faster and chatter less |
| Hole depth | No more than about 4 times the tool diameter for standard drilling |
| Thread depth | 2 to 5 times the thread diameter |
| Internal corners | Use the largest radius the design allows; sharp inside corners are impossible with a round cutter |
| Engraved text | 0.5 mm minimum stroke width |
A few more habits that save money:
Tuowei publishes these tolerance ranges for CNC milled parts:
| 申し込み | 寛容 |
| Standard machining | ±0.005インチ(±0.127 mm) |
| High precision | ±0.001インチ(±0.025 mm) |
| Small components | ±0.002インチ(±0.051 mm) |
| Large components | ±0.010インチ(±0.254 mm) |
| Threaded features | ±0.005インチ(±0.127 mm) |
Tighter machining tolerances are possible, but each step down adds machine time and inspection. Put tight tolerances only on features that mate or seal.
For dimensions without a specific tolerance, many drawings reference ISO 2768-1, which sets general tolerances in classes such as fine (f) and medium (m). A note like “ISO 2768-m” tells the shop what to hold everywhere else. ISO has signaled a revision of this standard is coming, so check which edition your customer requires.
Most machined aluminum parts get at least one finish after machining.
The most common problem with anodized aluminum parts is dimensional change. The coating grows partly outward from the surface, so tight bores, press fits, and threads can end up undersize. Mask those features, or state on the drawing whether dimensions apply before or after anodizing. Tuowei’s アルミニウム陽極酸化サービス page lists the available options.
Material is rarely the largest cost in CNC machining aluminum. Machine time and setups are. The main drivers, roughly in order of impact:
Our position: the cheapest change on most drawings is loosening tolerances that do not matter. It often saves more than switching alloy or supplier.
Tuowei’s published lead times for CNC milled parts are:
| Order size | リードタイム |
| Prototypes, 1 to 100 pieces | 1 to 5 business days |
| Low volume, 101 to 10,000 pieces | 5 to 15 business days |
| 大量生産 | 2 to 4 weeks |
Those windows cover machining. Anodizing, special inspection, and shipping add time on top. A typical first order moves through five stages: quote and DFM review, programming and fixturing, a first article for approval, the production run, and finishing and inspection. Answering DFM questions quickly is the easiest way to keep a project on schedule.
Inspection is where a good supplier proves that CNC machined aluminum matches the drawing. For a new part, expect:
Ask to see a sample inspection report before you order. Tuowei describes its process on the 品質保証 page.
| Problem | Likely cause | Fix |
| Material sticking to the tool | Rubbing, dull tool, poor chip clearance | Sharp polished carbide, higher feed, better coolant |
| Chatter marks | Long tool, thin wall, weak fixturing | Shorter tool, thicker walls, rigid support |
| Part warps after machining | Internal stress in the stock | Use T651 plate, balance material removal on both sides |
| Heavy burrs | Soft alloy or worn tool | Fresh tools, planned deburring, edge break note |
| Anodized parts do not fit | Coating growth on tight features | Masking or pre-anodize allowances |
Machined aluminum shows up across almost every industry that builds hardware.
A complete request gets a faster, more accurate quote for custom aluminum parts. Include:
Shops that offer design for manufacturing review will flag risky features at this stage, before any metal is cut.
6061-T651 is the best all-round choice. It machines cleanly, anodizes evenly, resists corrosion, and costs less than high-strength grades. Choose 7075-T651 when the part carries high loads, 2024 for fatigue-loaded parts, and MIC6 cast plate when flatness matters most, such as fixture bases and vacuum plates.
Yes. Aluminum is one of the easiest metals to machine because it is soft and allows high cutting speeds. The main challenge is material sticking to the tool. Sharp carbide tools with two or three polished flutes, a proper chip load, and good chip evacuation prevent most problems.
A standard tolerance of ±0.005 in (±0.127 mm) is typical, and high-precision features can reach ±0.001 in (±0.025 mm). Tighter tolerances cost more because they need slower cutting and more inspection. Reserve them for mating, sealing, or bearing features and use a general tolerance elsewhere.
A practical minimum is about 0.8 mm for metal walls. Thinner walls are possible on small features but tend to vibrate, deflect, and warp during cutting. Thicker walls machine faster and hold tolerance better, so use the thickest wall your design allows, especially on tall features.
Coolant is strongly recommended. Flood coolant, mist, or a strong air blast keeps chips from sticking to the tool and being recut, which protects surface finish and tool life. Some light cuts can run with air alone, but production machining of aluminum almost always uses coolant or mist.
Good aluminum CNC machining comes down to a few choices made early: the right alloy and temper, a design that suits the cutter, tolerances only where they matter, and a finish that is planned into the dimensions.
Tuowei Precision machines custom aluminum parts from prototype to production in its Shenzhen factory, with DFM feedback before cutting starts. Send your drawing through the Tuowei Precisionのホームページ, or review the 6061-T651 aluminum data sheet to confirm it fits your part.
執筆:TUOWEI Precisionの製造エンジニア、アンディ。. アンディは、CNC加工、精密製造、生産工学を専門としており、ラピッドプロトタイピングから本格生産に至るまでのプロジェクト支援において、実務経験を有しています。彼は、エンジニアリングチームや製造チームと緊密に連携し、材料、公差、加工プロセス、および設計の製造適性を評価しています。 彼の記事は、実用的かつ技術的な知見に裏打ちされた洞察を提供し、エンジニアや購買担当者がより適切な製造上の意思決定を行い、生産効率を最適化し、一貫した部品品質を実現できるよう支援しています。次回のプロジェクトには、TUOWEI PrecisionのCNC加工およびカスタム製造ソリューションをご検討ください。.
ラピッドプロトタイピングから量産に至るまで、Tuowei Precisionは、あらゆる工程において精度と一貫性を兼ね備えた信頼性の高いCNC加工を提供します。今すぐプロジェクトを始めましょう。.
Tuowei精密の実際のCNC加工、業界動向、生産洞察力を常に更新しますが、より良い生産の意思決定を行うことができるようにインストールされています。.