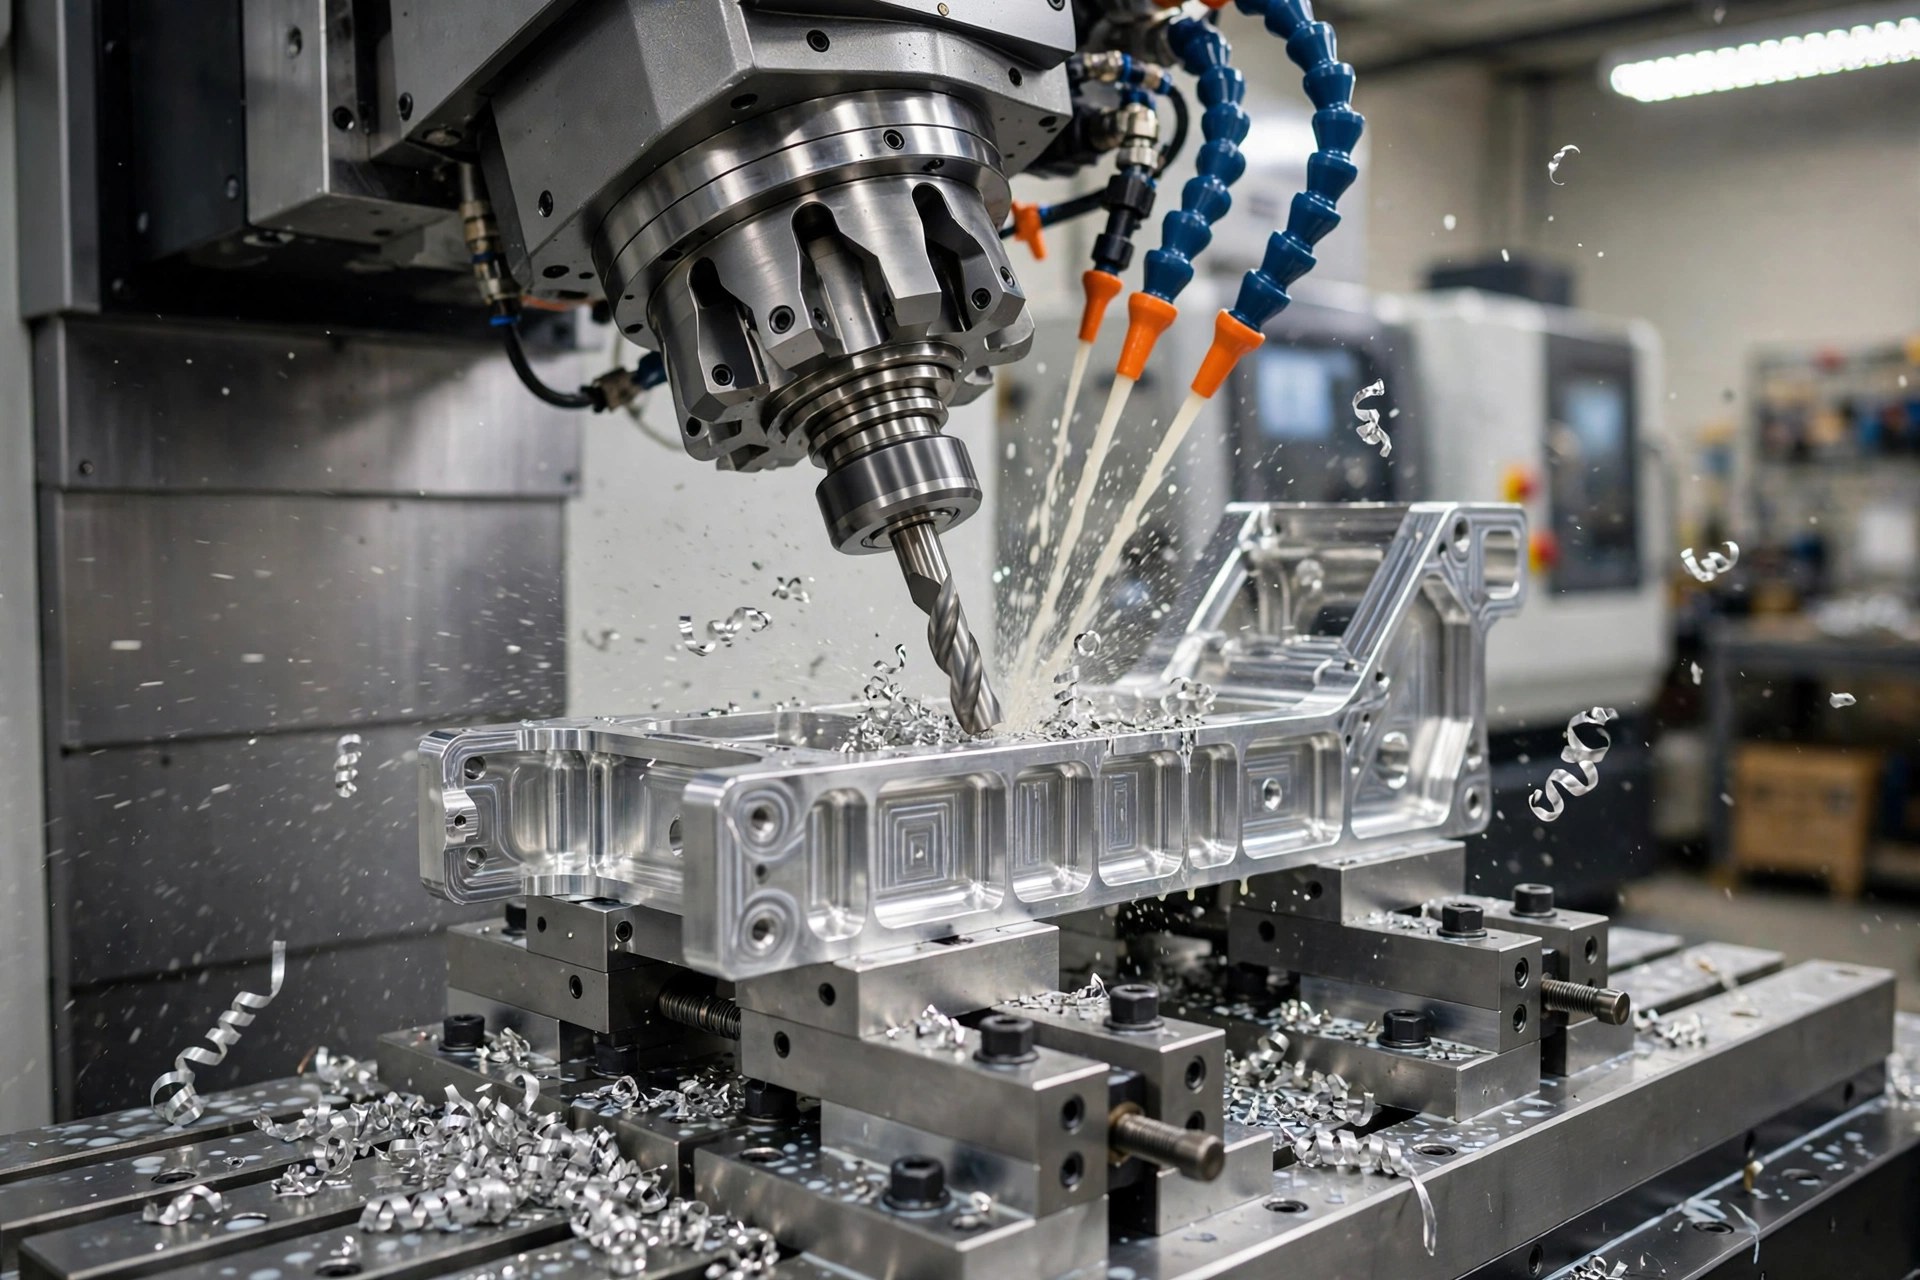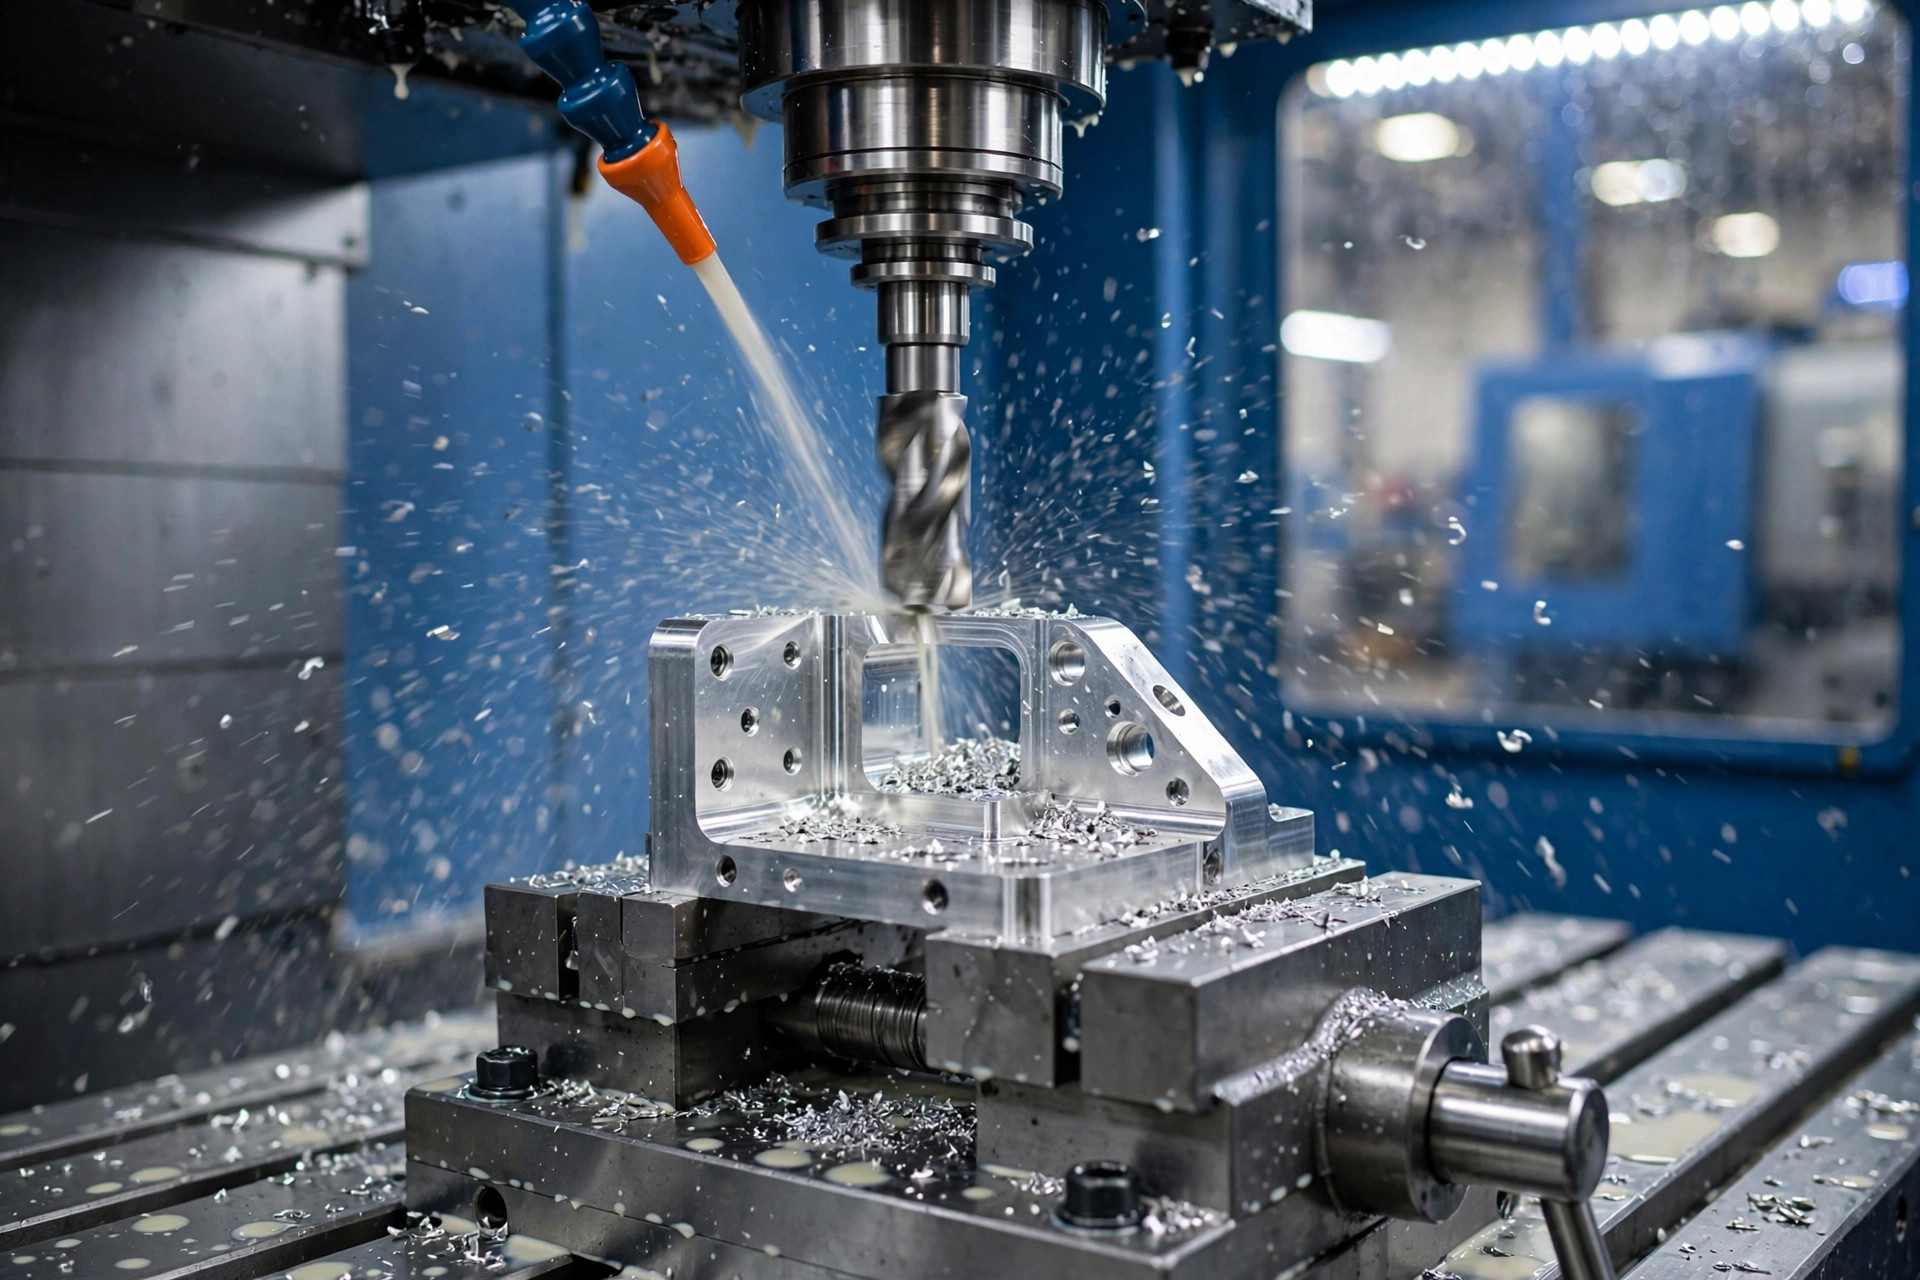
Machining 7075 aluminum is where aluminum stops behaving like a “soft, easy” metal. 7075 is the strongest of the common aluminum alloys — in the T6 temper, 7075-T6 aluminum reaches a tensile strength of 83,000 psi (572 MPa), close to some steels at roughly one-third of the weight. That strength is exactly why aircraft builders, defense contractors and high-performance brands specify it, and it is also why machining 7075 aluminum demands more discipline than machining a forgiving alloy: sharper tooling, controlled cutting parameters, and a plan for the residual stress locked inside the material.
This guide covers the complete machining process for 7075 aluminum on computer numerical control (CNC) equipment — the tooling that works, realistic speeds and feeds, how to choose between T6 and T7351 tempers, and how to keep precision parts from warping after they leave the machine. If you are still deciding which alloy your part needs, start with our grade-by-grade guide to the best aluminum alloy for CNC machining, then come back here for the machining detail.
Aluminum alloy 7075 belongs to the 7000 series, where zinc is the primary alloying element (5.1–6.1%), supported by magnesium (2.1–2.9%) and copper (1.2–2.0%). Developed in the 1930s for airframe structures, it is a heat-treatable alloy that gains its strength from precipitation hardening: solution heat treatment followed by artificial aging. The result is an aluminum alloy with an outstanding strength-to-weight ratio — a specific strength few lightweight materials can match — plus good fatigue resistance and a density of just 0.102 lb/in³ (2.81 g/cm³). It is supplied as plate, bar, sheet and extrusion, and almost every precision part starts from one of those forms.
Three properties of the 7075 aluminum alloy matter most at the machine:
The full registered chemical composition explains both the strength and the machining behavior — including the small chromium addition (0.18–0.28%) that controls grain structure and helps resist stress corrosion cracking:
| Element | Content |
|---|---|
| Zinc (Zn) | 5.1–6.1% |
| Magnesium (Mg) | 2.1–2.9% |
| Copper (Cu) | 1.2–2.0% |
| Chromium (Cr) | 0.18–0.28% |
| Iron (Fe) | 0.50% max |
| Silicon (Si) | 0.40% max |
| Manganese (Mn) | 0.30% max |
| Titanium (Ti) | 0.20% max |
| Aluminum (Al) | Balance |
The alloy is designated UNS A97075 in North America, EN AW-7075 in Europe and AlZnMgCu1.5 (material number 3.4365) in the DIN system.
The temper you buy decides half of the machining story before the spindle starts:
| Tempérament | État | Résistance à la traction | Limite d'élasticité | Allongement | Typical choice for |
|---|---|---|---|---|---|
| 7075-T6 / T651 | Peak aged; T651 is stress-relieved by stretching | 83,000 psi (572 MPa) | 73,000 psi (503 MPa) | 11% | Maximum strength; T651 plate for precision parts |
| 7075-T73 / T7351 | Overaged for stress corrosion resistance; T7351 is stress-relieved | 73,000 psi (505 MPa) | 63,000 psi (435 MPa) | 13% | Thick, highly machined parts exposed to weather or marine air |
| 7075-O | Annealed | 33,000 psi (228 MPa) | 15,000 psi (103 MPa) | 16% | Forming first, then heat treating to a stronger temper |
Other mechanical properties and reference values for 7075-T6: Young’s modulus ≈ 10,400 ksi (71.7 GPa), thermal conductivity ≈ 130 W/m·K, electrical conductivity around 40% IACS, and a melting range of roughly 890–1,180 °F (477–635 °C).
No — but it is less forgiving than 6061. The machinability of 7075 aluminum is usually rated at about 70–80% of free-machining brass (or of 2011-T3 aluminum) — good machinability for a high-strength alloy. With sharp tools, chip formation is clean and segmented: it produces short, well-broken chips instead of the long stringy swarf softer alloys make, burr formation is minimal, and it can hold an excellent surface finish.
Where machinists get caught out is treating it exactly like 6061:
In short, aluminum 7075 machining rewards a rigid setup, sharp carbide and steady chip flow — get those three right and the alloy is genuinely pleasant to cut.
Tool selection is the first decision in any 7075 aluminum CNC machining job. Cutting tools for this alloy follow a few simple rules:
Tool wear is the quiet variable in every 7075 job. The alloy’s hardness steadily rounds cutting edges, and a worn tool stops shearing chips and starts plowing — surface finish falls, heat climbs and dimensions drift. Track tool life by parts-per-edge on production work, index or swap tools on a schedule rather than on failure, and listen: an experienced machinist can hear the pitch change that signals a dulling cutter before the finish shows it.
7075 runs at high spindle speeds, slightly below the wildest values used for soft alloys, because edge life and surface finish matter more than raw material removal rate (MRR). Optimizing cutting parameters starts with the surface speed in SFM (surface feet per minute) and the feed rate per tooth. Use the figures below as proven starting points for carbide tooling with flood coolant, then tune to your machine, tool and part geometry.
| Operation | Cutting speed | Feed guidance | Notes |
|---|---|---|---|
| Milling (roughing) | 820–1,150 ft/min (250–350 m/min) | Chip load 0.004–0.010 in/tooth (0.10–0.25 mm) on 3/8–3/4 in cutters | Radial step-over 30–50% of tool diameter; climb milling preferred |
| Milling (finishing) | 1,150–1,800 ft/min (350–550 m/min) | Chip load 0.002–0.005 in/tooth (0.05–0.13 mm) | Light radial depth of cut (2–5% of diameter) for the best surface finish |
| Drilling | 490–820 ft/min (150–250 m/min) | 0.002–0.008 in/rev (0.05–0.20 mm/rev) by drill size | Peck on deep holes; coolant-through drills for production runs |
| Turning | 980–1,650 ft/min (300–500 m/min) | 0.004–0.012 in/rev (0.10–0.30 mm/rev) | Positive-rake polished inserts; continuous cuts avoid dwell marks |
| Parting and grooving | 700–1,180 ft/min (215–360 m/min) | 0.002–0.006 in/rev (0.05–0.15 mm/rev) | Narrow tools need rigid support; keep coolant on the cut to clear chips from the groove |
Three parameter habits protect both tool life and accuracy when machining aluminum 7075:
Distortion is the number-one scrap risk in 7075 aluminum machining, and it has little to do with the cutting itself. Plate and bar leave the mill with residual stress from quenching. Remove material unevenly and the stress balance shifts — the part bows, twists or springs the moment it is unclamped. Thin walls and large pockets machined from thick plate are the worst cases.
A distortion-proof machining sequence looks like this:
These are the same principles we apply to thin-wall aluminum machining generally — with 7075 the penalty for skipping them is simply higher, because the stock stress and the part values are both greater.
The T6 vs T7351 decision trades about 12% of strength for two things precision parts often need more: stability and stress corrosion resistance.
Both tempers start from the same heat treatment — solution treatment near 900 °F (480 °C), a water quench, then artificial aging. T6 stops aging at peak strength; T73 continues into overaging, giving up some strength to stabilize the grain-boundary structure that resists stress corrosion cracking. The temper code on the mill certificate is therefore not paperwork — it is a machining and service-life decision.
Practical rule: if the drawing simply says “7075,” quote and machine T651 for milled plate parts. If the part is a thick aerospace fitting with deep pockets and an outdoor service life, raise T7351 with the customer before cutting — it is cheaper to change temper on paper than to scrap a batch of bowed housings.
7075 rewards good machining with an excellent surface finish — Ra 32 µin (0.8 µm) or better is realistic straight off the tool with the finishing parameters above. From there, the common finishing routes are:
Because bare 7075 has only fair corrosion resistance, a protective finish is not optional for parts that will see humidity, salt air or dissimilar-metal contact.
The shortest honest answer: 6061 is the better default, 7075 is the better specialist. 6061-T6 (45,000 psi / 310 MPa tensile) is cheaper, easier to source, welds well and anodizes beautifully. 7075-T6 is roughly 80% stronger, holds up better under fatigue loading, and machines to a crisper finish with shorter chips — at a higher material price, with no practical weldability and more care needed against corrosion and distortion.
Choose 7075 when the design is genuinely strength- or fatigue-limited: highly loaded fittings, structural aerospace parts, performance components where a thinner, lighter section must carry the load. Stay with 6061 for general enclosures, brackets, fixtures and anything that will be welded. Our detailed 6061 vs 7075 aluminum comparison breaks the decision down property by property.
Machined 7075 parts cluster wherever strength-to-weight ratio decides the design:
No. Its machinability rating of about 70–80% (relative to free-machining brass) makes it one of the friendlier high-strength alloys. It does need sharper carbide tooling, a rigid setup and better chip control than softer alloys, and it wears tools faster — but with the right parameters it produces short chips and an excellent finish.
7075’s zinc- and copper-rich chemistry makes fusion welds hot-crack as they solidify, and the heat destroys the T6 temper in the weld zone, leaving a weak joint. In practice 7075 parts are joined with fasteners, bonding or shrink fits instead. If a design must be welded, engineers usually switch the welded members to 6061.
7075, by a wide margin. In the T6 temper, 7075 reaches 83,000 psi (572 MPa) tensile strength and 73,000 psi (503 MPa) yield, versus 45,000 psi (310 MPa) and 40,000 psi (276 MPa) for 6061-T6 — plus better fatigue resistance. That strength is why 7075 is specified for highly stressed parts despite its higher price.
Yes. Both Type II sulfuric anodizing and Type III hard anodizing work on 7075, and hard anodizing is the common choice where wear resistance and corrosion protection matter most. Set expectations on cosmetic parts, though: the alloy’s zinc content can give clear anodize a slight yellow-grey cast, and holding a consistent color is harder than on 6061.
Three reasons: its zinc and copper alloying content costs more than 6061’s magnesium-silicon recipe; it is produced in smaller volumes, so fewer sizes and tempers are stocked; and the tighter processing and stress-relief steps (T651, T7351) add mill cost. Expect a noticeable premium per pound over 6061, before machining time is counted.
Only gently, and usually not in the T6 temper — 7075-T6 sheet needs a bend radius of roughly 6–10 times the material thickness and still risks cracking. Parts that need real forming are bent in the soft O (annealed) condition and then heat treated to T6, or redesigned as machined parts — which is one reason so many 7075 components are milled from plate instead of formed.
Machining 7075 aluminum successfully comes down to respecting what the alloy is: a high-strength, heat-treated material that cuts cleanly with sharp carbide and correct speeds and feeds, but punishes dull tools, weak setups and careless material removal with wear, heat and distortion. Start with stress-relieved T651 (or T7351 for harsh environments), rough evenly, finish light, and protect the surface afterwards — and 7075 will hold tolerances and finishes that few lightweight materials can match.
If you are planning a production part, our complete guide to aluminum CNC machining covers the wider process, and Tuowei’s 7075 aluminum machining services team machines 7075-T6 and T7351 parts for aerospace, defense and industrial manufacturing programs — send us your drawing for a quote and a free manufacturability review.