This thread size chart covers the three thread systems you will meet on most drawings: Unified inch threads (UNC and UNF), ISO metric threads (coarse and fine) and NPT pipe threads. For each of these thread sizes you get the major diameter, the pitch or threads per inch (TPI) and the tap drill size, so you can identify a thread, order a fastener or set up a tapping operation.
Réponse rapide : Inch threads are written as diameter and TPI, such as 1/4-20 UNC. Metric threads are written as M plus diameter in mm and pitch, such as M6 x 1.0. For a standard 75% thread, the metric tap drill is roughly the major diameter minus the pitch; for inch sizes, use the table below.
Most thread charts online cover one system, hide the PDF behind a form, or show tolerance tables with no explanation. This one puts all three in one place, explains how to read them, and ends with a free downloadable chart.
Before using any thread chart, decode the callout on the drawing. Two examples cover nearly every case.
1/4-20 UNC-2A – 1/4: nominal major diameter, 1/4 inch – 20: threads per inch (TPI) – UNC: Unified National Coarse series – 2A: tolerance class 2, external thread (A = external, B = internal)
M10 x 1.5-6g – M10: metric thread, 10 mm nominal major diameter – 1.5: pitch, the distance between threads in mm – 6g: tolerance class for an external thread (6H is the common internal class)
For metric coarse threads the pitch is often left off, so M10 means M10 x 1.5. A fine thread always shows its pitch, such as M10 x 1.25. Number sizes such as #8-32 work like fractional inch sizes: the number is the screw size and the second number is the TPI.
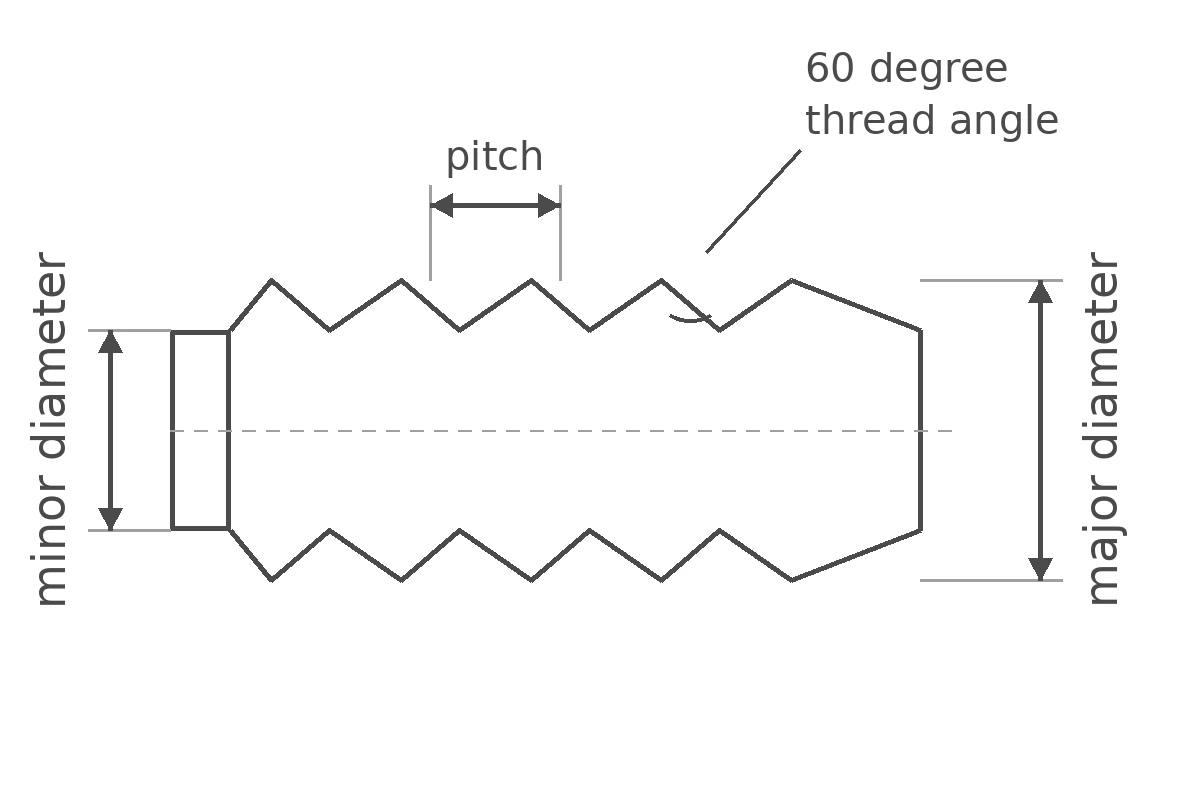
The Unified Thread Standard, defined in ASME B1.1, is the US system for inch fasteners. Coarse (UNC) threads are the default. Fine (UNF) threads have more threads per inch, which gives a little more tensile strength and finer adjustment, but they strip more easily in soft materials.
This UNC UNF thread chart lists major diameter, TPI and the tap drill size for a typical 75% thread.
| Taille | Major dia. (in) | Major dia. (mm) | UNC TPI | UNC tap drill | UNF TPI | UNF tap drill |
|---|---|---|---|---|---|---|
| #0 | 0.0600 | 1.52 | – | – | 80 | 3/64 |
| #1 | 0.0730 | 1.85 | 64 | #53 | 72 | #53 |
| #2 | 0.0860 | 2.18 | 56 | #50 | 64 | #50 |
| #3 | 0.0990 | 2.51 | 48 | #47 | 56 | #45 |
| #4 | 0.1120 | 2.84 | 40 | #43 | 48 | #42 |
| #5 | 0.1250 | 3.18 | 40 | #38 | 44 | #37 |
| #6 | 0.1380 | 3.51 | 32 | #36 | 40 | #33 |
| #8 | 0.1640 | 4.17 | 32 | #29 | 36 | #29 |
| #10 | 0.1900 | 4.83 | 24 | #25 | 32 | #21 |
| #12 | 0.2160 | 5.49 | 24 | #16 | 28 | #14 |
| 1/4 | 0.2500 | 6.35 | 20 | #7 | 28 | #3 |
| 5/16 | 0.3125 | 7.94 | 18 | F | 24 | I |
| 3/8 | 0.3750 | 9.53 | 16 | 5/16 | 24 | Q |
| 7/16 | 0.4375 | 11.11 | 14 | U | 20 | 25/64 |
| 1/2 | 0.5000 | 12.70 | 13 | 27/64 | 20 | 29/64 |
| 9/16 | 0.5625 | 14.29 | 12 | 31/64 | 18 | 33/64 |
| 5/8 | 0.6250 | 15.88 | 11 | 17/32 | 18 | 37/64 |
| 3/4 | 0.7500 | 19.05 | 10 | 21/32 | 16 | 11/16 |
| 7/8 | 0.8750 | 22.23 | 9 | 49/64 | 14 | 13/16 |
| 1 | 1.0000 | 25.40 | 8 | 7/8 | 12 | 59/64 |
Number drills (#) and letter drills (F, I, Q, U) are standard US drill sizes. If you only have metric drills, the nearest metric drill usually works for general tapping, but check the thread percentage for critical or thin-walled parts.
Number sizes run from #0 to #12 for machine screws. The major diameter rises by 0.013 inch per step, starting at 0.060 inch for #0. That is why the #12 screw diameter is 0.216 inch (about 5.49 mm), slightly smaller than 1/4 inch. Wood screws use the same numbering and also come in #14.
ISO metric threads are defined in ISO 261 (general plan) and ISO 724 (basic dimensions). The coarse series is the default worldwide; fine pitches are used for adjusting screws, thin walls and higher clamping precision.
This metric thread chart gives the coarse pitch, a common fine pitch and the tap drill size for each.
| Taille | Coarse pitch (mm) | Coarse tap drill (mm) | Common fine pitch (mm) | Fine tap drill (mm) |
|---|---|---|---|---|
| M1.6 | 0.35 | 1.25 | 0.2 | 1.4 |
| M2 | 0.4 | 1.6 | 0.25 | 1.75 |
| M2.5 | 0.45 | 2.05 | 0.35 | 2.15 |
| M3 | 0.5 | 2.5 | 0.35 | 2.65 |
| M4 | 0.7 | 3.3 | 0.5 | 3.5 |
| M5 | 0.8 | 4.2 | 0.5 | 4.5 |
| M6 | 1.0 | 5.0 | 0.75 | 5.25 |
| M8 | 1.25 | 6.8 | 1.0 | 7.0 |
| M10 | 1.5 | 8.5 | 1.25 | 8.75 |
| M12 | 1.75 | 10.2 | 1.25 | 10.75 |
| M14 | 2.0 | 12.0 | 1.5 | 12.5 |
| M16 | 2.0 | 14.0 | 1.5 | 14.5 |
| M20 | 2.5 | 17.5 | 1.5 | 18.5 |
| M24 | 3.0 | 21.0 | 2.0 | 22.0 |
| M30 | 3.5 | 26.5 | 2.0 | 28.0 |
The quick rule for metric threads: tap drill = major diameter minus pitch. M8 x 1.25 gives 6.75, rounded to the standard 6.8 mm drill. Fine-pitch tap drills in the table follow the same rule; in practice shops round to the nearest available drill.
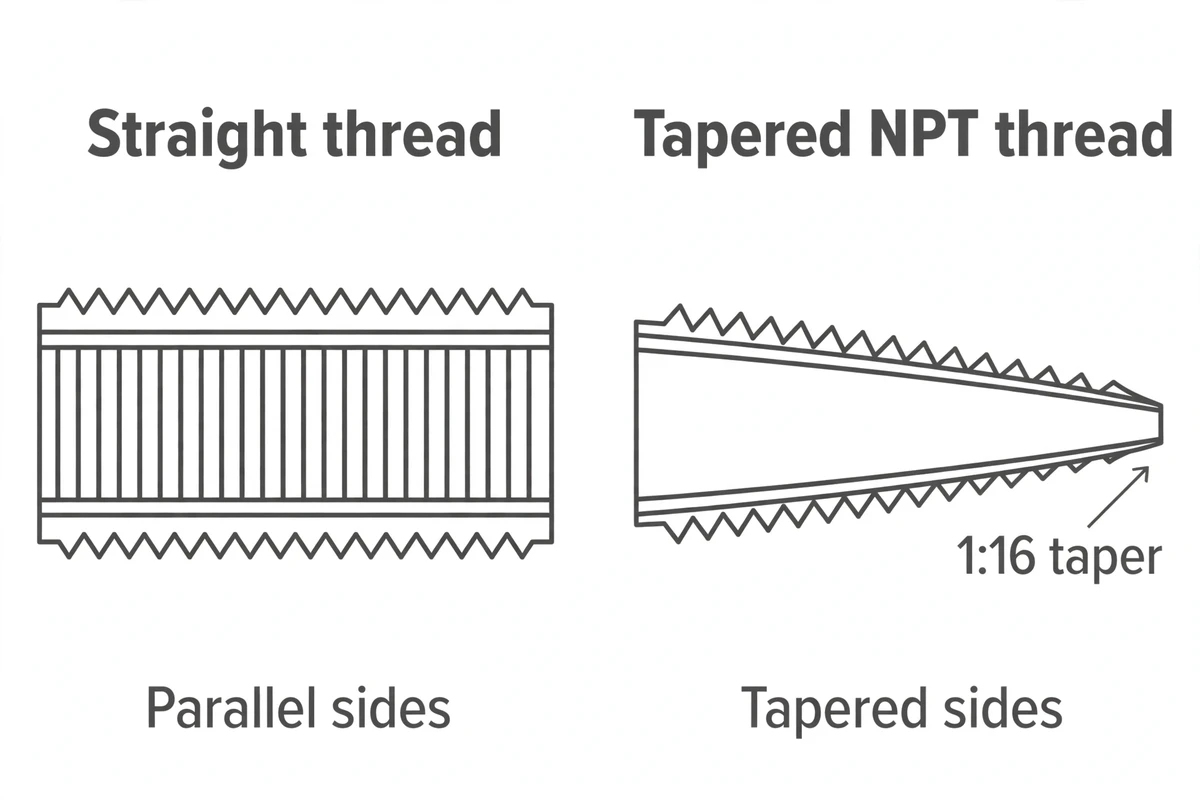
A pipe thread size chart works differently: pipe threads are sized by the nominal pipe size, not the measured diameter, which confuses almost everyone the first time. A 1/2 inch NPT fitting has an outside diameter of 0.840 inch. NPT threads are tapered at 1 in 16 on diameter so they seal as they tighten, usually with thread sealant or PTFE tape. The US standard is ASME B1.20.1.
| Nominal pipe size | TPI | Pipe outside diameter (in) | Pipe outside diameter (mm) |
|---|---|---|---|
| 1/16 | 27 | 0.3125 | 7.94 |
| 1/8 | 27 | 0.405 | 10.29 |
| 1/4 | 18 | 0.540 | 13.72 |
| 3/8 | 18 | 0.675 | 17.15 |
| 1/2 | 14 | 0.840 | 21.34 |
| 3/4 | 14 | 1.050 | 26.67 |
| 1 | 11.5 | 1.315 | 33.40 |
| 1-1/4 | 11.5 | 1.660 | 42.16 |
| 1-1/2 | 11.5 | 1.900 | 48.26 |
| 2 | 11.5 | 2.375 | 60.33 |
NPT, NPTF (dryseal) and BSPT (British, 55° thread angle) are not interchangeable even when the sizes look similar. Mixing NPT and BSP is a common cause of leaking fittings on imported equipment.
Engineers often ask which metric thread is close to a familiar inch size. These pairs are close in diameter, but the pitches differ, so the threads will not mate.
| Inch size | Diameter | Closest metric | Diameter |
|---|---|---|---|
| #4-40 | 2.84 mm | M3 x 0.5 | 3.0 mm |
| #8-32 | 4.17 mm | M4 x 0.7 | 4.0 mm |
| #10-24 / #10-32 | 4.83 mm | M5 x 0.8 | 5.0 mm |
| 1/4-20 | 6.35 mm | M6 x 1.0 | 6.0 mm |
| 5/16-18 | 7.94 mm | M8 x 1.25 | 8.0 mm |
| 3/8-16 | 9.53 mm | M10 x 1.5 | 10.0 mm |
| 1/2-13 | 12.70 mm | M12 x 1.75 | 12.0 mm |
A 1/4-20 screw may start in an M6 hole and then bind or cross-thread after a turn or two. If a fastener feels tight early, stop and check the system before forcing it.
A typical trap: a measured 0.245 inch diameter is a 1/4 inch thread with slightly worn crests, not a special size. Actual major diameters run a little under nominal on external threads.
Thread class sets how tight the fit is, independent of the thread sizes listed above.
| Classe | Fit | Utilisation courante |
|---|---|---|
| 1A / 1B | Loose | Quick assembly, dirty or damaged threads |
| 2A / 2B | Standard | The large majority of commercial fasteners |
| 3A / 3B | Tight | Aerospace, precision instruments, high-strength bolts |
| 6g / 6H (metric) | Medium, general purpose | Default for metric fasteners |
Specify 2A/2B or 6g/6H unless you have a specific reason not to. Tighter classes cost more to make and to inspect.
When we review drawings for machined parts, these thread issues come up again and again:
Threads also show up on drawings next to weld callouts and machining notes; our welding symbols chart covers how to read those. On a lathe, external threads are cut with single-point threading tools, explained in our guide to lathe cutting tools.
The PDF thread chart contains the UNC UNF thread chart, the metric coarse and fine tables and the NPT table from this page on two printable pages. It is free, with no email form. Pin it next to the drill rack or keep it with your drawing templates.
Download the Free Thread Size Chart (PDF)
The most common standard threads are UNC and UNF inch threads from #0 to 1 inch, ISO metric coarse threads from M1.6 to M30, and NPT pipe threads from 1/16 to 2 inch. In US general machinery, 1/4-20, 5/16-18, 3/8-16 and 1/2-13 UNC dominate; worldwide, M3 to M12 coarse threads are most common.
Yes. M10 means an ISO metric thread with a 10 mm nominal major diameter. If no pitch is given, it is the coarse pitch, 1.5 mm, so M10 equals M10 x 1.5. A fine version is written with its pitch, such as M10 x 1.25. The tap drill for M10 x 1.5 is 8.5 mm.
8-32 is UNC, the coarse thread for a #8 screw, with 32 threads per inch and a 0.164 inch major diameter. The fine version is 8-36 UNF. Both use a #29 tap drill for a standard thread. Similarly, 4-40 is UNC and 4-48 is UNF.
M6 x 1.0 is the closest metric thread to 1/4-20. The diameters are 6.0 mm and 6.35 mm, and the pitches are 1.0 mm and about 1.27 mm, so they do not interchange. A 1/4-20 screw may start in an M6 hole but will bind or damage the threads after a turn or two.
Measure the outside diameter of the bolt with calipers, then check the pitch with a thread gauge, trying both inch and metric leaves. Compare both values with a thread chart. If the diameter tapers along the length, it is a pipe thread. A slightly undersized reading usually means normal wear, not a special size.
Keep a thread chart at hand, but remember that a correct callout prevents most thread problems: name the system and size, the pitch or TPI, the class, and the depth. Use coarse threads by default, fine threads only where you need them, and enough engagement in soft metals.
We machine tapped holes, single-point threads and thread milling on turned and milled parts every day. See our Services d'usinage CNC, Tournage CNC et Fraisage CNC, ou upload a drawing for a quote. Visit Précision Tuowei for our full range of services.
Sources et lectures complémentaires – ASME B1.1 Unified Inch Screw Threads (UN, UNR and UNJ Thread Form): asme.org – ISO 261 ISO general purpose metric screw threads: General plan and ISO 724 Basic dimensions: iso.org – ASME B1.20.1 Pipe Threads, General Purpose, Inch: asme.org
Thread size values in this chart are for reference. Confirm critical dimensions and tap drill sizes against the current standards and your tooling supplier before production.
Tap drill sizes are for an approximately 75% thread and are standard reference values. For critical parts, check thread percentage, material and tap supplier recommendations.