¿Necesita soluciones de mecanizado expertas? Nuestro equipo de Tuowei Proto está aquí para ayudarle con todas sus necesidades de fabricación. Póngase en contacto con nosotros hoy mismo para obtener un presupuesto para sus proyectos en curso o futuros.
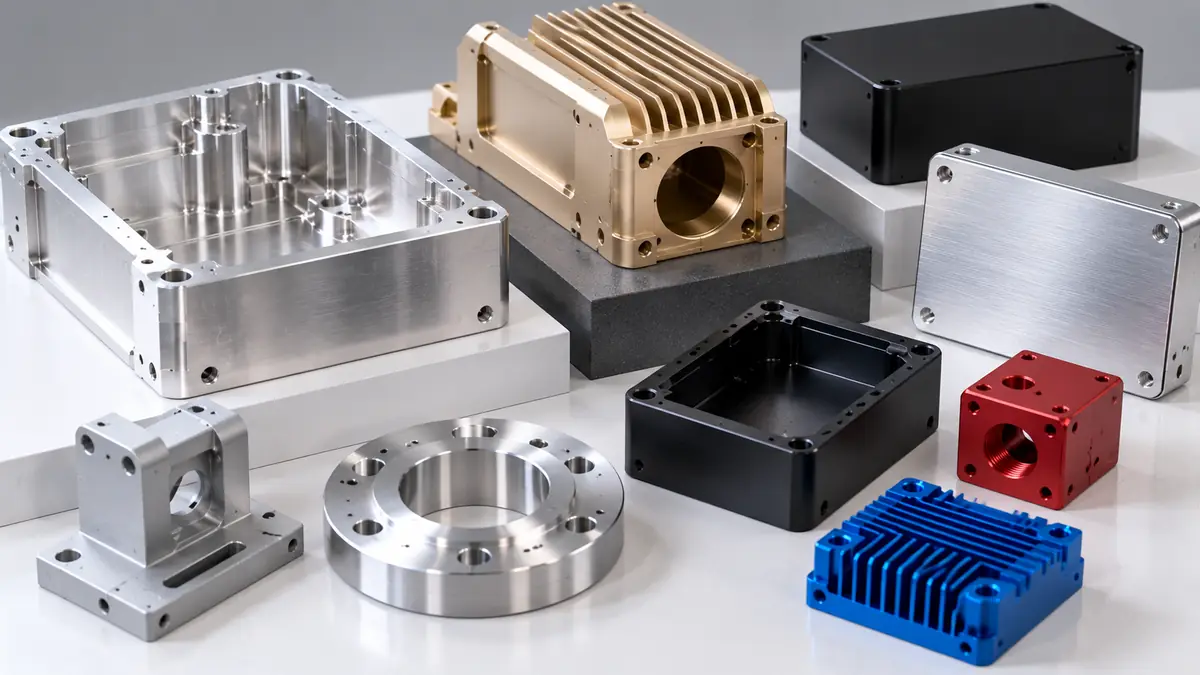
The most common surface finishes for CNC machined aluminum are as-machined, bead blasting, anodizing, chromate conversion coating (chem film), powder coating and electroless nickel plating. Each one does a different job. Anodizing protects and colors the part, chem film protects while keeping it electrically conductive, bead blasting changes only the look, and powder coat and plating add thicker functional layers.
Short answer: For most aluminum parts, Type II anodizing is the best all-round finish: good corrosion protection, many colors and only small dimensional change. Choose chem film when the surface must stay conductive, Type III hardcoat for wear, powder coat for thick colored protection, and bead blasting before anodizing for an even matte look.
This guide compares each finish on protection, appearance, conductivity, dimensional change and cost, then shows how to choose and specify one.
| Finish | What it does | Dimensional effect | Electrically conductive? | Look | Relative cost |
| As-machined | Nothing added; tool marks visible | Ninguno | Sí | Metallic with tool marks | Lowest |
| Granallado | Even matte texture, hides tool marks | Very small; edges soften | Sí | Uniform satin matte | Bajo |
| Brushing or polishing | Directional grain or gloss | Very small | Sí | Satin grain or shiny | Low to medium |
| Type II anodizing | Corrosion protection, dyed colors | Small growth | No (insulating) | Clear or colored | Medio |
| Type III hardcoat | Wear and abrasion resistance | Larger growth | No (insulating) | Gray to dark bronze, dark dyes | Más alto |
| Chem film (chromate conversion) | Corrosion protection, paint base | Negligible | Yes (Class 3) | Clear, gold or iridescent | Bajo |
| Powder coating | Thick colored protective layer | Thickest | No (insulating) | Any color, matte to gloss | Medio |
| Electroless nickel | Hard, uniform metallic coating | Uniform, specified thickness | Sí | Bright to semi-bright nickel | Más alto |
The sections below explain each of these aluminum finishing options, including the exceptions.
Two terms get mixed up. Surface roughness is the texture the machining leaves, usually measured as Ra, the average height of the peaks and valleys. Surface finishing is anything done to the part after machining: blasting, coating or plating.
They are linked across all aluminum surface finishes. Most coatings follow the texture underneath, so a clear anodized finish on a rough surface still looks rough.
Tuowei’s standard as-machined finish is about 125 µin Ra (3.2 µm), with visible tool marks. That suits most functional parts. Smoother machined finishes are possible with extra passes, but they add time, so specify them only where a surface seals, slides or will be seen.
The simplest aluminum finishing options change only the surface texture.
As-machined means the part ships as it came off the machine, after deburring. It is the cheapest option and keeps every dimension exactly as cut. The trade-off is that bare aluminum forms only a thin natural oxide, so it will mark and dull in handling and corrode in harsh environments.
Granallado sprays fine glass beads at the surface to create a uniform satin-matte texture. It hides tool marks and small handling scratches, which is why it is so often done before anodizing on cosmetic parts. It adds no protection on its own. Blasting can soften sharp edges and slightly change very fine features, so mask sealing faces and precision bores.
Cepillado produces a straight, directional grain, often used on visible panels. Pulido produces a bright, reflective surface but is labor-intensive and shows every later scratch. Tumbling or vibratory finishing rounds edges and smooths many small parts at once, at the cost of less control over individual surfaces.
Our view: for any aluminum part with a cosmetic finish requirement, specify bead blasting before anodizing. It is inexpensive and removes most of the variation that makes anodized parts look inconsistent from batch to batch.
Anodizing converts the aluminum surface into a hard aluminum oxide layer, grown from the metal itself rather than applied on top. It is the most widely used of all finishes for machined aluminum.
The governing US specification is MIL-PRF-8625, available through the DoD ASSIST database. Two types matter for most machined parts:
Anodizing insulates the surface, so grounding points need masking. Alloy also affects color: 6061 gives the most even result, while 7075 and 2024 can look darker or less uniform in clear and light dyes.
Chromate conversion coating, also called chem film or by the brand name Alodine, is a thin chemical conversion layer applied by dipping the part in a solution. It protects against corrosion, provides an excellent base for paint and primer, and, unlike anodizing, leaves the surface electrically conductive.
In the US it is specified under MIL-DTL-5541, which sorts coatings by type and class:
The type matters more than it used to. Hexavalent chromium is one of the substances restricted by the EU RoHS Directive, which sets a maximum of 0.1% by weight in homogeneous materials for electrical and electronic equipment. If your product must be RoHS compliant, specify MIL-DTL-5541 Type II. Rules and exemptions change, so confirm the current requirements for your market before release.
Type I coatings often have a gold or iridescent color. Type II coatings are commonly clear or light blue, which surprises buyers expecting the traditional gold look. The coating is very thin, so it has a negligible effect on dimensions, but it is also softer and less wear resistant than anodizing.
Tuowei offers revestimiento de conversión al cromato on aluminum parts.
Powder coating applies a dry polymer powder electrostatically, then cures it in an oven into a continuous, colored layer. It is tough, available in almost any color, and good for parts exposed to weather or handling.
It is also the thickest of the common aluminum finishes, which makes it a poor choice for close-tolerance features. Threads, bores, mating faces and grounding points are normally masked. Sharp edges carry thinner coating, so small edge radii help the coating last. On aluminum, a conversion coating or other pretreatment under the powder improves adhesion and corrosion resistance.
Wet paint follows similar rules. For precise color matching across parts, specify a color standard such as a RAL number, and approve a sample before production.
Electroless nickel deposits a nickel-phosphorus alloy chemically, without electric current, so it builds a very uniform thickness even inside bores and on complex shapes. It adds hardness, wear resistance and solderability, and it keeps the surface conductive.
ASTM B733 classifies electroless nickel by phosphorus content:
| Phosphorus range | Main characteristics |
| Lower (1 to 3% P) | Microcrystalline; used where solderability and conductivity matter |
| Low (2 to 4% P) | High as-plated hardness (620 to 750 HK100) for wear resistance |
| Medium (5 to 9% P) | The general-purpose choice for wear and corrosion resistance |
| High (above 10% P) | Best salt spray and acid resistance; non-magnetic above 11.2% P |
Plating aluminum needs a special pretreatment, usually a zincate step, to get the nickel to adhere. That adds process risk and cost, so electroless nickel is chosen when its specific properties are needed, not as a general surface finish for aluminum. Other electroplated finishes, such as tin or silver for electrical contacts, are possible on aluminum but less common.
Supplier finish lists usually cover every metal they machine, so some options simply do not apply to aluminum:
Tuowei’s finish list includes black oxide and electropolishing for its steel and stainless parts. For aluminum parts, choose from the machined aluminum finishes in the comparison table above.
This is where finishing aluminum parts affects machining. MIL-PRF-8625 states that each anodized surface grows by about half the coating thickness. For a Type III coating at the nominal 0.002 in., that is about 0.001 in. per surface, or about 0.002 in. on a diameter: bores shrink, shafts grow and threads tighten.
| Finish | Planning guideline |
| As-machined | No change |
| Granallado | Negligible, but mask precision faces and bores |
| Chem film | Negligible for most tolerances |
| Type II anodizing | Small; check fine threads and precision fits |
| Type III anodizing | About half the coating thickness per surface; allow for it in machining |
| Electroless nickel | Uniform and specified; machine undersize by the coating thickness |
| Powder coating | Thickest; mask all fits, threads and datum faces |
A practical rule for all machined aluminum finishes: put a note on the drawing saying whether dimensions apply before or after finishing. That single note removes most disputes about coated parts.
Conductivity is one of the most overlooked requirements when choosing aluminum surface finishes. Many aluminum parts need to carry current: chassis grounds, EMI-shielded enclosures and connector mounts. Anodizing and powder coating both insulate, so they cannot be used on contact surfaces without masking.
The usual solutions:
Para electrónica de consumo housings, the second approach is common: an anodized finish for looks and protection, with small conductive pads for grounding.
Aluminum finishes are often layered:
Each extra step adds handling and lead time, and each one needs clear masking instructions on the drawing.
| If the part needs | Elija | Notas |
| General corrosion protection and color | Type II anodizing | The default for most parts |
| An even cosmetic finish | Bead blast plus Type II anodizing | Hides tool marks |
| Wear resistance on sliding surfaces | Type III hard anodizing | Plan for dimensional growth |
| Electrical conductivity | Chem film Class 3 or electroless nickel | Anodizing insulates |
| RoHS compliance with chem film | MIL-DTL-5541 Type II | Type I contains hexavalent chromium |
| A tough outdoor color finish | Powder coating over pretreatment | Mask fits and threads |
| Hardness and solderability | Electroless nickel | Higher cost and process risk |
| Lowest cost for internal parts | As-machined | No protection added |
Our position: when a part has no special requirement, choose Type II anodizing over powder coating for machined aluminum. It adds far less thickness, holds tighter tolerances, and does not chip the way a thick polymer layer can.
Para aerospace components, the finish is often set by the customer’s specification, so confirm the exact type, class and revision before quoting.
Most aluminum surface finishes are batch processes. Parts are racked, treated and inspected in lots, so finishing adds its own queue time on top of machining, and each extra finish in a stack adds another. Lot charges mean a handful of prototypes can cost almost as much to anodize as a larger batch.
Masking is usually the biggest variable. Plugging threads and taping faces is manual work priced per feature, so a part with many masked areas can cost more to finish than a simpler part with a thicker coating. Grouping parts that share a finish into one lot, and finishing aluminum parts in the same color together, keeps both cost and color variation down.
A complete callout for any of these aluminum finishing options removes guesswork:
Tuowei quotes machining and finishing together through its Servicios de mecanizado CNC, so masking and dimensional allowances can be planned before the first cut.
Most of these are fixed with a better drawing note, not a better process. Our CNC milling services team reviews finish callouts together with the machining so problems surface at quote stage.
Choosing between surface finishes for CNC machined aluminum starts with the part’s job: protection, conductivity, wear, appearance or cost. Type II anodizing covers most needs, chem film covers conductivity, hardcoat covers wear, and bead blasting makes cosmetic parts consistent.
Send your drawing and finish requirements to Precisión Tuowei, and our engineers will confirm the finish, masking and dimensional allowances with your quote.
Q: What is the best surface finish for aluminum CNC parts?
A: For most parts, Type II anodizing is the best all-round choice: good corrosion protection, many colors and small dimensional change. Use chem film where the surface must conduct, Type III hardcoat for wear, and bead blasting before anodizing when appearance matters.
Q: What is the difference between anodizing and chem film?
A: Anodizing grows a thicker, harder oxide layer that insulates the surface and can be dyed. Chem film is a much thinner chemical conversion coating that protects against corrosion, makes a good paint base and stays electrically conductive, but it is softer and less wear resistant than anodizing.
Q: How much does anodizing change part dimensions?
A: MIL-PRF-8625 states that each coated surface grows by about half the coating thickness. For Type III hardcoat at the nominal 0.002 in., that is about 0.001 in. per surface. Type II changes dimensions less, but fine threads and precision fits still need checking or masking.
Q: Does bead blasting change dimensions?
A: Only slightly. It creates a matte texture and can soften sharp edges, but it does not add a coating. Precision bores, sealing faces and fine features should still be masked, and bead blasting should be called out on the drawing when it is required before anodizing.
Q: Is Alodine RoHS compliant?
A: It depends on the type. MIL-DTL-5541 Type I chem film contains hexavalent chromium, which the EU RoHS Directive limits to 0.1% by weight in homogeneous materials. Type II chem film does not contain hexavalent chromium and is the usual choice for RoHS products.
Written by Andy, Manufacturing Engineer at TUOWEI Precision. Andy specializes in CNC machining, precision manufacturing, and production engineering, with hands-on experience supporting projects from rapid prototyping through full-scale production. He works closely with engineering and manufacturing teams to evaluate materials, tolerances, machining processes, and design manufacturability. His articles provide practical, technically informed insights to help engineers and buyers make better manufacturing decisions, optimize production efficiency, and achieve consistent part quality. Explore TUOWEI Precision’s CNC machining and custom manufacturing solutions for your next project.
From rapid prototypes to scalable production, Tuowei Precision delivers reliable CNC machining with accuracy and consistency at every step. Start your project today.
Manténgase al día sobre el mecanizado CNC real, las tendencias del sector y las perspectivas de producción en Tuowei Precision, pero se instala para permitirle tomar mejores decisiones de producción.