Sheet metal forming is the group of manufacturing processes that reshape flat metal sheet into a 3D part by plastic deformation, without removing material. Bending, stamping, deep drawing, roll forming, stretch forming, spinning and hydroforming are the main methods. The right forming process depends on part shape, material, tolerance and production volume.
Respuesta rápida: For low to medium volumes of brackets, enclosures and chassis, press brake bending is usually the most cost-effective method. For thousands of identical parts, stamping with progressive dies wins on cost per part. Deep drawing makes cups and cans, roll forming makes long constant profiles, and hydroforming and spinning suit complex or round shapes in lower volumes.
Most guides on forming sheet metal list the processes and stop there. This one also covers the numbers that decide whether a formed part comes out right: springback, K-factor, bend allowance, minimum bend radius and the design rules that keep holes from tearing near a bend.
When metal is stressed beyond its yield point but below its ultimate tensile strength, it deforms permanently without breaking. Every forming process uses that window. A punch, die, roller or pressurized fluid pushes the sheet into a new shape, and the metal keeps that shape when the force is removed, apart from a small elastic springback.
Sheet usually means metal thinner than about 6 mm. Thicker material is plate and is normally formed on heavier equipment. Our tabla de espesores de chapa metálica converts gauge numbers to millimeters and inches for steel, stainless and aluminum.
Some guides list laser cutting and shearing as forming processes. They are not. Cutting processes such as laser cutting, punching, blanking and shearing separate material along a line. A forming process changes the shape of the sheet without separating it. Most formed sheet metal parts use both: the flat pattern is cut first, then formed. The difference matters for quoting, because cutting and forming run on different machines and carry different tolerances.
The types of sheet metal forming below cover nearly every formed sheet metal part you will see, from a simple bracket to a deep-drawn housing.
| Proceso | Cómo funciona | Ideal para | Volumen |
|---|---|---|---|
| Press brake bending | Punch presses sheet into a V-die along a straight line | Brackets, enclosures, chassis | Prototype to medium |
| Stamping (forming dies) | Press and matched dies form the part in one or more strokes | Panels, clips, brackets in volume | Alta |
| Deep drawing | Punch draws a blank into a die cavity | Cups, cans, sinks, housings | De medio a alto |
| Roll forming | Sheet passes through a series of rollers | Long constant profiles, rails, studs | High, long lengths |
| Stretch forming | Sheet is stretched over a form block | Large curved aircraft and façade panels | Bajo a medio |
| Metal spinning | Disc is pressed onto a rotating mandrel | Round parts: cones, domes, reflectors | Bajo a medio |
| Hydroforming | Fluid pressure forms sheet or tube into a die | Complex shapes with even thickness | Medio |
| Curling and hemming | Edge is rolled or folded back | Safe edges, hinges, stiffening | Cualquiera |
| Flanging and embossing | Local edges or raised features formed | Stiffening ribs, mounting flanges | Cualquiera |
| Incremental forming | CNC tool forms the sheet point by point | Prototypes, one-offs | Muy bajo |
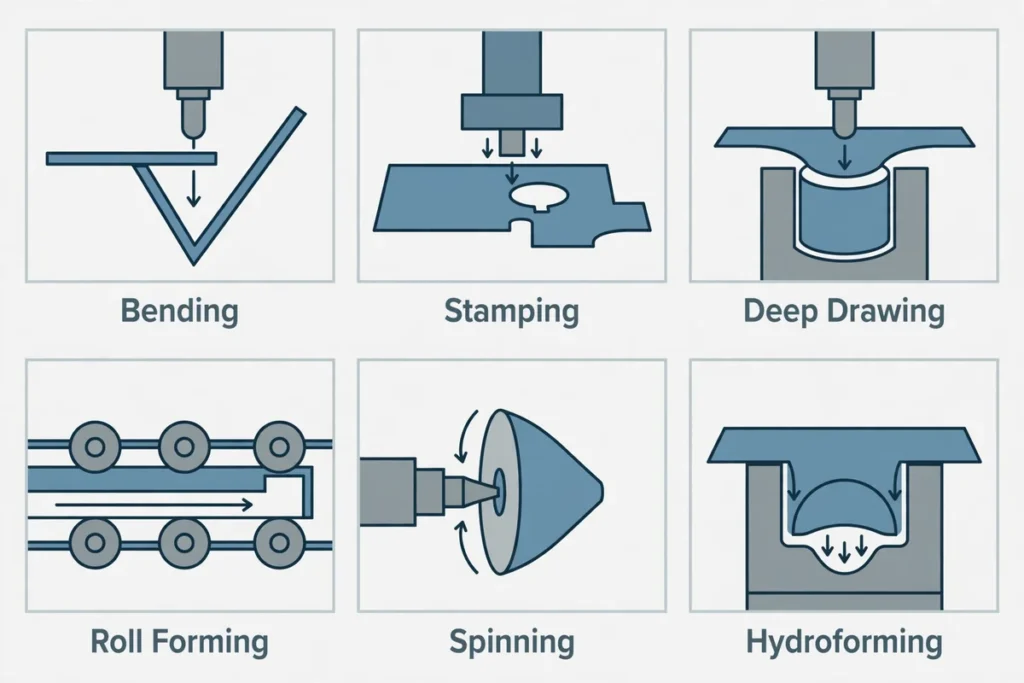
Bending is the most common sheet metal forming process. A press brake drives a punch into a V-shaped die, and the sheet bends along a straight line. There are three main methods:
Wipe bending, rotary bending and roll bending (for large radii and cylinders) are variations used for specific shapes. Our step-by-step guide on Cómo doblar chapa metálica covers tooling and setup in more detail.
Stamping uses a press and a set of matched dies. A single press stroke can blank, pierce, bend, emboss and flange the part, or a progressive die can carry a strip through several stations, finishing one part per stroke. Of all sheet forming methods, stamping has the lowest cost per part at high volume but the highest upfront tooling cost.
| Die type | Cómo funciona | Uso habitual |
|---|---|---|
| Progressive die | Strip moves through stations; each stroke advances it one step | Small to medium parts in high volume |
| Compound die | Several cutting operations in one stroke at one station | Flat parts like washers |
| Transfer die | Parts are moved between separate stations | Larger or deeper parts |
| Line dies | Separate dies in separate presses | Large panels, lower volumes |
In deep drawing, a punch pushes a flat blank into a die cavity while a blank holder controls how the metal flows in. A part is usually called “deep drawn” when its depth exceeds its diameter. The limiting draw ratio for the first draw of steel is commonly around 2, so deeper parts need redraws, sometimes with annealing in between. Wrinkling at the flange and tearing at the punch radius are the classic failures; both are controlled with blank holder pressure, lubrication and generous radii.
Roll forming feeds a long strip through a series of roller stations, each bending it a little more, until the final profile emerges. It produces long parts with a constant cross section, such as rails, channels, trim and steel studs, at high speed with very consistent dimensions. Tooling is expensive, so it suits long runs.
Stretch forming grips the sheet at both ends and stretches it over a shaped block, which keeps springback low on large, gently curved panels. Metal spinning presses a disc against a rotating mandrel to make round, hollow parts with low tooling cost. Hydroforming, a fluid-based forming process, uses high-pressure fluid to push the sheet against a single die half, producing complex shapes with fairly even wall thickness and good surface finish.
These smaller operations finish edges and add stiffness. Curling rolls an edge into a round bead; hemming folds the edge back on itself to remove sharp edges; flanging bends a narrow lip; embossing raises ribs or logos. They often run as extra stations in a stamping die or as extra hits on a press brake.
When forming sheet metal, formability depends on ductility, strength and how much the material work-hardens.
| Material | Formability | Notas |
|---|---|---|
| Low-carbon steel (CRS, SPCC, DC01) | Excelente | Default for brackets and enclosures; needs coating or paint |
| Acero galvanizado | Muy bien | Zinc can flake at tight bends |
| Stainless steel 304 | Bien | High springback; work-hardens fast; needs more tonnage |
| Aluminio 5052-H32 | Muy bien | Best general-purpose formable aluminum |
| Aluminio 6061-T6 | Deficiente | Cracks at tight bends; use larger radii or form in O/T4 temper |
| Cobre y latón | Excelente | Soft; marks easily |
After the punch lifts in any bending-based forming process, the elastic part of the deformation recovers and the bend opens slightly. This is springback. It increases with:
Shops compensate by overbending (bending past the target so it springs back to the right angle), bottoming or coining, adjusting the stroke on CNC press brakes with angle measurement, or adding stiffening features that lock the bend. Expect a first-article check on any new material or thickness, because springback is the single biggest source of angle error in formed sheet metal.
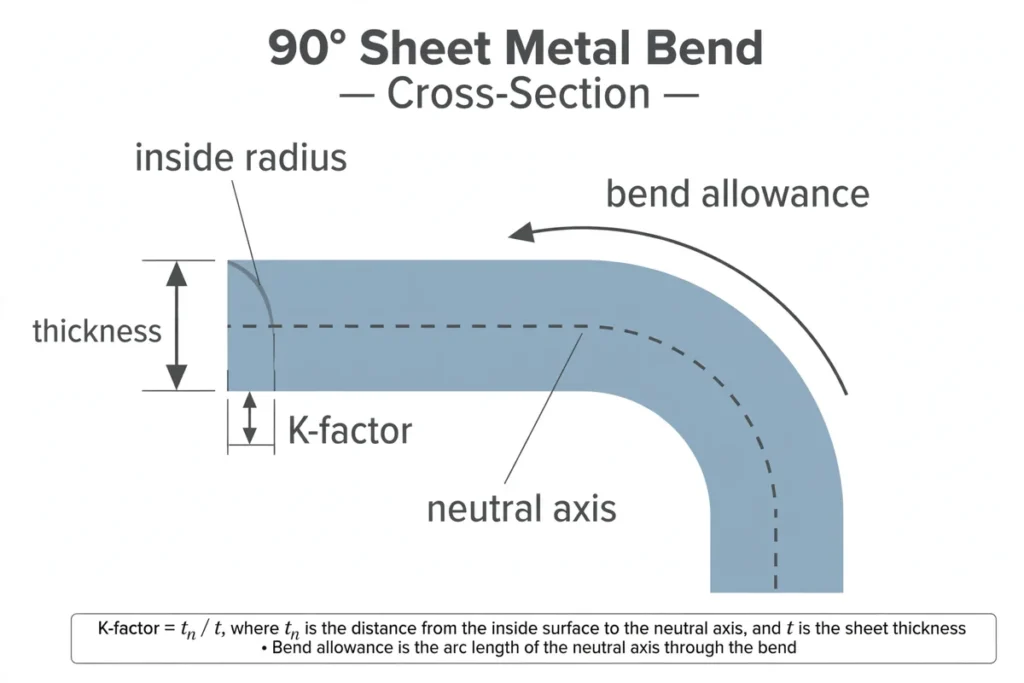
To make a flat pattern for formed sheet metal that bends to the right size, you need to know how much material the bend consumes. During bending, the inside compresses and the outside stretches. The neutral axis, which neither stretches nor compresses, shifts toward the inside. The K-factor is the position of that axis as a fraction of thickness.
Worked example: a 90° bend in 2 mm steel with a 2 mm inside radius and K = 0.44.
So a part with two 50 mm outside flanges needs a flat length of 50 + 50 − 3.48 = 96.52 mm. Our bending guide walks through more bend examples step by step. CAD software does this calculation, but only if the K-factor in the sheet metal settings matches the shop’s tooling, which is why we ask customers to share flat patterns only as a reference.
Bending tighter than the material allows causes cracking on the outside of the bend. These typical starting values assume bending across the rolling direction.
| Material | Typical minimum inside radius |
|---|---|
| Low-carbon steel | 0.5 to 1 × thickness |
| Stainless steel 304 | 1 to 2 × thickness |
| Aluminio 5052-H32 | 1 to 1.5 × thickness |
| Aluminio 6061-T6 | 2 to 4 × thickness or more |
| Copper (soft) | About 0.5 × thickness |
Using one standard inside radius for every bend on a part, often equal to the material thickness, lets the shop run all bends with the same tooling and lowers cost.
These sheet metal design guidelines prevent the most common problems in forming sheet metal we see on incoming drawings.
Tolerances for formed sheet metal depend on the process, material and part size, so confirm them with your supplier. As general guidance for press brake work, bend angles are commonly held to about ±0.5° to ±1°, and dimensions across a single bend to a few tenths of a millimeter. In any sheet forming job, laser-cut features on the same flat surface hold tighter tolerances than features measured across bends. General tolerances on drawings are often specified to ISO 2768, and cold bending of flat steel products is covered by DIN 6935.
Forming cost comes from three places: tooling, machine time and material. How they balance depends almost entirely on volume.
| Factor de coste | Press brake | Progressive stamping |
|---|---|---|
| Herramientas | Standard punches and dies, little or no custom tooling | Custom die, often the largest single cost |
| Setup | Minutes per bend sequence | Hours to set a die, then very fast |
| Coste por pieza | Rises with every bend and handling step | Falls steeply as volume grows |
| Cambios de diseño | Cheap: edit the flat pattern | Expensive: rework or rebuild the die |
On press brake parts, every extra bend, flip and tool change adds handling time. A bracket with four bends in one direction is cheaper than one with the same four bends that needs the part turned over twice. Tight tolerances add cost too, because they need more first-article checks and sometimes slower angle-measuring cycles.
Material choice matters as well. Stainless steel needs more tonnage and springs back more than mild steel, so expect longer setup and more trial bends. Pre-plated or pre-painted sheet saves a finishing step but can mark or crack at tight bends.
Our honest advice: if you expect fewer than a few thousand parts a year, or the design may still change, stay with laser cutting and press brake forming. Move to a stamping die only once the part is stable and the volume pays back the tooling.
| Situation | Elección habitual | Por qué |
|---|---|---|
| 1 to a few hundred parts, straight bends | Laser cutting plus press brake | No dedicated tooling; fast changes |
| Thousands to millions of identical parts | Progressive stamping | Lowest cost per part once tooling is paid |
| Cups, cans or deep housings | Deep drawing | Forms depth without seams |
| Long, constant profiles | Roll forming | High speed, consistent sections |
| Round, hollow parts in low volume | Metal spinning | Cheap tooling |
| Large curved panels | Stretch forming | Low springback on big parts |
| Complex shapes, even wall thickness | Hydroforming | Single-sided die, good finish |
| Prototype of a stamped part | Laser cut and bend, or incremental forming | Validate the design before buying a die |
A useful rule when choosing among types of sheet metal forming: start with laser cutting and press brake forming while the design is changing, then move to stamping tooling once volumes and the design are stable. Redesigning a part after a progressive die is built is expensive, so freeze the design before you commit to a high-volume forming process.
It means reshaping flat metal sheet into a 3D part by bending, stretching or drawing it beyond its yield point, so it keeps the new shape. No material is removed. Common methods include press brake bending, stamping, deep drawing, roll forming, stretch forming, spinning and hydroforming.
The main methods are bending on a press brake, stamping with matched dies, deep drawing for cups and housings, roll forming for long profiles, stretch forming for large curved panels, metal spinning for round parts and hydroforming for complex shapes. Curling, hemming, flanging and embossing finish edges and add stiffness.
Cutting separates material along a line, using processes such as laser cutting, punching, blanking and shearing. Forming changes the shape without separating material, using bending, drawing or stretching. Most sheet metal parts are cut flat first and then formed, and the two steps run on different machines with different tolerances.
A forming tool is any punch, die or roller that shapes the sheet. On a press brake it is the upper punch and lower V-die. In stamping it is the matched die set. Special forming tools on turret punches also create louvers, extrusions, embosses and countersinks directly in flat sheet.
The K-factor is the location of the neutral axis in a bend, expressed as a fraction of the sheet thickness. It is typically between 0.3 and 0.5. CAD programs use it to calculate bend allowance and flat pattern length, so it should match the tooling and material the shop will actually use.
Choose the sheet forming method by shape and volume, design with consistent radii and enough distance between holes and bends, and agree on K-factor and tolerances with your supplier before cutting the first flat pattern. Those steps make forming sheet metal predictable and prevent most cracked bends, distorted holes and parts that do not assemble.
We cut, form, weld and finish sheet metal parts from prototypes to production. See our servicio de fabricación de chapas metálicas, servicio de plegado de metales and laser cutting services. To price a part, Sube tu dibujo para recibir un presupuesto o visita Precisión Tuowei.
Fuentes y lecturas recomendadas
– International Organization for Standardization, ISO 2768-1 General tolerances: iso.org
– DIN 6935 Cold bending of flat steel products: din.de
K-factors, minimum bend radii, DFM distances and tolerances are typical starting values. Confirm them with test bends on your material and with your supplier’s tooling.