

Black oxide is a chemical conversion coating that turns the surface of steel, stainless steel or copper parts a uniform black color. Unlike paint or plating, it does not deposit a separate layer on top of the metal. Instead, a chemical reaction between the part and an alkaline solution converts the surface into magnetite (Fe3O4), a stable iron oxide that is part of the metal itself.
Short answer: Black oxide coating is a thin, low-cost surface treatment that gives steel parts a black appearance, mild corrosion protection, reduced light reflection and minimal dimensional change. Its dimensional effect is generally small compared with deposited coatings, making it a practical option for CNC machined steel components with tight fits. This guide covers the black oxide process, types, corrosion performance, compatible materials and how it compares to other surface finishes for machined parts.
Black oxide works through a controlled chemical reaction between iron on the part surface and an oxidizing salt solution. The reaction creates a thin layer of magnetite (Fe3O4) that is chemically bonded to the base metal.
The key difference between black oxide and coatings like powder coating or plating is that the oxide layer grows from the metal itself rather than sitting on top.
A typical hot black oxide layer on steel is only 0.5 to 1.5 micrometers (0.00002 to 0.00006 inches) thick. That is thin enough to preserve the part dimensions to within a fraction of a tenth of a thousandth, which is why black oxide is a preferred finish for precision-machined steel parts where every thousandth matters.
The black color comes from magnetite itself. It absorbs light effectively, reducing glare. That property makes black oxide a standard finish on firearms, optical equipment, measuring tools and any part where reflected light is a problem.
On its own, the magnetite layer is porous. To get useful corrosion protection, the part must be sealed immediately after blackening, usually by dipping in oil, wax or a lacquer. The sealant fills the pores and creates the actual corrosion barrier.
There are three main black oxide processes. Each uses a different operating temperature and chemistry, and each has trade-offs in finish quality, corrosion performance and cost.
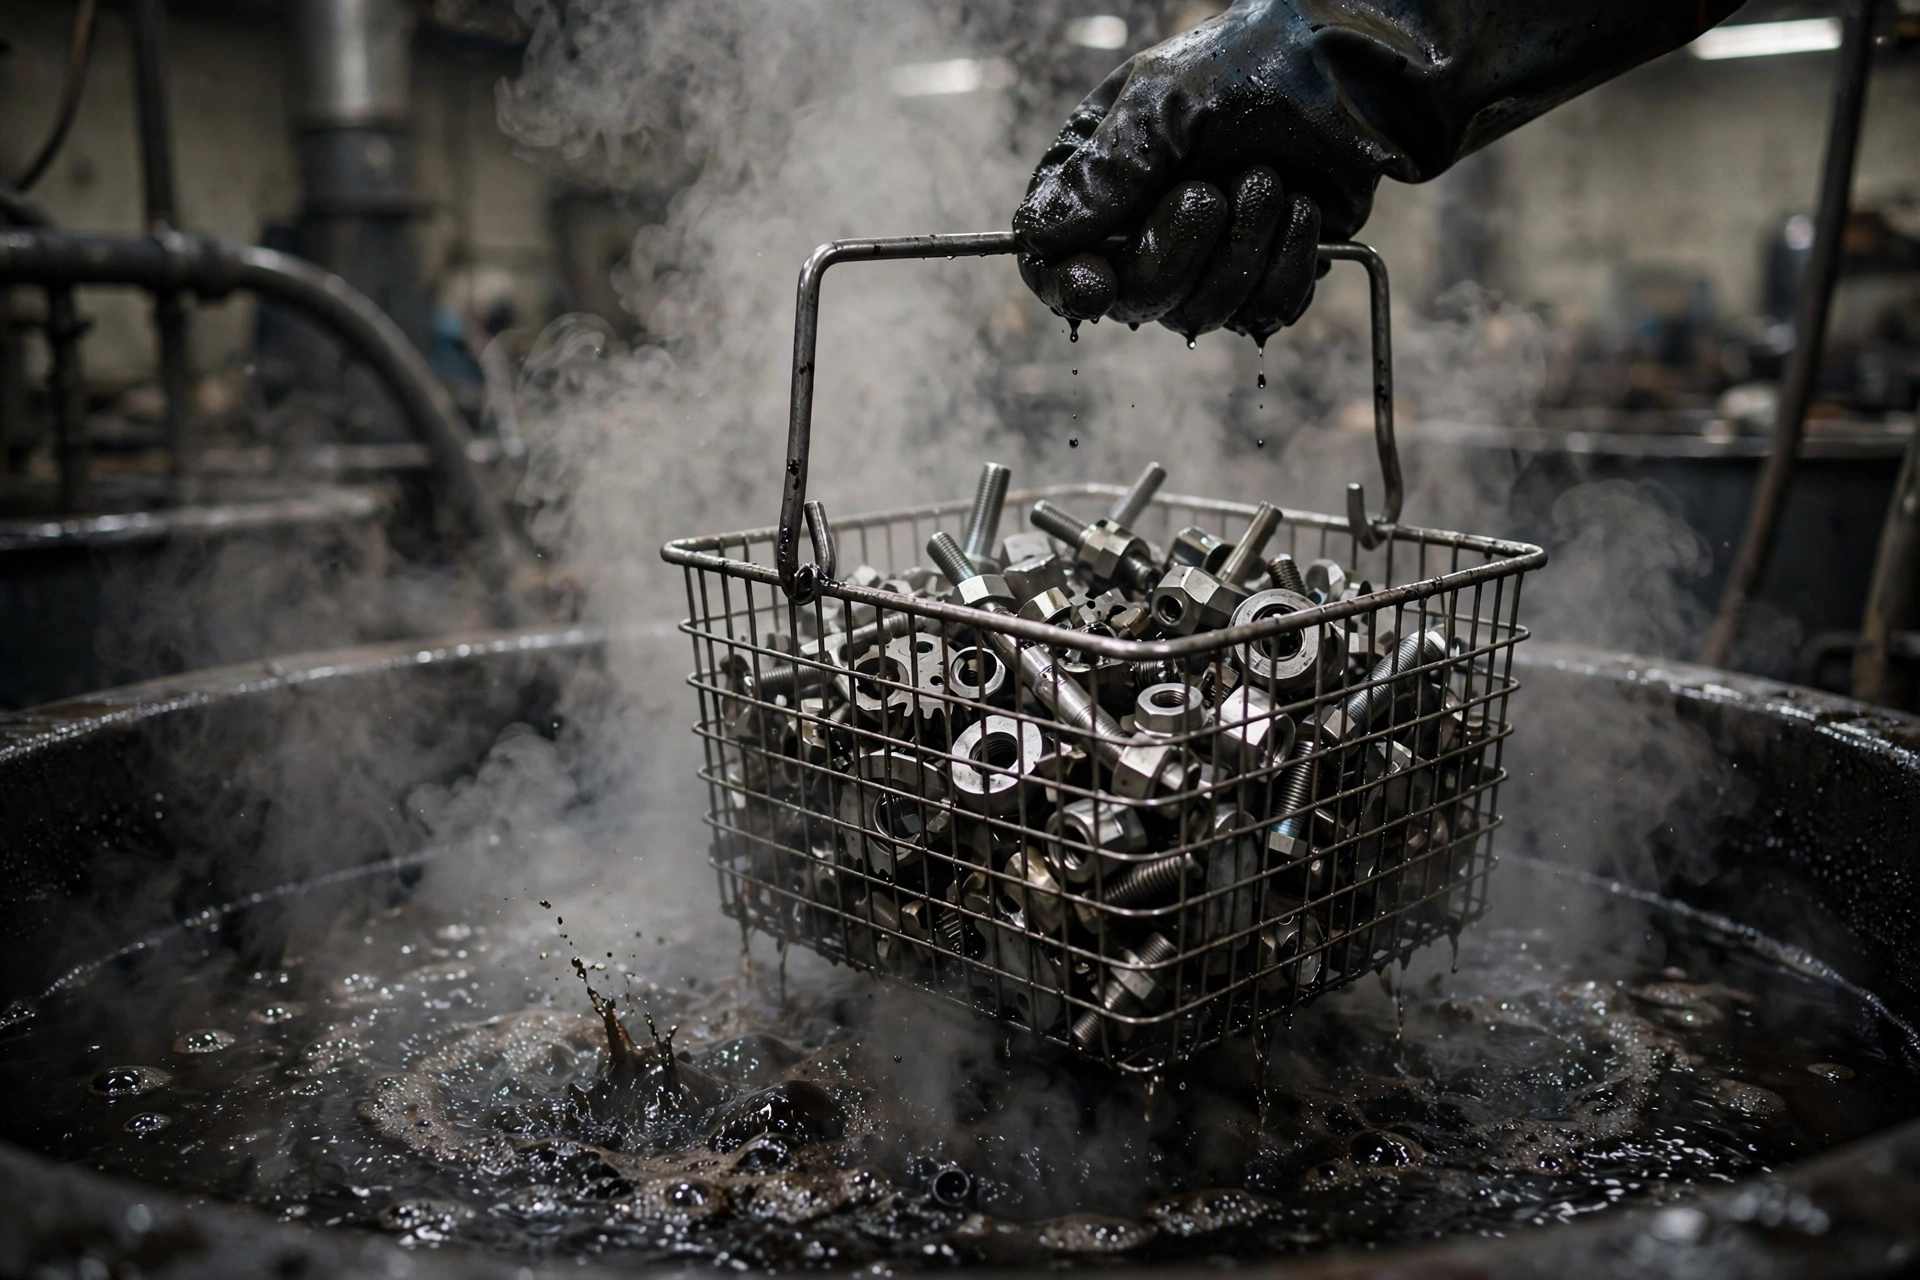
Hot black oxide is the traditional and most widely specified process. It operates at about 141 degrees Celsius (285 degrees Fahrenheit) in a bath of sodium hydroxide, nitrates and nitrites.
The high temperature drives a true chemical conversion. The resulting magnetite layer is dense, uniform and well bonded to the substrate.
Hot black oxide can be specified to applicable classes of MIL-DTL-13924, the US military specification for black oxide on ferrous metals. Compliance depends on the substrate, process controls, inspection and specific class stated on the drawing.
The downside is energy cost, handling of hot caustic solution and wastewater treatment. The bath chemicals are alkaline and require proper disposal.
Mid-temperature processes run at about 100 to 120 degrees Celsius (220 to 250 degrees Fahrenheit). They use proprietary chemical blends that produce a magnetite layer similar to the hot process but at a lower operating temperature.
Mid-temperature black oxide reduces energy use and is somewhat easier to handle in smaller shops. The finish can approach the quality of hot black oxide, although many specifications still call out the hot process explicitly.
Cold black oxide is a room-temperature process that deposits a copper selenium compound on the surface rather than converting the iron into magnetite. Strictly speaking, it is not a true oxide conversion coating.
Cold black oxide is inexpensive and easy to apply, which makes it popular for small batches and non-critical parts. However, it does not meet MIL-DTL-13924 and its adhesion and corrosion resistance are lower than the hot process. It can also rub off more easily under handling or contact.
| 特点 | Hot black oxide | Mid-temperature | Cold black oxide |
|---|---|---|---|
| Bath temperature | About 140–150°C (284–302°F) | About 100–120°C (212–248°F) | 室温 |
| Chemistry | Hot alkaline oxidizing salts | Lower-temperature proprietary salts | Typically copper–selenium compounds |
| True conversion coating | Yes; magnetite on ferrous metals | Yes; magnetite on ferrous metals | Usually no; deposited blackening layer |
| MIL-DTL-13924 | Possible if specified process and tests comply | Verify process eligibility and supplier certification | Generally not compliant |
| Adhesion | Typically strong when correctly processed | Typically strong when correctly processed | More variable; may rub off |
| 耐腐蚀性 | Limited without oil or sealant | Limited without oil or sealant | Often lower; sealant dependent |
| Dimensional impact | Very small; verify tolerances | Very small; verify tolerances | Very small; verify tolerances |
| 相对成本 | 中度 | 中度 | Often lower |
For CNC machined parts that need to meet a drawing callout or a military specification, hot black oxide is the standard choice. Cold black oxide is acceptable for prototypes, internal tooling or parts where appearance matters more than performance.
The hot black oxide process for steel follows a consistent sequence. Each step matters because contamination or improper rinsing causes blotchy finish, poor adhesion or early rust.
Tuowei’s black oxide finishing service follows this sequence with in-process quality checks at each step.
Yes, black oxide can rust if the sealant is missing, worn away or improperly applied. This is the most common misunderstanding about the finish.
The magnetite layer itself is stable and will not flake or peel, but it is porous. Without a sealant, moisture reaches the base steel through the pores and corrosion starts underneath. Black oxide generally offers limited salt-spray resistance compared with heavy-duty protective coatings. Report ASTM B117 results only for the tested substrate, pretreatment, sealant, coating specification and failure criterion; the standard defines a test method, not a guaranteed number of protective hours.
Zinc plating and properly specified powder-coating systems can deliver substantially greater corrosion protection, but exact salt-spray hours depend on thickness, pretreatment, topcoat or passivation, and the specified test endpoint. Black oxide is not a heavy corrosion barrier. It is a light protective and cosmetic finish best suited for parts that operate in controlled environments or receive regular oiling.
Parts that will be stored or shipped need a heavier rust-preventive oil or VCI (volatile corrosion inhibitor) packaging. Black oxide finishers typically offer both options.
Black oxide corrosion resistance is adequate when the part:
It is not adequate when the part is exposed to outdoor weather, salt spray, high humidity or corrosive chemicals over long periods.
The table below puts black oxide in context against other common finishes for CNC machined steel and aluminum parts.
| 完成 | Typical substrates | Corrosion performance | Dimensional impact | 相对成本 |
|---|---|---|---|---|
| Black oxide (oiled) | Applicable steels | Depends on sealant and test | Very small; verify tolerances | 低 |
| Phosphate coating (oiled) | 钢 | Depends on phosphate and oil | Varies by coating class | 低 |
| Zinc plating | 钢 | Depends on thickness and passivation | Specified deposit thickness | 中型 |
| Electroless nickel | Steel, aluminum, copper | Depends on deposit and test | Specified deposit thickness | 更高 |
| 粉末涂装 | Steel, aluminum | Depends on pretreatment and system | Specified dry-film thickness | 中型 |
| II型阳极氧化 | 铝质 | Depends on alloy and sealing | Specified oxide thickness | 中型 |
| 铬酸盐转化 | 铝质 | Depends on process and class | Thin conversion layer | 低 |
Black oxide is often selected for minimal dimensional change and a uniform dark appearance, but its corrosion performance depends heavily on the supplementary treatment. Choose the finish against the drawing tolerances, environment and test requirements, rather than relying on a single generic ranking.
Yes, stainless steel can be black oxide treated, but it requires a different chemistry than carbon steel. The standard hot alkaline process for carbon steel does not work on stainless because the chromium oxide layer on stainless resists the reaction.
Stainless steel black oxide uses a proprietary acid-based process that creates a dark, uniform surface. It is less common than carbon steel black oxide and fewer finishers offer it, but it is a viable option when a black finish is needed on stainless parts without adding a deposited coating.
MIL-DTL-13924 specifies four black oxide process classes for applicable ferrous metals. The classes describe process chemistry and material applicability, not four separate families of steel, copper and zinc:
| 班级 | Base metal |
|---|---|
| Class 1 | Alkaline oxidizing process for wrought, cast and malleable iron and plain carbon or low-alloy steels |
| Class 2 | Alkaline oxidizing process for certain corrosion-resistant steels |
| Class 3 | Fused-salt oxidizing process for corrosion-resistant steels |
| Class 4 | Alkaline oxidizing process for corrosion-resistant steels, including specified 300-series grades |
For CNC machined stainless steel, select the MIL-DTL-13924 class based on the exact steel grade and approved process, and confirm the current specification and capabilities with the finisher before finalizing the drawing. Do not assume Class 2 covers every stainless alloy.
Copper and brass can receive specialized blackening treatments, but they are not MIL-DTL-13924 Class 3 ferrous-metal treatments. Conventional steel black oxide chemistry is not suitable for aluminum; black anodizing or black powder coating are common alternatives.
Black oxide is widely used across industries where a black finish, reduced reflection, mild corrosion protection or dimensional preservation is needed.
Most firearm components are hot black oxide treated to reduce glare and protect against light handling corrosion. The finish is specified per MIL-DTL-13924 Class 1 for carbon steel receivers, barrels and triggers.
Black oxide is used on fasteners, gears, shafts and internal engine components. It reduces galling between mating steel surfaces and provides a base for oil retention, which helps lubrication in moving assemblies.
For non-critical steel hardware and tooling, black oxide provides a low-cost finish that meets military specifications without adding measurable thickness. Tuowei machines 航空航天零部件 with tight tolerances where black oxide preserves the as-machined dimensions.
Drill bits, taps, wrenches, calipers and gauge blocks are commonly black oxide treated. The dark surface reduces glare and shows wear patterns, which helps operators spot tool wear early.
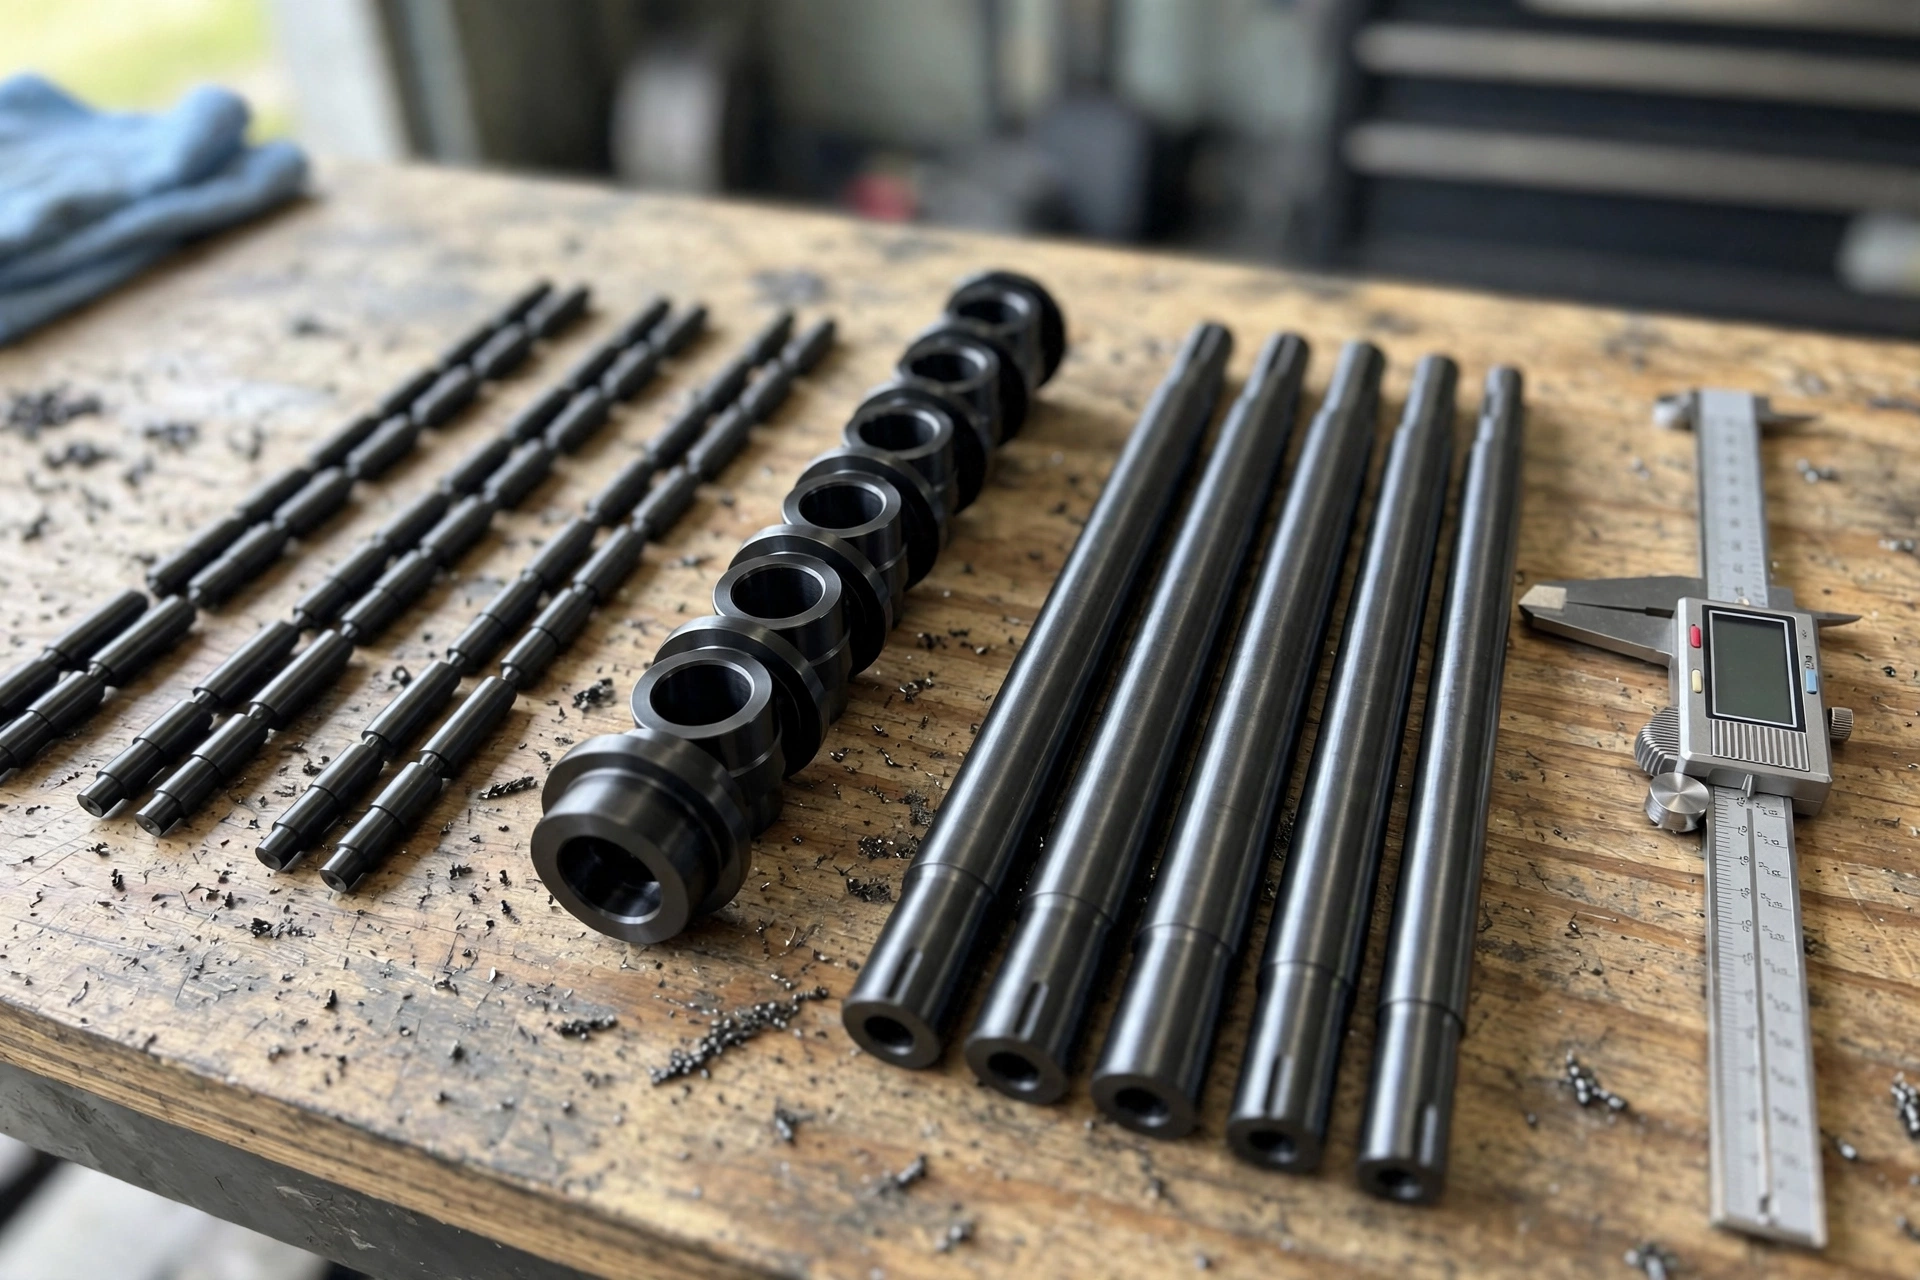
Any steel part that must hold a tolerance of plus or minus 0.001 inches or tighter benefits from a finish that adds virtually no material. Black oxide is the go-to finish for dowel pins, bushings, shafts, spacers and locating features on steel fixtures.
Black oxide makes sense when the application checks these boxes:
It does not make sense when the part faces outdoor exposure, aggressive chemicals, or when corrosion resistance measured in hundreds of salt spray hours is required. In those cases, zinc plating, 无电解镀镍, powder coating or a combination of finishes is a better choice.
For aluminum parts specifically, black oxide is not an option. Instead, look at black Type II anodizing or black powder coat, both of which Tuowei offers as standard finishes for CNC machined aluminum parts.
The main disadvantage is limited corrosion resistance, especially when the supplementary oil or wax protection is missing or wears away. Corrosion test results vary by substrate and sealant, so do not assume a universal salt-spray life. Black oxide also does not meaningfully increase base-metal hardness or abrasion resistance.
Hot black oxide is chemically bonded to the metal, so it will not chip, peel or flake under normal handling. It can wear through over time on contact surfaces, especially without lubrication. For parts that slide or rub against other surfaces, a harder finish like electroless nickel or hard chrome is more durable.
A properly applied hot black oxide finish does not rub off. Cold black oxide, on the other hand, can smear or transfer to a white cloth because it is a deposited compound rather than a true conversion coating. If rub-off is a concern, specify hot black oxide and confirm the process meets MIL-DTL-13924.
Standard black oxide with an oil sealant is not considered food safe because the oil itself is not food-grade. Some manufacturers offer food-grade sealants or dry wax finishes for black oxide parts used in food processing equipment. Confirm the sealant type with the finisher if the part will contact food.
Black oxide goes by several names depending on the industry and the base metal. Common alternatives include blackening, gun bluing, hot blackening, alkaline blackening and chemical blackening. On copper parts, it is sometimes called copper oxide or CuO coating. Technically, gun bluing uses a slightly different chemistry (selenium dioxide or ferric chloride) and produces a different oxide, but the terms overlap in common use.





