Powder coating protects pièces métalliques and gives them color at the same time. Instead of liquid paint, it uses a fine powder that is sprayed onto a part with an electric charge and then baked in an oven until it forms a hard, continuous coating. The result is a tough, high-quality finish that resists chipping, scratching, corrosion, and fading better than most liquid paints.
If you buy machined components, you have almost certainly handled powder coated products: appliance panels, fence sections, automotive wheels, equipment housings, and electrical enclosures. Powder coating is commonly used across all of them, and this guide explains what powder coating is, how the process works, how long it lasts, and when it is the right choice, including for services de revêtement en poudre on CNC machined parts.
The dry powder coating process is one in which the coating is applied as a powder to a substrate and then cured with heat to form a solid protective layer. The powder itself is made from polymer resins mixed with curatives, pigments, leveling agents, and flow modifiers. These ingredients are melt mixed, cooled, and ground into a uniform powder with a texture similar to baking flour.
The powder coating industry has used this process in North America since the 1960s, according to the Powder Coating Institute and it now holds more than 15% of the industrial finishing market. It is specified for both functional protection and decoration, unlike many older coating processes, and powder coatings are available in an almost limitless range of colors and textures. That combination is why it shows up on everything from heavy machinery to household goods.
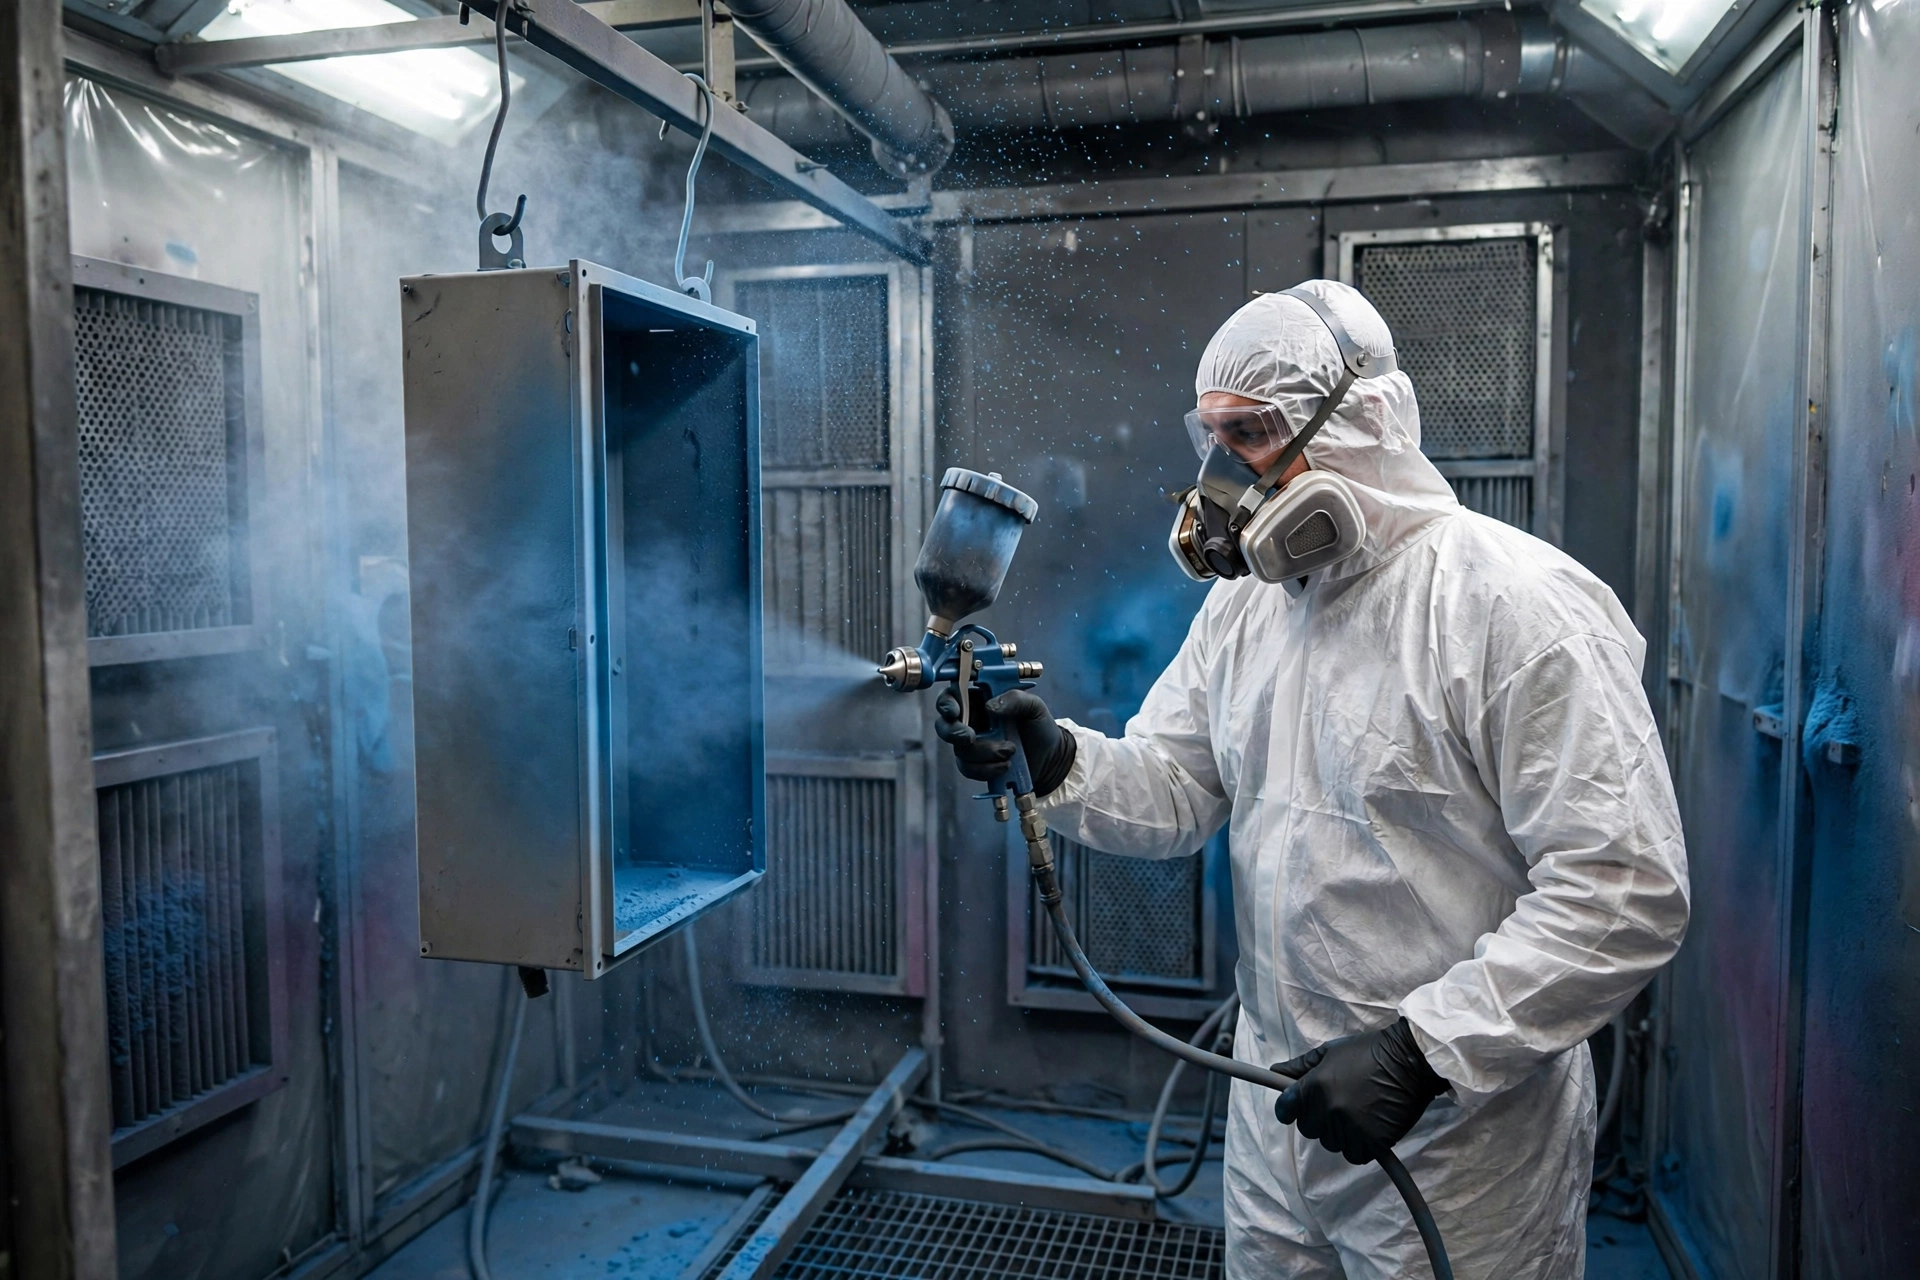
The standard process called electrostatic spray deposition starts with a powder coat gun. The gun applies an electrostatic charge to the powder particles, and the grounded metal part attracts them, so the powder sticks evenly across the surface. The coated part then goes into the oven, where heat melts the powder into a continuous film and triggers the chemical reaction that hardens it.
The powder coating process involves cleaning and pretreatment, electrostatic powder coating application, and oven curing. Modern powder coating technology has refined each stage, from pretreatment chemistry to oven controls.
Good powder adhesion starts before any powder is sprayed. The cleaners used to clean parts are alkaline, acidic, or neutral, and most parts receive a chemical pretreatment matched to the metal: iron phosphate for steel, zinc phosphate for galvanized or steel substrates, and chromium phosphate or non-chrome treatments for aluminum substrates, which improve adhesion of the powder to the metal.
Some parts are also blasted with sand or shot to create a fine anchor pattern that helps the powder to stick to the surface. Blasting is especially useful for removing rust, mill scale, and laser oxide. After cleaning and treatment, parts are rinsed and dried in a low temperature dry off oven so they are fully dry before coating.
The application process starts in a powder coating booth, where compressed air carries the powder through an electrostatic gun that charges each particle. Because the part is grounded, the charged powder is drawn to it and wraps around edges and curves, building an even layer of uniform powder application. The operator keeps spraying until the part is fully covered, and any overspray can often be collected and reused.
An alternative method is fluidized bed application, which coats parts without using a spray gun. Parts are preheated and then dipped into a tank of fluidizing powder, which melts directly onto the hot surface. This method suits a thicker coating on simpler shapes, while electrostatic spraying suits most machined parts with varied geometry. Production guides such as Nordson’s complete guide to powder coating describe both spray and fluidized bed setups for industrial use.
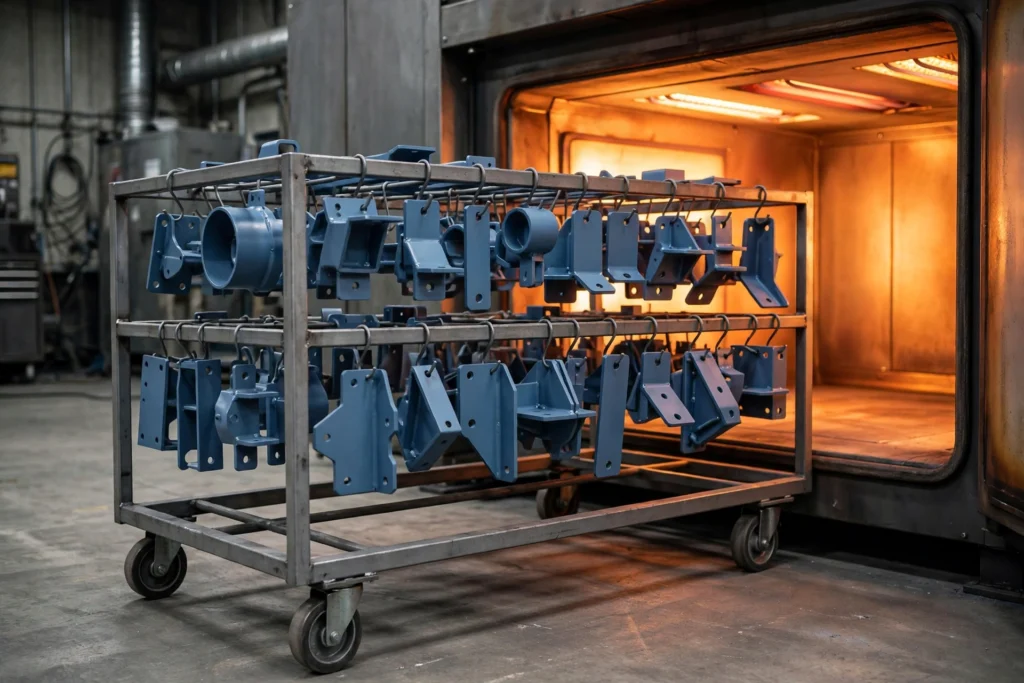
Curing is where the powder becomes a real coating, and the curing process decides the final quality. For thermoset powders, ovens typically run at 150 to 200 degrees Celsius for 10 to 20 minutes, although the exact schedule depends on the powder, the part material, and its thickness and shape. In that heat, the powder melts, flows out, and crosslinks into long, tightly bonded molecular chains, improving the bonding of the powder to the metal.
Once curing is complete and the part has cooled, the cured powder forms a single continuous film rather than a layer of separate particles. That crosslinked structure is the reason powder coatings resist impact, moisture, chemicals, and ultraviolet light far better than a dried layer of conventional paint.
| Process step | What happens |
| 1. Pretreatment | Cleaning, chemical treatment matched to the metal, optional blasting, rinsing, and drying |
| 2. Application | Electrostatic spray coats the grounded part, or preheated parts are dipped in a fluidized bed |
| 3. Curing | Oven heat melts the powder into a continuous film and crosslinks it into a hard coating |
| 4. Cooling and inspection | Parts cool, the film sets, and the finish is checked before assembly or packing |
Both powder coating and liquid paint protect and color a part, but they get there differently. Paint arrives as a liquid full of solvents that must evaporate as it dries, which can cause drips, sagging, and runs. A powder coat has no wet stage at all, so those defects simply do not occur, and there is no flash off drying time to manage.
Powder coatings contain no solvents, so they release little to no volatile organic compounds during application. Applying powder coatings this way lets shops apply powder coatings with less waste, since overspray can be recovered and recirculated, which cuts waste and often makes the process more efficient than painting over a production run, even when the equipment costs more up front.
| Aspect | Powder coating | Liquid paint |
| Form applied | Dry powder, electrostatically charged | Liquid droplets, usually solvent based |
| Solvents and VOCs | None, so little to no VOC emissions | Solvents evaporate as paint dries, releasing VOCs |
| Typical finish defects | Very few, with no drips or sagging | Drips, runs, and sagging are common risks |
| Durabilité | Harder, more resistant to chipping and chemicals | Softer film, more prone to scratching and peeling |
| Overspray | Can be collected and reused | Generally wasted once sprayed |
Different powder coating types fall into two main families, thermoset and thermoplastic, plus a smaller category of UV curable powder coatings for heat sensitive substrates. The difference comes down to what happens when the cured coating is heated again, and that difference decides where each type should be used.
The type of powder used most often is thermoset. During curing, their resins crosslink into new, thermally stable compounds, which means the finished coating cannot be melted and reshaped by heating it again. Common thermoset materials include epoxy, polyester, acrylic, and epoxy polyester blends.
That stability makes thermosets a strong choice for parts that see heat in service, such as automotive housings and covers, appliance panels, and equipment parts. A powder coat made this way is cost effective, hard, and chemically resistant, which is why thermosets dominate general industrial powder coating work.
Thermoplastic powders melt when heated and solidify when cooled, without any permanent chemical change. That means a thermoplastic coating can be remelted and reshaped, and the materials are often recyclable. Common examples include nylon, polyvinyl chloride, and polyester based powders.
Thermoplastics offer superb corrosion resistance, but they soften again if they are reheated toward their melting range, typically around 100 to 150 degrees Celsius. They are therefore a poor choice for parts that will run hot, and a good choice for parts that need chemical resistance without high temperature exposure.
| Propriété | Thermoset | Thermoplastique |
| After curing | Crosslinked, cannot be remelted | Can be remelted and reshaped |
| Common materials | Epoxy, polyester, acrylic, epoxy polyester | Nylon, PVC, polyester |
| Heat behavior | Stays stable when reheated | Softens again near 100 to 150 degrees Celsius |
| Idéal pour | General industrial parts, vehicles, appliances | Chemical resistance where heat is not an issue |
One reason designers like powder coating is the range of looks it can produce from a single process, including a wide range of colors. Colors are built from pigment combinations in the base powder, and color matching is commonly done against standard color codes. Gloss and texture then change how that color reads on the finished part. Powder coatings offer all of this from one powder coat finish.
Gloss is measured in gloss units, and the usual bands are matte below 30, standard gloss around 70, and high gloss above 80. Matte finishes diffuse light and help hide surface imperfections, while high gloss finishes are shinier, smoother, and easier to clean but tend to show every flaw underneath.
Gloss also tracks with the recipe: as the share of pigment in the powder rises, gloss falls, and coatings with more resin and less pigment are used to achieve higher gloss. Semi gloss finishes sit between the two, with better stain and abrasion resistance than a flat finish.
Beyond smooth finishes, powder coating offers textures such as wrinkle, sand, and hammer finishes. Wrinkle textures, usually based on polyester or urethane chemistry, are good at covering surface imperfections and give decent weathering, hardness, and chemical resistance. Hammer textures look like an orange rind and resist abrasion and chipping well.
Texture is a practical choice, not just a cosmetic one. A textured surface can hide minor marks, add grip, and stand up to handling better than a smooth high gloss coat, but it can also be harder to clean. The right texture depends on how the part will be handled and where it will live.
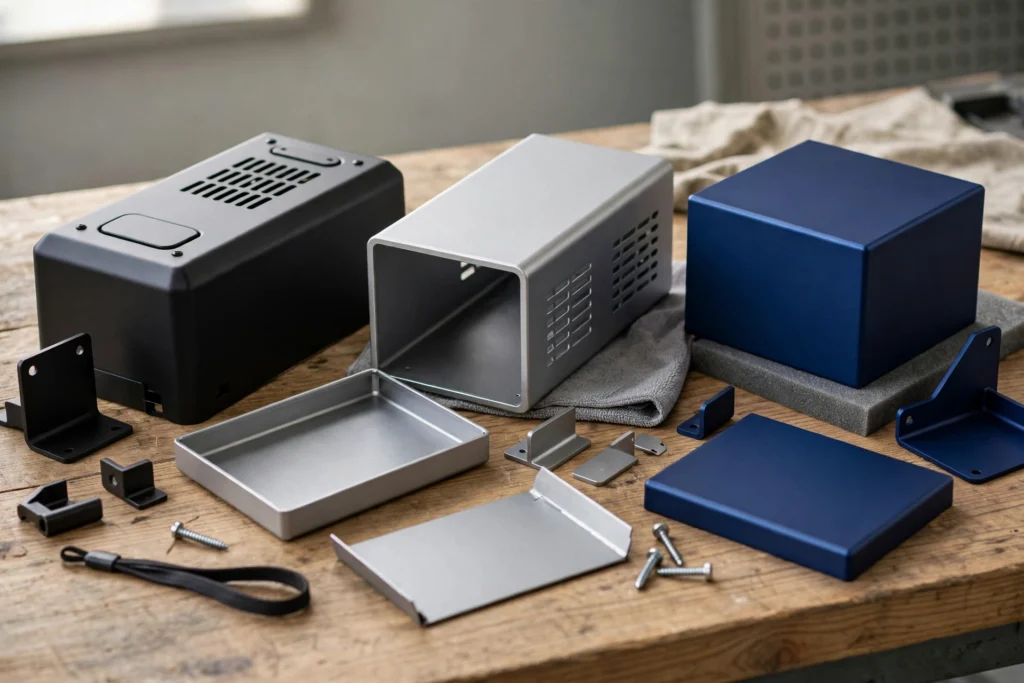
Powder coatings typically last 15 to 20 years or more, depending on the powder composition and the type of coating. That lifespan is one of the main reasons buyers choose powder over paint: the crosslinked film resists impact, moisture, chemicals, ultraviolet light, and extreme weather, which reduces scratching, chipping, corrosion, and fading over the life of the product.
Those years are typical ranges, not guarantees, and indoor parts usually outlast outdoor ones. A coated bracket inside an enclosure lives an easier life than a fence panel facing sun, rain, and road salt every day. The gap between a coating that lasts five years and one that lasts twenty usually comes down to the factors in the table below.
| Facteur | How it affects lifespan |
| Pretreatment quality | Thorough cleaning and the right phosphate treatment give the coating something to grip, poor preparation leads to early peeling |
| Film thickness | Even, full coverage protects the metal, while thin or patchy areas expose it to corrosion and abrasion |
| Powder chemistry | The right resin for the environment matters, outdoor parts need powders rated for weather and UV exposure |
| UV exposure | Constant sunlight breaks down weaker coatings, causing chalking and fading over time |
| Environment | Coastal salt, harsh chemicals, and heavy abrasion all wear a coating faster than a mild indoor setting |
| Care and repair | Regular cleaning and prompt attention to chips and scratches keep small damage from spreading |
The most common early failures trace back to preparation and specification, not to the powder itself. A part that was not properly cleaned, a film applied too thin or unevenly, or a powder chosen for indoor use and then installed outdoors will all fail sooner than expected. These are avoidable problems when the finisher controls each step.
Service conditions do the rest. Salt air near the coast, aggressive cleaning chemicals, constant abrasion, and physical damage all shorten coating life, especially when chips are left unrepaired and moisture reaches the bare metal underneath. A durable finish still needs sensible handling to reach its full lifespan.
Powder coatings are used most often on steel, aluminum, and galvanized substrates, and the pretreatment is chosen to match each metal. The powder coating used most often for outdoor parts is polyester, valued for weather resistance. With the right process, it can also be applied to non metallic substrates such as plastics and medium density fiberboard, although metal remains the standard case.
The main constraint is heat. Standard curing happens in an oven, so the part must survive the cure temperature without warping or degrading. Heat sensitive substrates can sometimes use UV curable powders instead, where a melt stage is followed by a UV cure that takes seconds rather than a long oven cycle. Common applications of powder coating cover appliances, vehicles, furniture, and enclosures.
Powder coating is not the right finish for every part. Because application relies on a spray pattern, surfaces must have a line of sight to the gun: the inside of tubing, deep recesses, and blind holes can be difficult or impossible to coat evenly by spraying, and a dipping process may suit those shapes better.
Geometry and tolerances need attention too. Sharp edges should be broken with a radius or chamfer, because charged particles do not adhere well to sharp corners. Coating thickness must also be allowed for in the design, especially on moving parts and assemblies with precise fits, since the added film changes dimensions.
For machined parts, powder coating is commonly used as the final step after machining: the part is made, cleaned, pretreated, coated, and cured. As a surface finish, it suits enclosures, brackets, panels, housings, and frames in aluminum and steel, where a powder coat adds corrosion protection and a consistent cosmetic finish to a part that already holds precise machined features. It pairs naturally with Services d'usinage CNC that produce those parts.
Aluminum is a particularly common pairing, since it machines cleanly and takes pretreatment well; our guide to machining 6061 aluminum covers the alloy most often used for such parts. Areas that must stay bare, such as threads or mating faces, are masked before coating so the finish never interferes with assembly. The Précision Tuowei team can advise on finish selection alongside machining.
Start from the environment the part will live in. Indoor parts can use a wide range of powders, while outdoor parts need weather resistant chemistry and careful pretreatment to reach the long lifespans quoted above. Color and texture then follow from appearance needs and how much handling the part will see.
Ask your finisher about two numbers before committing: the pretreatment they will use for your metal, and the thickness of the powder coating they target. Most standard powder coated finishes measure around 60 to 80 micrometers thick after curing, and that figure should be agreed in advance for any part with tight fits. For a dedicated finishing route, see our services de revêtement en poudre page.
Powder coating is a dry finishing process in which the coating is applied as a powder made from polymer resins, curatives, pigments, and leveling agents to a metal part. The powder is charged electrostatically so it sticks to the grounded part, then cured in a curing oven into a hard, durable, decorative, or protective coating. The uses of powder coating range from appliances and vehicles to enclosures and furniture.
The part is cleaned and pretreated, sprayed with electrostatically charged powder, and baked in a powder coating oven. Heat melts the powder into a continuous film and crosslinks it into a tough coating. Thermoset powders typically cure at 150 to 200 degrees Celsius for 10 to 20 minutes, depending on the powder and the part.
A powder coat typically lasts 15 to 20 years or more, depending on the powder composition and coating type. Indoor parts generally last longest, while outdoor parts depend on UV exposure, pretreatment quality, film thickness, and the environment. These are typical ranges, not guarantees for any specific part.
For most metal parts, yes. Powder coating provides a harder, more durable finish than wet paint, with better resistance to chipping, scratching, chemicals, and weather. It also avoids drips and sagging, releases little to no volatile organic compounds, and lets overspray be recovered and reused. The main advantages of powder coating over paint are durability, consistency, and lower waste.
Powder coating needs oven curing, so parts must survive the heat, and spray application needs a line of sight to the surface, which makes deep recesses and blind holes hard to coat. Coating thickness affects tolerances on precise fits, sharp edges must be broken first, and touching up damage is harder than with wet paint.
Cost depends on part size and quantity, the color and texture chosen, the pretreatment required, and whether masking or special handling is needed. Because of those variables, no single price applies to every job, and the reliable way to budget is to request a quote for your specific parts and volumes.
The process of powder coating turns a fine polymer powder into a hard, attractive, long lasting coating on metal. It beats wet paint on durability, appearance consistency, and environmental impact for most applications, as long as the part can take oven curing.
Design matters too: line of sight for spraying and allowance for coating thickness decide whether the finish performs as promised. For machined parts that need both protection and a clean finished look, a powder coat is one of the most dependable finishes available, and our services de revêtement en poudre page is the place to start.