

By Owen Lin, Engineer, Tuowei Precision · November 2026
Die casting is a metal casting process that forces molten metal into a hardened steel mold, called a die, under high pressure. The metal fills the cavity in a fraction of a second, freezes against the cooled die walls and comes out as a near-finished part.
Most die cast parts are made from aluminum, zinc or magnesium alloys. So what is die casting best suited to? Volume. Once the tool exists, a machine can repeat the same complex shape thousands of times with very little variation.
الإجابة المختصرة: Die casting injects molten non-ferrous metal into a reusable steel die at high pressure, holds it while it solidifies, then ejects a near-net-shape part. It suits complex, thin-walled aluminum, zinc and magnesium parts in medium to high volumes, where the cost of the tool can be spread across thousands of pieces.
This guide covers how the process works step by step, the main machine types, which alloys you can cast, what tolerances to expect, and the design and buying mistakes behind most problems with cast parts.
Every casting method does the same basic thing: liquid metal goes into a shaped cavity and is left to freeze. The differences come from the mold and from how the metal gets in.
That pressure is the whole point. It drives metal into thin walls and fine details before it can freeze, and it presses the metal against polished steel, which is why the as-cast surface is smooth.
A die has two halves. The cover die is fixed to the injection side of the machine, and the ejector die moves to open the tool and push the part out. Engineers call the result a near-net-shape part, meaning it needs little or no machining to reach its final form.
If you know القولبة بالحقن, the logic will feel familiar: a two-half steel tool, a fast injection, a cooling period and ejection. The difference is temperature. Molten aluminum is far hotter than molten plastic, so the steel takes much more punishment and the die wears out sooner.
Every shot follows the same cycle. On a cold-chamber aluminum machine it typically runs like this:
Cycle time depends mostly on wall thickness and alloy. Thin zinc parts cycle very quickly. A heavy aluminum housing has to sit in the die longer while its thick sections solidify.
Temperature balance matters as much as injection speed. A die that runs too cold gives cold shuts and flow lines on the surface. One that runs too hot causes soldering, where aluminum welds itself to the steel and tears the part on ejection. Most early-production defects trace back to one of these two conditions, not to the alloy.
The tool itself takes time. A new die goes through design and flow simulation, CNC machining and EDM of hardened tool steel, heat treatment, and then trial shots. First samples almost always need small adjustments to gates, vents or ejection, so build that loop into your schedule.
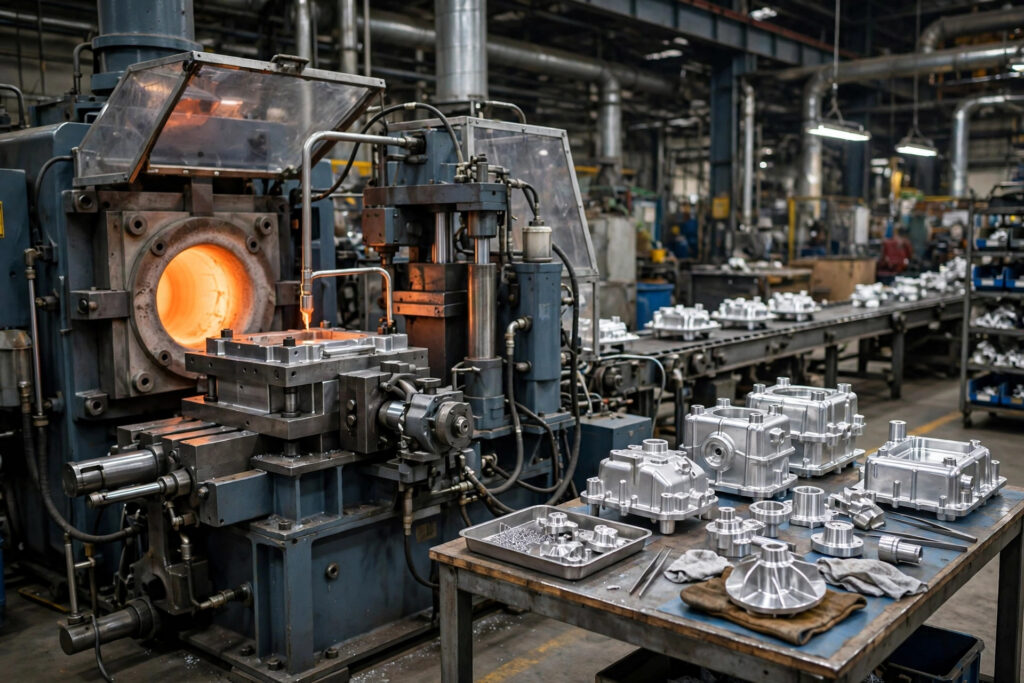
In a hot-chamber machine, the injection mechanism, called a gooseneck, sits inside a pot of molten metal that is part of the machine. Each stroke of the plunger pushes metal straight from the pot into the die. There is no ladling step, so cycles are fast.
The catch is that the injection parts sit in molten metal all day. That only works for alloys with low melting points that do not attack iron. Zinc, which melts at about 419 °C (786 °F), is the classic hot-chamber metal, along with some magnesium, lead and tin alloys. Aluminum is ruled out because molten aluminum dissolves the iron components.
A cold-chamber machine keeps the furnace separate. For every shot, a measured amount of molten metal is ladled into a shot sleeve, and a hydraulic plunger drives it into the die. The extra step slows the cycle, but the injection parts only touch hot metal briefly.
This is the route for aluminum, which melts at about 660 °C (1,220 °F), and for magnesium and copper alloys. ASTM B85, the US specification for aluminum-alloy die castings, notes that alloys such as A360, A380, 383, 384 and A413 can be produced only on cold-chamber machines.
| الميزة | Hot-chamber | Cold-chamber |
|---|---|---|
| Where the metal is melted | In a pot inside the machine | In a separate furnace |
| Typical alloys | Zinc, some magnesium, lead, tin | Aluminum, magnesium, copper alloys |
| Cycle speed | أسرع | Slower (ladling each shot) |
| Typical part size | Small to medium | Small to large |
| Wear on injection parts | Constant contact with melt | Brief contact per shot |
High pressure die casting (HPDC) is the umbrella term for both machine types above. When engineers say “die casting” without a qualifier, they almost always mean HPDC. Its strengths are speed, thin walls and fine detail. Its weakness comes from the same fast, turbulent fill: air and gas get trapped, and that porosity limits heat treatment, welding and pressure tightness.
Gravity die casting, also called permanent mold casting, pours metal into a reusable steel or iron mold and lets gravity fill it. There is no injection pressure. Cycles are slower and walls must be thicker, but the calmer fill traps less gas, so parts can often be heat treated for higher strength.
Our view: for most custom parts under a few kilograms, conventional cold-chamber HPDC in aluminum or hot-chamber zinc is the right starting point. Move to vacuum, squeeze or gravity casting only when the part must be heat treated, welded or held to a strict leak test.
The process is built around non-ferrous alloys. Steel melts above 1,400 °C, and at that temperature the steel die itself would erode within a short run, so ferrous parts are cast in sand or investment molds instead.
| Alloy family | الدرجات الشائعة | نقاط القوة | Watch-outs |
|---|---|---|---|
| ألومنيوم | A380, ADC12, A360, A413 | Light, strong, good thermal conductivity, most widely used | Porosity; high-silicon grades anodize gray and patchy |
| الزنك | Zamak 3, Zamak 5, ZA-8 | Best fluidity, very thin walls, long die life, excellent for plating | About 2.6 times heavier than aluminum; creeps under sustained load and heat |
| المغنيسيوم | AZ91D, AM60B | Lightest structural metal, good EMI shielding | Needs corrosion protection and careful melt handling |
Aluminum die casting is the cold-chamber process applied to aluminum alloys, and it accounts for most die cast parts by volume. A380 is the general-purpose workhorse, with a balance of strength, castability and cost. ADC12 is its close Japanese and Chinese equivalent. A360 gives better corrosion resistance and pressure tightness but is harder to cast, and A413 is chosen for thin, pressure-tight parts.
One limit is worth knowing early. ASTM B85 covers general-purpose castings and states that it may not address the properties and testing needed for highly loaded or safety-critical parts. If your part falls in that category, agree the test plan with the caster before tooling starts.
Zinc alloys run on hot-chamber machines, fill the thinnest walls and give the best surface for plating, so they suit small hardware, connectors and decorative parts. Magnesium is the choice when weight is the priority, such as laptop and camera frames or automotive brackets.
في دقة تووي we cast aluminum, zinc and magnesium alloys, and the alloy decision usually comes down to weight, wall thickness and the finish the part needs.
As-cast tolerance depends on part size, alloy and whether a dimension crosses the parting line or a moving slide. Dimensions held within one die half are the most stable. The North American Die Casting Association publishes standard and precision tolerance tables in its product specification standards, and most casters work from them.
Typical as-cast tolerances on our خدمات صب القوالب:
| Die casting type | التفاوت المعتاد |
|---|---|
| Standard die casting | ±0.010 بوصة (±0.254 ملم) |
| High-precision die casting | ±0.005 بوصة (±0.127 ملم) |
| الأجزاء المعقدة | ±0.008 in (±0.203 mm) |
| Large parts | ±0.020 in (±0.508 mm) |
Features tighter than this, such as bearing bores, sealing faces and threads, are machined after casting. Small round holes under 3 mm in diameter are also drilled afterwards, because thin cores do not survive the heat of aluminum casting well.
Our advice: accept as-cast tolerances everywhere you can, and call out machined features only where the function needs them. Every precision call-out either costs extra tool steel work or a machining operation. Our خدمات التصنيع الآلي باستخدام الحاسب الآلي الرقمي handle that secondary work on cast parts in the same order.
| المزايا | العيوب |
|---|---|
| Very fast cycles and low cost per part at volume | High upfront tooling cost and long tool lead time |
| Complex shapes, thin walls and cast-in features | Porosity limits heat treatment, welding and some finishes |
| Good repeatability from part to part | Design changes after tooling are slow and expensive |
| Smooth as-cast surface | Mostly limited to non-ferrous alloys |
| Several parts can be combined into one casting | Part size limited by machine clamping force |
| Runners and scrap are remelted | Rarely economical for prototypes or small batches |
The pattern is simple. Almost every advantage comes from the steel die, and almost every disadvantage does too.
The decision comes down to two questions: how many parts you need, and how settled the design is. The die is a large upfront cost, while the cost per part afterwards is low. There is no universal break-even quantity, because it depends on part size, complexity, alloy and the alternative you are comparing against.
A common and sensible path is to machine the first prototypes from billet, then move to die casting once testing is done. Keep one trade-off in mind: a machined 6061 prototype will not show porosity or casting distortion, and its properties differ from cast A380. Plan to validate the first die cast samples properly rather than assuming they will behave like the prototype.
Good die cast design is mostly about helping metal flow in and helping the part come out.
Most problems with die cast parts start before the die is cut. These are the ones we see most often:
Die cast parts show up wherever a metal part needs complex geometry in volume:
Casting is the general term for pouring or forcing molten metal into a mold. Die casting is one type that uses a reusable hardened steel die and high injection pressure. Sand and investment casting destroy their molds each time, run slower and suit larger or ferrous parts.
The main downsides are high tooling cost, long tool lead times and porosity from air trapped during fast injection. Porosity can limit heat treatment, welding and pressure tightness. The process also mostly works with aluminum, zinc and magnesium, and rarely pays off for small batches.
Yes. High pressure die casting holds tighter tolerances and smoother surfaces than sand or gravity casting, and it repeats them shot after shot. Typical as-cast tolerances run from about ±0.005 in to ±0.020 in depending on size, while critical bores and threads are machined afterwards.
It can, but the result is rarely cosmetic. Common casting alloys such as A380 contain a lot of silicon, which leaves a gray, uneven anodic film. If appearance matters, powder coating, painting or plating is usually the better finish for die cast aluminum parts.
The name comes from the die, the hardened steel tool that forms the part. A die has two halves: a fixed cover half on the injection side and a moving ejector half. The same die is reused for every shot, which is what separates it from sand casting.
At Tuowei Precision we run more than 60 die casting machines and keep tooling, casting, CNC machining, surface finishing and inspection under one roof in Shenzhen, so one team owns the part from die design to finished batch. Our quality system is certified to ISO 9001:2015.
To get a useful quote, send a STEP file and drawing with the alloy, expected annual volume, cosmetic surfaces and the dimensions that are truly critical. Our engineers review every design for castability before tooling and flag draft, wall and porosity risks early. You can start with our die casting services page.
About the author: Owen Lin is an engineer at Tuowei Precision. He plans tooling and production processes and works with the quality team to keep every batch consistent.





